 日本語



Introduction: Understanding Polycarbonate (PC)
ポリカーボネート(PC)[^1] is renowned for its exceptional performance, offering high transparency, excellent impact toughness, creep resistance, and a wide operating temperature range. However, processing this engineering plastic requires precision.
Key Material Characteristics:
- Viscosity Sensitivity: PC melt viscosity is highly sensitive to temperature but less sensitive to shear rate.
- No Clear Melting Point: It softens over a range.
- High Melt Viscosity: Requires higher processing temperatures.
- Hydrolysis Risk: The resin is prone to hydrolysis at high temperatures if moisture is present, leading to part degradation.
> プロのアドバイス To improve melt flow, do not rely solely on increasing injection pressure. Instead, raise the injection temperature. However, strict moisture control is non-negotiable.
?️ Critical Pre-Processing: Drying & Mold Design
Before the injection process begins, specific steps must be taken to ensure quality.
- Drying is Mandatory[^2]: PC must be dried thoroughly to reduce moisture content to below 0.02%.
- Moisture Protection: Keep the resin insulated during processing to prevent re-absorption of moisture from the air.
- Mold Design: Runners and gates should be short and thick to minimize pressure loss.
- Stress Reduction: High mold temperatures and post-processing annealing are recommended to eliminate internal stress and prevent cracking.
⚙️ The 7 Key Parameters of PC Injection Molding
Here is a detailed breakdown of the processing window for PC.
1. Injection Temperature[^3] Temperature selection depends on part geometry, mold structure, and requirements.
- Standard Range: 270°C – 320°C.
- 警告だ: Exceeding 340°C can cause decomposition. Signs include darkened color, silver streaks, dark spots, and bubbles. Mechanical properties will significantly degrade.
2. 射出圧力[^4] Pressure affects physical properties, internal stress, and shrinkage.
- Standard Range: 80 – 120 MPa.
- High Pressure (120 – 145 MPa): Required for thin-walled, long-flow, or complex parts with small gates to overcome flow resistance.
3. Holding Pressure & Time Crucial for preventing vacuum voids and sink marks.
- 戦略: Low holding pressure with high melt temperature is often the best approach to reduce internal stress.
- Timing: Thin parts need short holding times; thick parts require longer times. This is often determined by the gate freeze-off time.
4. Injection Speed While speed has less impact on PC properties, flow control is key.
- 推奨事項: Use medium to slow speeds.
- Technique: Multi-stage injection (Slow-Fast-Slow) is preferred to ensure smooth filling without trapping air.
5. 金型温度[^5]
- Standard: 80°C – 100°C.
- Complex/Thin Parts: Can be increased to 100°C – 120°C (ensure this is below the mold steel's tempering temperature).
6. Screw Speed & Back Pressure[^6] Due to high viscosity, excessive speed can damage the machine or the material.
- Screw Speed: 30 – 60 r/min.
- Back Pressure: 10% – 15% of injection pressure.
7. Material Usage
- Release Agents: Use strictly controlled amounts.
- Recycled Material: Limit re-grind usage to max 20% and no more than 3 cycles.
Quick Reference: PC Processing Parameters
For easy reference, here is a summary of the optimal settings.
| パラメータ | Recommended Setting | Notes |
|---|---|---|
| Drying Temp/Time | 120°C / 4+ Hours | Moisture < 0.02% |
| 溶融温度 | 270°C - 320°C | Do not exceed 340°C |
| 射出圧力 | 80 - 145 MPa | Higher for thin walls |
| 金型温度 | 80°C - 120°C | Higher temp reduces stress |
| Screw Speed | 30 - 60 r/min | Prevents shear heating |
| 背圧 | 10% - 15% | Ensures melt density |
Screw Selection & Machine Requirements
Choosing the right hardware is as important as setting the parameters.
Machine Requirements:
- Shot Size: The maximum part weight (including runners) should not exceed 70-80% of the machine's nominal injection capacity.
Screw Specifications:
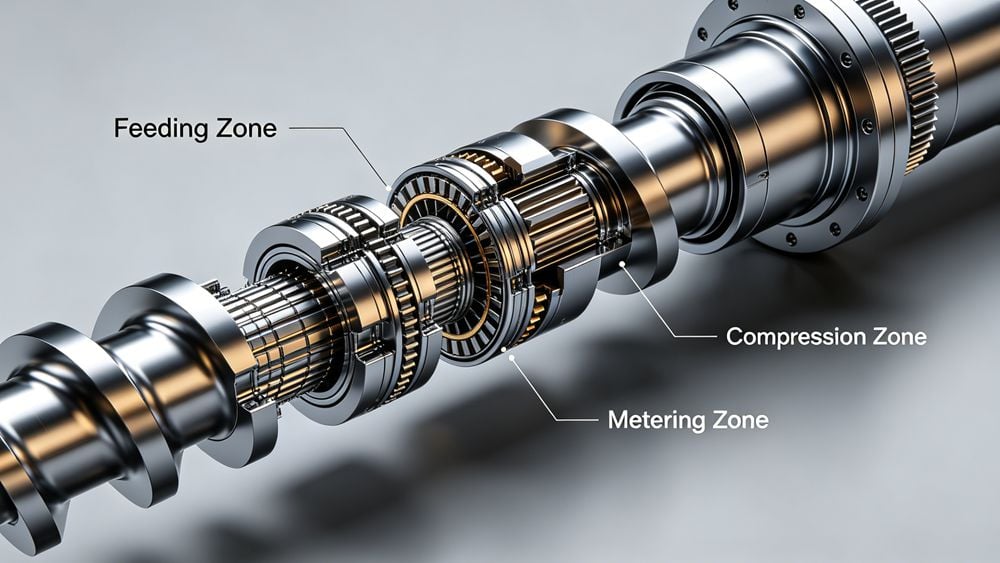
- Type: Single-flight, constant pitch, gradual compression screw with a non-return valve (check ring).
- L/D Ratio (Length/Diameter): 15:1 to 20:1.
- Compression Ratio: 2:1 to 3:1.
結論
Mastering PC injection molding requires a balance of thermal control and pressure management. By strictly controlling moisture and adhering to the temperature and screw speed guidelines above, you can produce high-clarity, impact-resistant parts with minimal internal stress.
[^1]: Explore the advantages of Polycarbonate (PC) to understand its applications and benefits in various industries. [^2]: Understand the importance of drying Polycarbonate to ensure optimal processing and part quality. [^3]: Find out the best injection temperature settings for Polycarbonate to ensure quality and performance. [^4]: Explore how injection pressure affects the molding process and the final properties of Polycarbonate parts. [^5]: Explore the relationship between mold temperature and the quality of Polycarbonate parts in injection molding. [^6]: Learn how screw speed and back pressure influence the injection molding process and material quality.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean