 한국어



Sink marks are one of the most common and frustrating defects in injection molding. If you’ve ever noticed a localized depression or micro-dimple on the surface of a plastic part, you’re dealing with sink marks.
While often considered a cosmetic issue, severe sink marks can indicate structural weaknesses and residual stresses. In this comprehensive guide, we’ll break down why sink marks occur, how material selection plays a role, and actionable strategies to fix them.
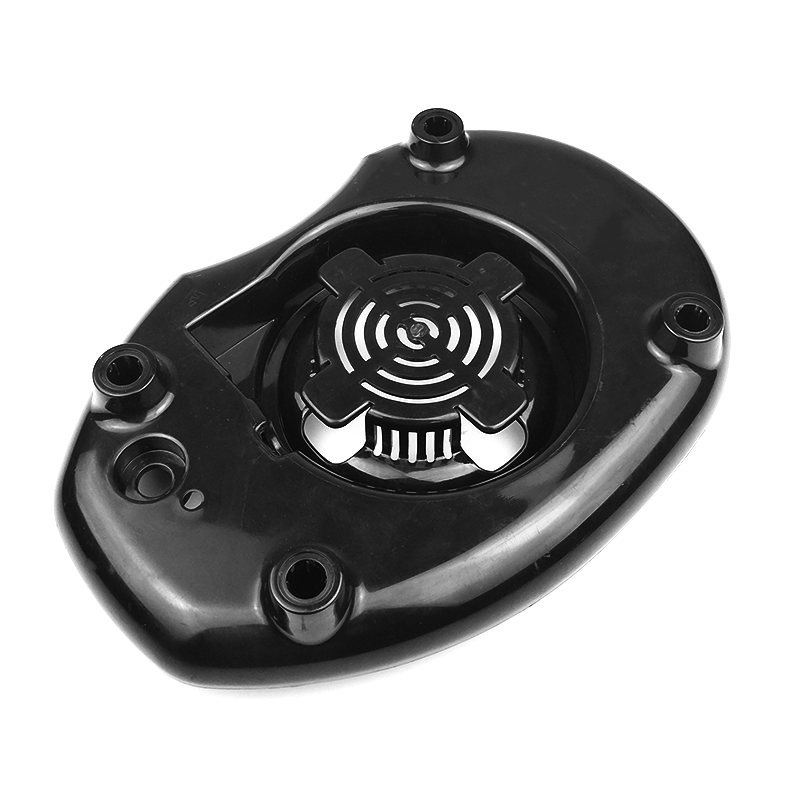
What Exactly is a Sink Mark?
Sink marks are localized depressions that occur when the interior of a thick plastic section shrinks more than the exterior. They typically appear in areas where the wall thickness increases, such as behind ribs, bosses, or near external corners.
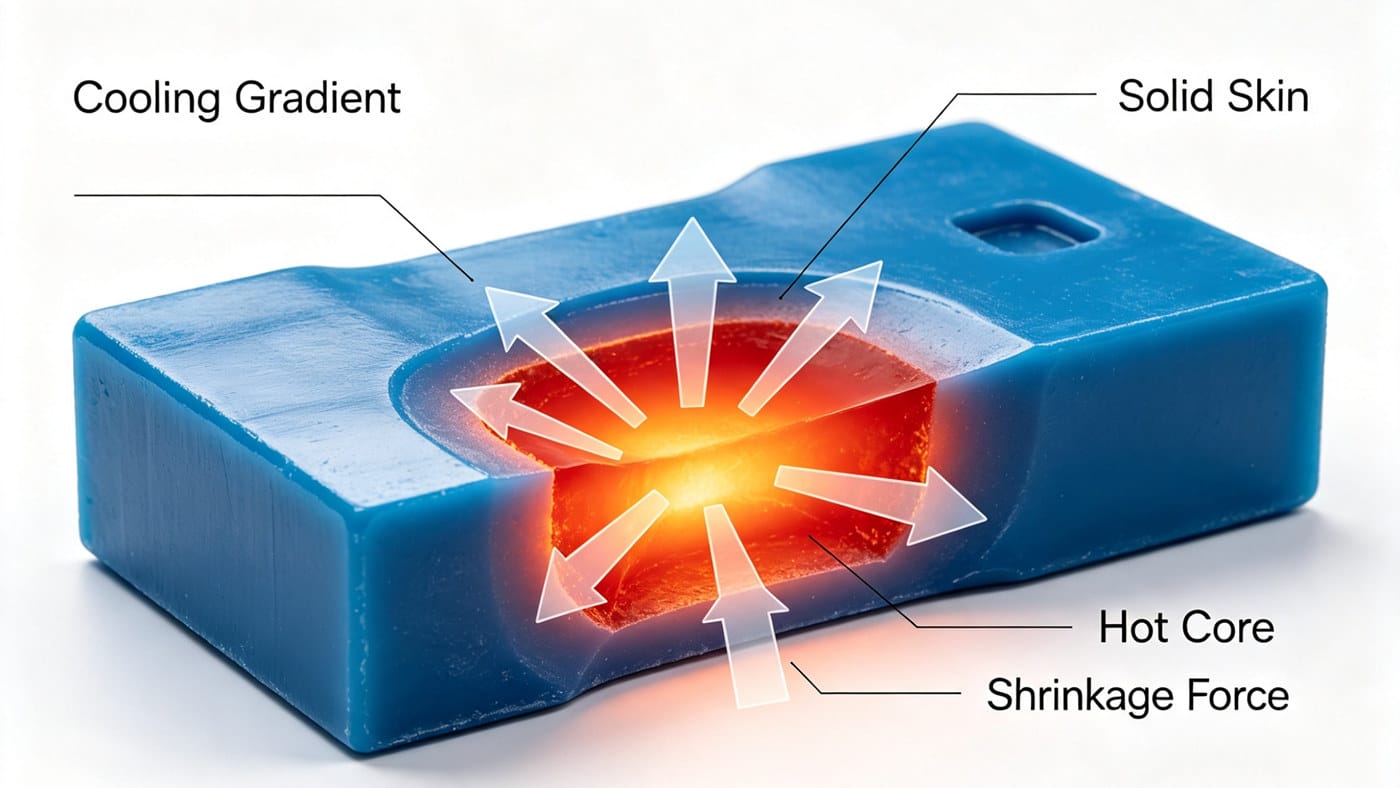
The fundamental cause is differential cooling and shrinkage. Thermoplastics have a high coefficient of thermal expansion. As the molten plastic cools inside the mold, it shrinks. If the core of a thick section remains molten and hot while the outer skin has already solidified, the cooling core will pull the semi-solid surface inward, creating a dent. For a full breakdown of root causes and mold-level fixes, read our dedicated troubleshooting guide: Troubleshooting Injection Molding Sink Marks: Causes & Solutions.
The Science Behind the Defect: Why Does It Happen?
To fix sink marks, you must understand the thermodynamics of the mold cavity.
- Cooling Rate Differences: Thin sections and sharp corners cool and solidify rapidly because they have maximum contact with the cold mold walls.
- The "Hot Core" Effect: The center of thick sections is furthest from the cooling channels. It retains heat the longest and is the last area to solidify.
- The Pulling Force: As the hot core finally cools and shrinks, it lacks sufficient molten material to compensate for the volume loss. It pulls inward on the already rigid outer skin, causing the sink mark.
How Material Selection Impacts Shrinkage
Not all plastics are created equal. The base resin you choose dictates how aggressively your part will shrink.
| Material Type | 수축률 | Sink Mark Risk | Examples |
|---|---|---|---|
| Semi-Crystalline | High (1.5% - 3.0%) | ? Very High | PP, PE, PA (Nylon), POM |
| Amorphous | Low (0.4% - 0.7%) | ? Low | ABS, PC, PS, PMMA |
| Filled/Reinforced | Very Low (0.1% - 0.5%) | ? Very Low | Glass-filled Nylon, Mineral-filled PP |
Pro Tip: If you are designing a part prone to sink marks and have material flexibility, switching from a semi-crystalline resin to an amorphous or glass-filled alternative can drastically reduce shrinkage. To learn more about resin shrinkage characteristics that drive sink formation, check our article: Injection Molding Shrinkage: How Temperature & Speed Affect Quality.
Process & Design Solutions to Eliminate Sink Marks
Fixing sink marks usually requires a combination of design adjustments, process tuning, and mold modifications.
1. Optimize Part Design (The Best Prevention)
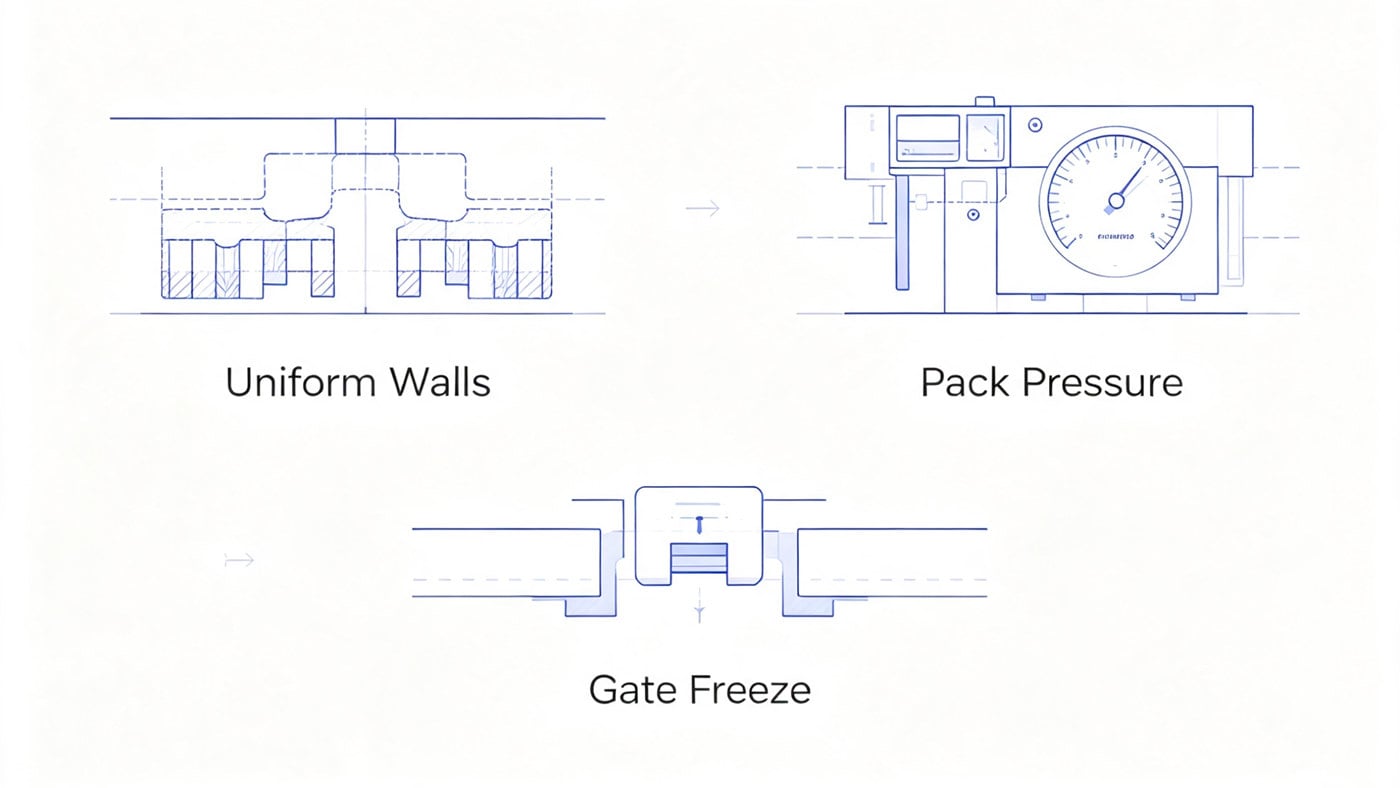
- Maintain Uniform Wall Thickness: This is the golden rule of injection molding. Avoid sudden transitions.
- Core Out Thick Sections: If a thick boss or rib is necessary, hollow it out to reduce the overall mass.
- Rib Thickness Guidelines: Ribs should generally be no thicker than 50% to 60% of the adjacent nominal wall thickness.
2. Fine-Tune the Injection Process
If the design is locked, you can try adjusting the molding parameters:
- Increase Packing/Holding Pressure: This forces more material into the cavity to compensate for volumetric shrinkage.
- Extend Packing Time: Crucial Note: The packing pressure is only effective as long as the gate remains open (molten). If your gate freezes off too early, extending pack time will do absolutely nothing. You may need to increase nozzle/mold temperature or gate size to keep the gate open longer.
- Optimize Cooling: Ensure cooling is as uniform as possible. Faster overall cooling reduces the time window for shrinkage.
Nearly all common molding defects including sink marks can be resolved with calibrated machine parameters; see our full parameter tuning guide for step-by-step adjustments: 사출 성형 파라미터 조정 가이드.
The Hidden Danger: Residual Stress
Don't ignore sink marks just because they look bad. A sink mark is a physical manifestation of uneven shrinkage. This differential shrinkage creates internal residual stresses within the polymer matrix.
These hidden stresses can lead to:
- Reduced impact strength (the part becomes brittle).
- Lower heat deflection temperature.
- Premature failure under load or chemical exposure.
- Post-molding warpage.
Final Thoughts
Eliminating sink marks requires a holistic approach. Always start with good part design—uniform walls and properly sized ribs. When issues arise, analyze your material's shrinkage rate and ensure your packing phase is actually reaching the cavity before the gate freezes.
Are you still struggling with surface defects on your injection molding parts? Drop a comment below or contact our engineering team for a free design-for-manufacturability (DFM) review!
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean