 한국어



If you’re involved in injection molding—whether as a designer, manufacturer, or hobbyist—understanding three critical plastic properties is non-negotiable: shrinkage, flowability, and crystallinity. These properties directly impact part quality, mold design, and production efficiency.
In this guide, we break down each concept in plain language, plus actionable strategies to optimize your molding process. Let’s dive in!
Plastic Shrinkage: What It Is & How to Control It
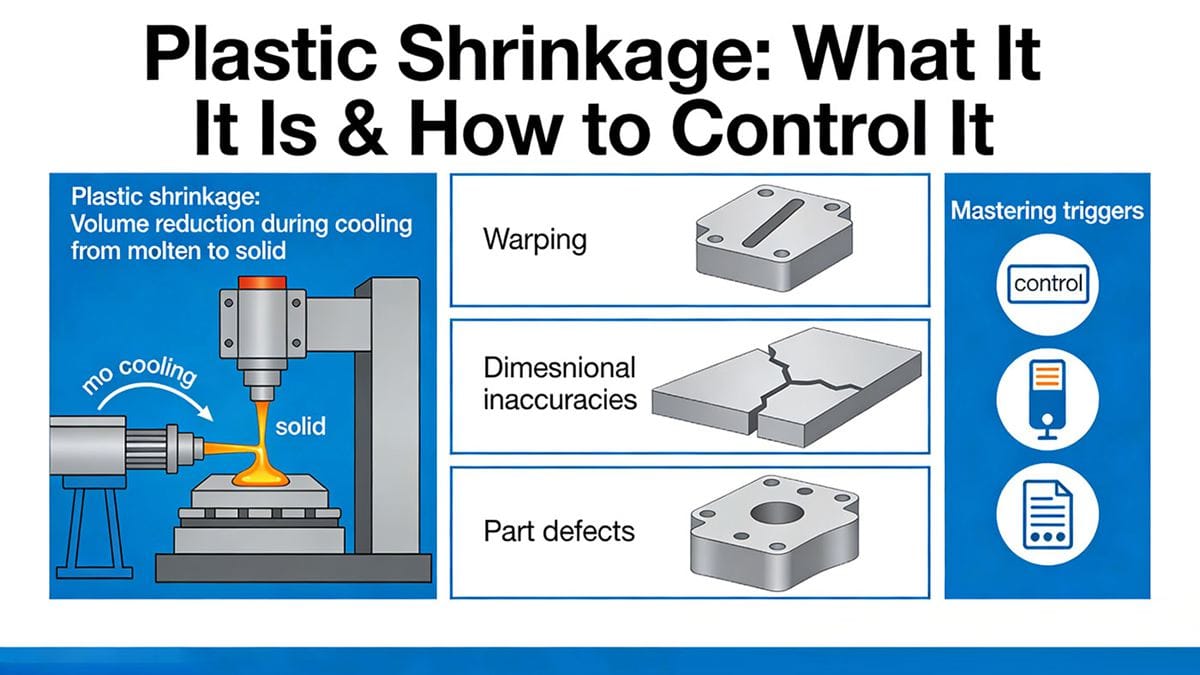
Plastic shrinkage refers to the volume reduction of thermoplastic materials as they cool from molten to solid state during injection molding. Uncontrolled shrinkage causes warping, dimensional inaccuracies, and part defects—so mastering its triggers is key to successful molding.
Key Factors Affecting Plastic Shrinkage in Injection Molding
1.1 Plastic Material Type
Thermoplastics have higher shrinkage rates than thermosets due to crystallization, internal stress, and molecular orientation during cooling. For example:
Crystalline plastics (e.g., PE, PP, PA) shrink more than amorphous plastics (e.g., PMMA, PC)
Post-molding shrinkage (after annealing or moisture conditioning) is also more significant in thermoplastics
1.2 Part Design & Geometry
벽 두께: Thicker parts cool slower, forming a denser inner layer that shrinks more. Aim for uniform wall thickness to avoid uneven shrinkage.
Inserts: The number, layout, and material of inserts alter flow direction and shrinkage resistance. Metal inserts reduce local shrinkage but may cause stress concentrations.
1.3 Gate Design (Type, Size, Location)
Gates control how molten plastic fills the mold—directly impacting shrinkage:
Large, direct gates minimize shrinkage but increase directional shrinkage (anisotropy)
Wide, short gates reduce directional shrinkage
Areas near gates or parallel to flow paths shrink more than distant or perpendicular sections
1.4 Injection Molding Process Parameters
Adjust these settings to reduce shrinkage:
Mold temperature: Lower mold temperature speeds cooling, reducing shrinkage (critical for crystalline plastics)
Holding pressure & time: Higher pressure + longer holding time = less shrinkage (but more directional shrinkage)
사출 압력: Increased pressure reduces viscosity and elastic recovery, lowering shrinkage
Melt temperature: Avoid excessive melt temperature—higher temps increase shrinkage
1.5 Mold Design Tips for Shrinkage Control
For high-precision parts, follow this workflow:
Test mold with initial gating and process parameters
Measure part dimensions 24 hours after ejection (allow for post-molding shrinkage)
Adjust cavity dimensions based on actual shrinkage data
Fine-tune process parameters (e.g., mold temperature, holding time) for final optimization
Plastic Flowability: How to Ensure Proper Mold Filling
Flowability (or melt flow) describes how easily molten plastic flows through the mold’s runners, gates, and cavities. Poor flowability leads to incomplete filling, weld lines, and burn marks—while excessive flow can cause flash.
How to Measure Plastic Flowability
Key metrics to evaluate flowability:
Melt Flow Index (MFI/MFR): Higher values = better flow
Archimedean Spiral Flow Length: Longer flow = better flowability
Flow Ratio (Flow Length ÷ Wall Thickness): Ideal ratio = 150–200 for most plastics
Apparent Viscosity: Lower viscosity = better flow
Common Plastics Ranked by Flowability (Injection Molding)
| Flowability Grade | Plastic Materials | Best For |
|---|---|---|
| 좋아요 | PA, PE, PS, PP, CA, Poly(4-methyl-1-pentene) | Thin-walled parts, complex geometries |
| Medium | ABS, AS, PMMA, POM, PPO | General-purpose parts with moderate complexity |
| Poor | PC, Rigid PVC, PSU, PAS, Fluoroplastics | Thick-walled parts, simple shapes |
Factors That Improve or Reduce Flowability
2.1 Temperature
Temperature-sensitive plastics (PS, PP, PA, ABS, PC): Increase melt temperature to boost flow
Temperature-insensitive plastics (PE, POM): Temperature changes have minimal effect—focus on pressure instead
2.2 Injection Pressure
Higher pressure increases shear stress, improving flow (critical for low-flow plastics like PE and POM)
Avoid over-pressurization, which causes flash and stress marks
2.3 Mold Design for Optimal Flow
Use a streamlined gating system (short, wide runners)
Ensure smooth cavity surfaces (reduce flow resistance)
Add proper venting (prevents air traps that block flow)
Design uniform cooling systems (avoids cold spots that thicken melt)
Plastic Crystallinity: What It Means for Molding
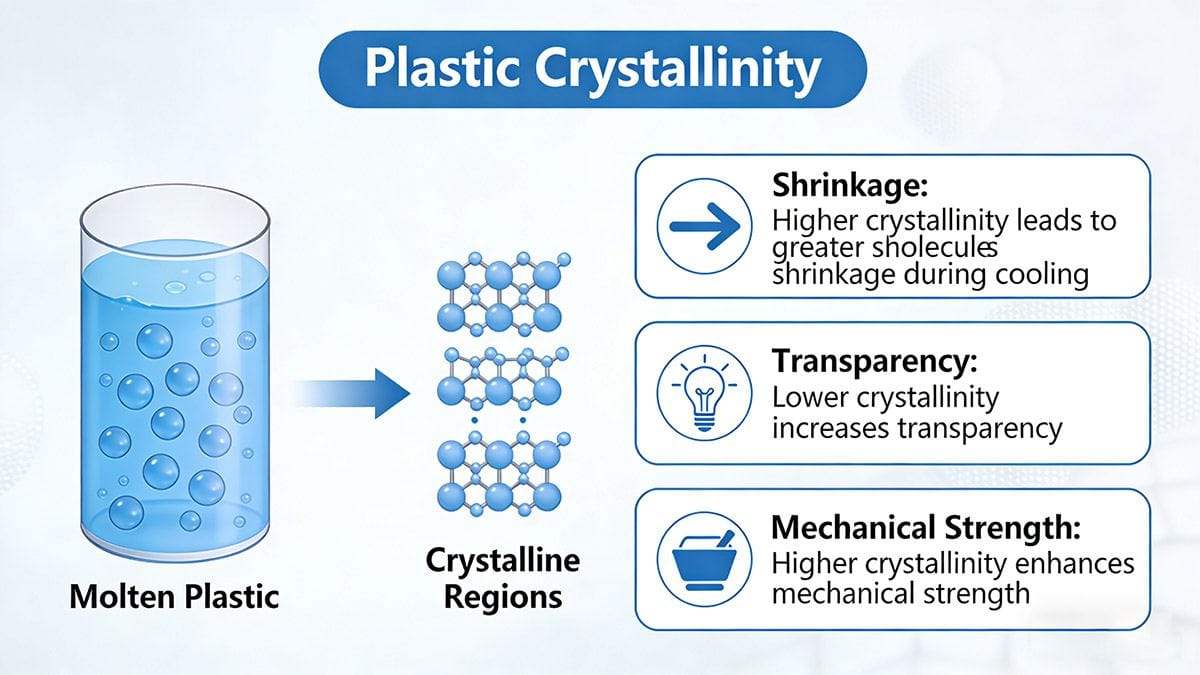
Crystallinity refers to the degree to which polymer molecules arrange into ordered, repeating structures as molten plastic cools. This property impacts shrinkage, transparency, and mechanical strength.
Crystalline vs. Amorphous Plastics: Key Differences
| Property | Crystalline Plastics | Amorphous Plastics |
|---|---|---|
| Structure | Ordered molecular arrangement | Disordered molecular arrangement |
| 투명성 | Opaque/translucent (e.g., POM, PE) | Transparent (e.g., PMMA, PC) |
| Shrinkage | Higher (5–15%) | Lower (0.5–3%) |
| Melting Point | Sharp (specific temperature) | Gradual softening range |
| Impact Strength | Better at low temperatures | Less consistent |
| Exceptions | Poly(4-methyl-1-pentene) (crystalline + transparent) | ABS (amorphous + opaque) |
Practical Implications for Injection Molding
Crystalline plastics (PE, PP, PA, POM):
Require more heat to melt (use machines with high plasticizing capacity)
Need controlled cooling (uniform mold temperature prevents uneven crystallization)
Higher shrinkage = adjust mold dimensions and holding pressure accordingly
Amorphous plastics (PMMA, PC, ABS):
Lower shrinkage = easier to achieve dimensional accuracy
Cool faster = shorter cycle times
More prone to stress marks = avoid rapid cooling or over-pressurization
Final Tips for Injection Molding Success
- Always check the material datasheet for shrinkage rates, flowability metrics, and crystallinity data
- Test small batches first to optimize process parameters (mold temp, pressure, cooling time)
- For complex parts, use simulation software to predict shrinkage and flow issues before molding
- Match mold design to plastic properties: e.g., wider gates for low-flow plastics, uniform walls for crystalline plastics
By mastering these three core properties, you’ll reduce defects, improve plastic part quality, and streamline your injection molding process.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean