 Français



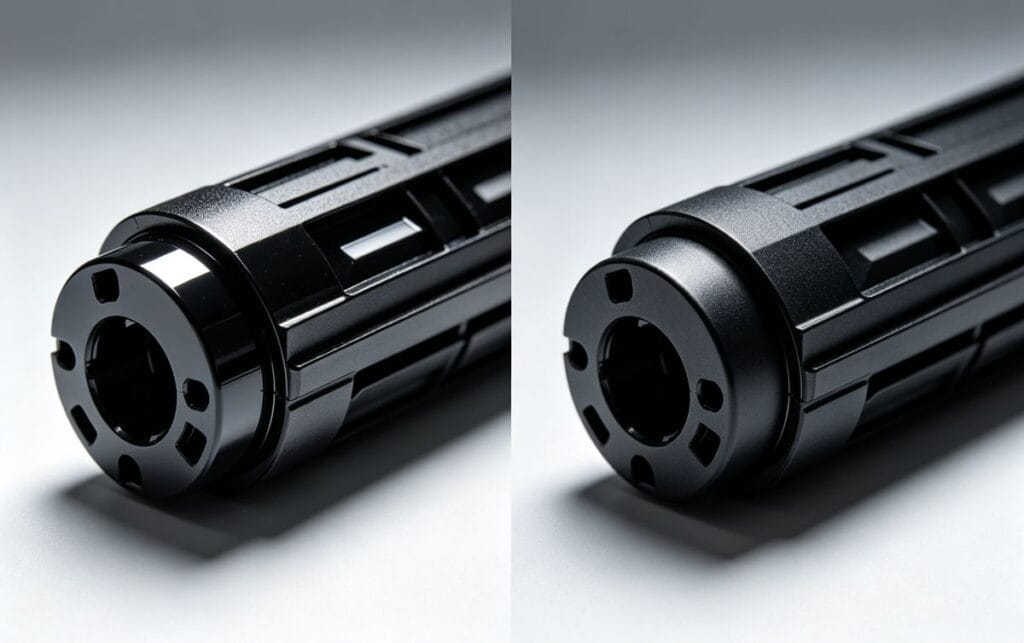
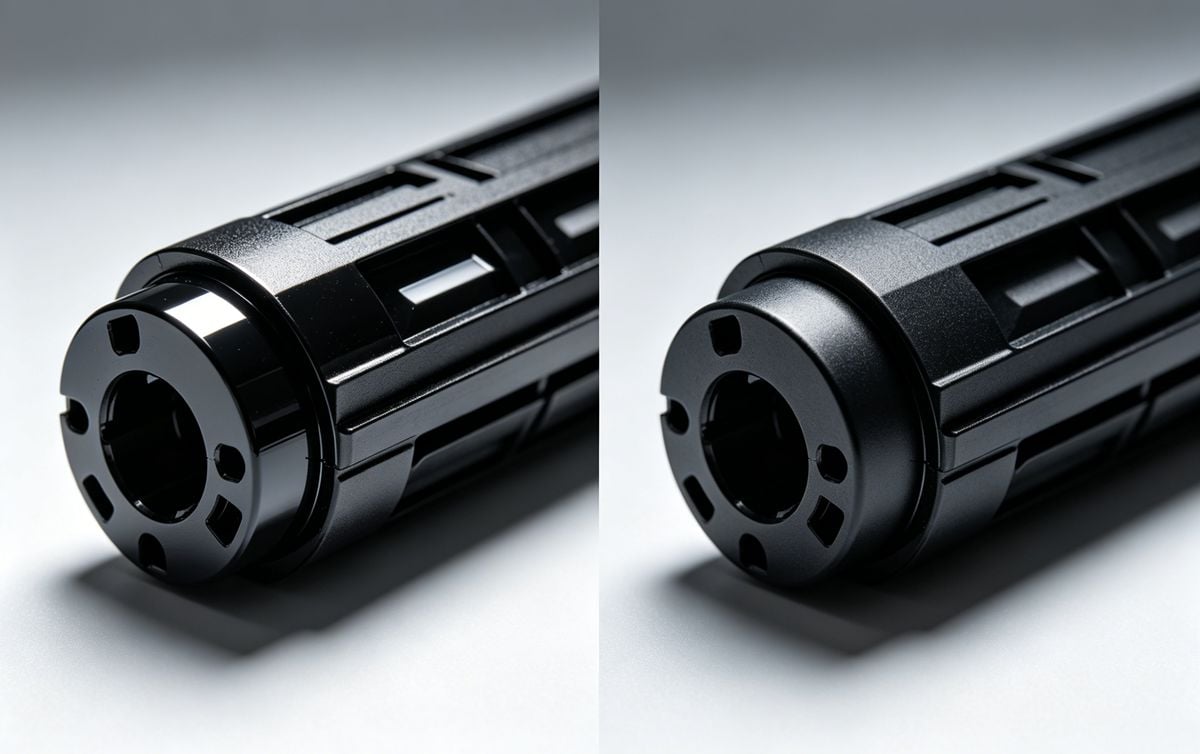
Achieving the perfect surface finish in moulage par injection de plastique is critical for product quality. However, manufacturers often encounter surface gloss defects, resulting in dull, matte, or uneven finishes.
Generally, these defects stem from three main categories: Mold Faults, Improper Molding Conditions, et Raw Material Issues. This guide breaks down each cause and provides actionable solutions.
Mold Faults and Design Issues
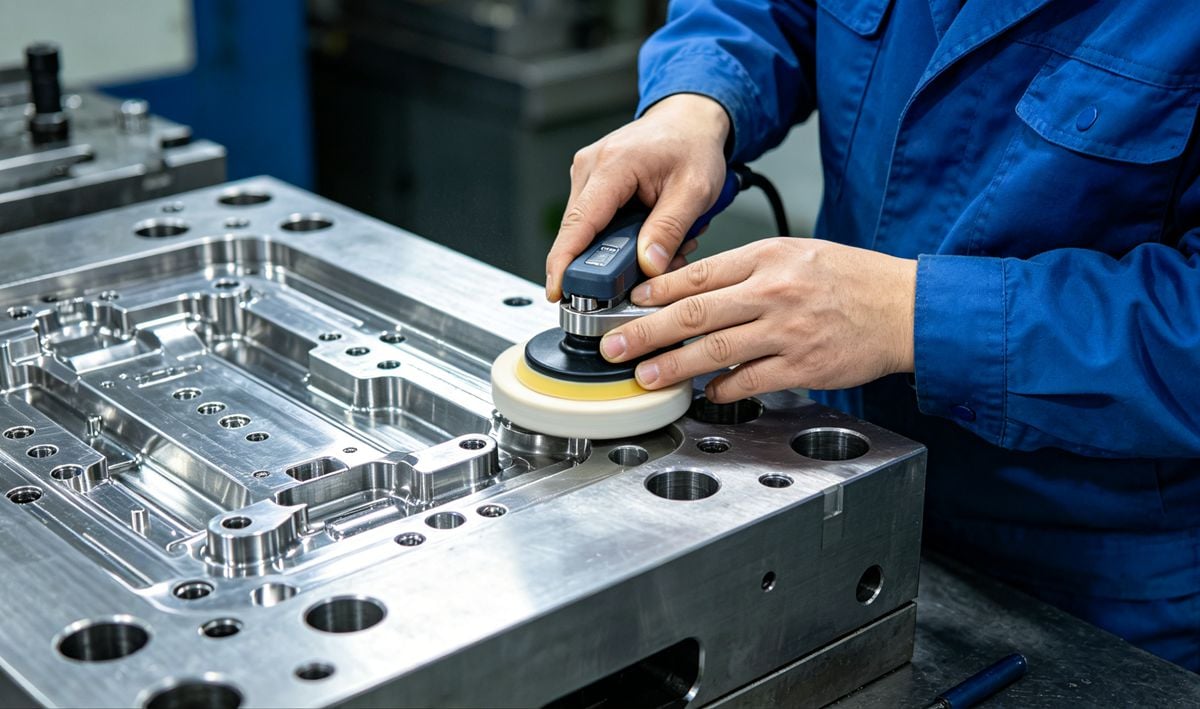
Since the plastic part is a reproduction of the mold cavity, the condition of the mold is paramount. If the mold surface has scratches, corrosion, or micropores, these imperfections will be replicated on the plastic part.
Common Mold-Related Causes:
- Surface Finish: The cavity surface must have excellent smoothness. Polishing or chrome plating the cavity surface is recommended.
- Contamination: Oil, moisture, or excessive release agent on the cavity surface can cause darkening. Keep the mold clean and use release agents sparingly and correctly.
- Mold Temperature: This is a critical factor.
- Too Low: The melt solidifies instantly upon contact, preventing the plastic from replicating the mold's texture, leading to poor gloss.
- Solution : Augmentez le mold temperature. Using warm water in the cooling circuit helps transfer heat quickly without extending the cycle time significantly.
- Design Flaws: Small draft angles, sudden changes in wall thickness, overly thick ribs, or small gates can cause turbulence or poor flow. Poor venting also traps air, affecting the finish.
Improper Control of Molding Conditions
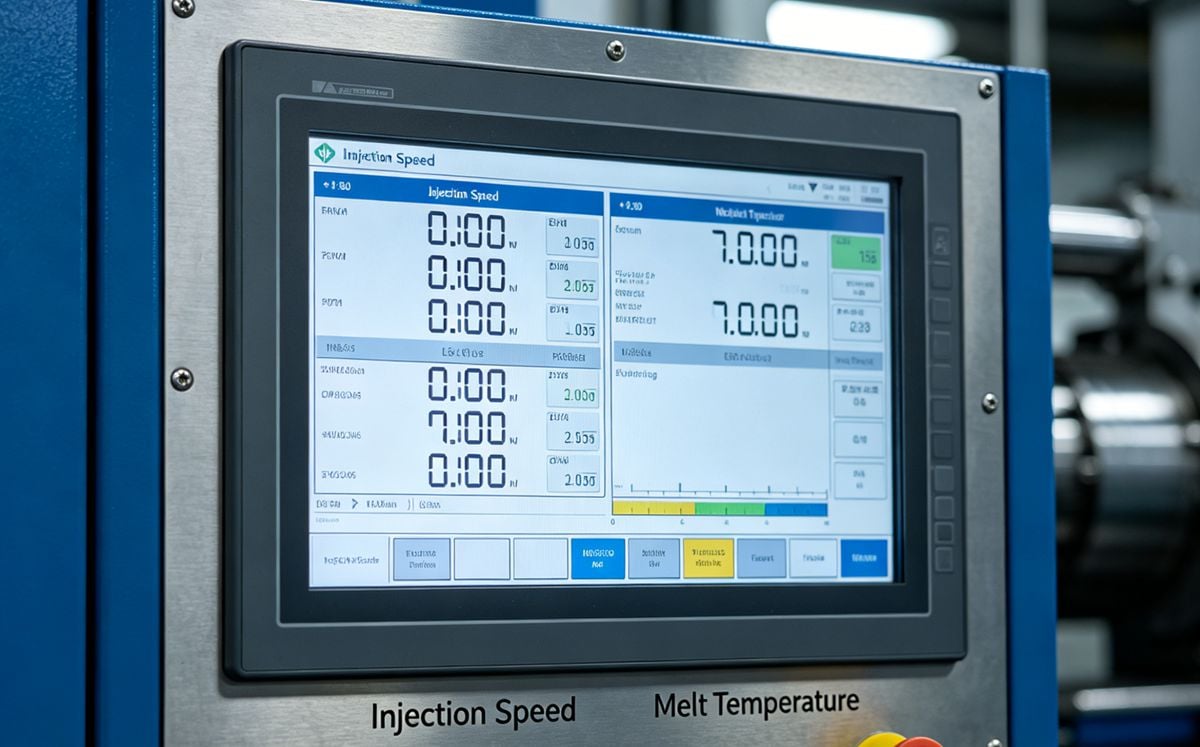
Even with a perfect mold, incorrect machine settings can ruin the surface finish. Parameters such as speed, pressure, and temperature must be balanced.
Key Adjustments:
- Injection Speed & Pressure: If the speed is too fast or too slow, or if injection pressure is too low, the surface may appear dull.
- Holding Pressure & Time: Insufficient holding time or pressure prevents the material from packing tightly against the mold surface.
- Nozzle Temperature: A cold nozzle or low barrel temperature results in poor plasticization.
- Fiber Reinforcement: For reinforced plastics, poor dispersion of fillers can lead to a "silver foil" appearance or exposed fibers.
Troubleshooting Specific Symptoms:
- Dark areas near the gate: Try reducing vitesse d'injection, relocating the gate, increasing gate size, or adding fillet transitions at thickness changes.
- Milky white layer: Usually indicates the injection speed is too high; reduce it slightly.
- Filler Dispersion Issues: Switch to a resin with better flow or use a screw with stronger mixing capabilities.
Raw Material Incompatibility
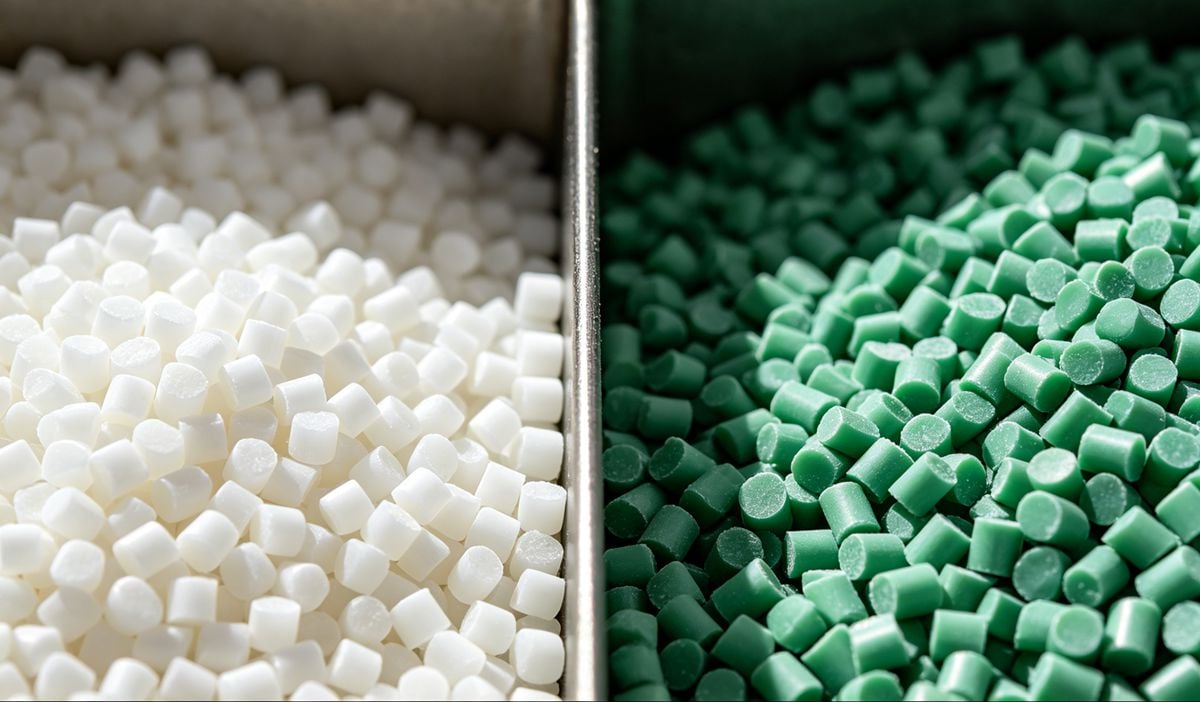
Sometimes the issue lies within the plastic pellets themselves. Using materials that do not meet processing requirements is a common cause of gloss failure.
Material Checklist:
| Issue Category | Cause | Recommended Solution |
|---|---|---|
| Moisture | High moisture or volatile content creates condensation between melt and mold. | Pre-dry the raw material thoroughly. |
| Degradation | Resin or colorant decomposition due to heat. | Use higher temperature-resistant resins/colorants. |
| Flow Rate | Material viscosity is too high (poor flow). | Switch to free-flowing resin, add lubricant, or increase temp. |
| Contamination | Mixed foreign materials or incompatible polymers. | Replace with virgin/new material. |
| Particle Size | Uneven particle size distribution. | Sieve the material to remove outliers. |
| Crystallinity | Uneven cooling in crystalline resins (e.g., PP, PE). | Control mold temp carefully; cool thick parts in a cold press immediately after ejection. |
| Recycled Material | Too high a percentage of regrind affects uniformity. | Reduce the ratio of recycled material. |
Résumé
Fixing surface gloss defects requires a systematic approach. Start by inspecting the mold surface and temperature, then optimize your injection parameters (speed/pressure), and finally, verify the quality and dryness of your raw materials.
À propos de l'auteur

Alex Yu
Ideal Pro Manufacturing
Alex est le cofondateur d’Ideal Pro, mais lorsqu’il ne supervise pas des projets clés ou ne dirige pas l’équipe technique, vous le trouverez sans doute en train de faire une longue balade à vélo, à la recherche du meilleur café de la ville, ou en train de planifier sa prochaine aventure de voyage. Fort de plus de 20 ans d’expérience dans le commerce international et la gestion de projets, il a tout vu : délais serrés, problèmes techniques complexes et tout ce qui se trouve entre les deux. Il est convaincu qu’un travail de qualité naît d’un esprit bien reposé et d’une bonne tasse de café, et il apporte cette même curiosité et ce même souci du détail à chaque projet qu’il entreprend. Lorsqu’il n’est pas au bureau, il se trouve généralement en plein air, à explorer de nouveaux endroits et à glaner des anecdotes à partager.




 English
 French
 Dutch
 German
 Japanese
 Korean