 Deutsch



Einführung
Stress cracking is a common failure mode in Kunststoffteile[^1] that can lead to costly recalls and product failures. By understanding the root causes and implementing smart design principles, engineers can significantly reduce internal stresses. This guide covers three critical areas: part geometry, metal insert integration, und hole design.
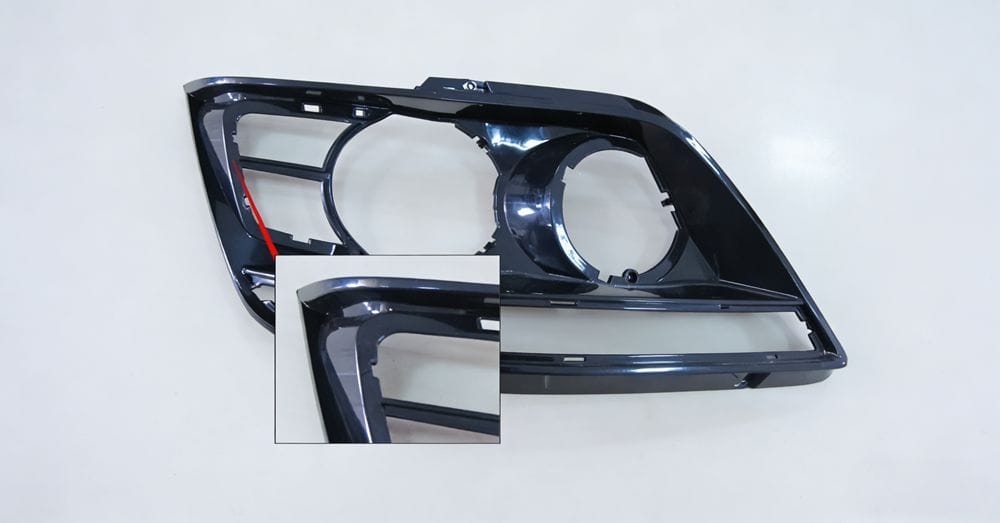
Optimizing Plastic Part Shape and Dimensions
The geometry of a plastic part plays a pivotal role in how internal stresses are distributed during cooling and usage.
Key Design Principles
- Maintain Continuity: Ensure the outer shape of the product remains as continuous as possible.
- Avoid Stress Concentrators: Strictly avoid sharp corners, right angles, notches, and sudden changes in cross-sectional area.
- Fillet Radii:
- Inner Corners: The inner fillet radius should be greater than 70% of the thickness of the thinner adjacent wall.
- Outer Corners: Determine based on the overall part geometry to maintain uniform wall thickness.
Managing Wall Thickness
Variations in wall thickness lead to uneven cooling rates, causing both cooling internal stress und orientation internal stress.
- Uniformity is Key: Design parts with uniform wall thickness whenever possible.
- Gradual Transitions: If varying thicknesses are unavoidable, ensure a schrittweiser Übergang between thick and thin sections to minimize stress concentration.
Best Practices for Metal Insert Design
Integrating metal inserts into plastic parts introduces significant challenges due to thermal expansion differences. Plastics typically have a Coefficient of Thermal Expansion (CTE) 5 to 10 times higher than metals.
During cooling, the plastic shrinks more than the metal, gripping the insert tightly. This creates compressive stress in the inner plastic layer and tensile stress in the outer layer, leading to potential cracking.
Strategies to Minimize Insert-Induced Stress
To mitigate these risks, follow these engineering guidelines:
- Material Selection:
- Whenever possible, replace metal inserts with plastic inserts.
- If metal is necessary, choose materials with a CTE closer to the plastic, such as Aluminium, Aluminiumlegierungen, oder Kupfer.
- Buffer Layers: Apply a rubber or polyurethane elastic buffer coating to the metal insert. Ensure this layer does not melt during molding to effectively reduce shrinkage differences.
- Surface Preparation:
- Perform degreasing treatment on metal inserts to prevent oils from accelerating stress cracking[^2].
- Preheat the metal inserts before molding to reduce the thermal shock.
- Geometry and Thickness:
- Ensure sufficient plastic thickness around the insert.
- Für Aluminum inserts: Plastic thickness ($h$) $ge$ 0.8 $times$ Insert Diameter ($D$).
- Für Copper inserts: Plastic thickness ($h$) $ge$ 0.9 $times$ Insert Diameter ($D$).
- Design inserts with smooth shapes, preferably featuring fine knurling to improve mechanical bonding without sharp edges.
- Ensure sufficient plastic thickness around the insert.
Strategic Hole Design in Plastic Parts
The shape, number, and location of holes significantly impact stress concentration levels.
Rules for Hole Geometry
- Avoid Angular Shapes: Never use prismatic, rectangular, square, or polygonal holes, as their corners act as severe stress concentrators.
- Preferred Shapes:
- Circular Holes: The standard safe choice.
- Elliptical Holes: Often the most effective solution. Orient the major axis of the ellipse parallel to the direction of the external force.
Advanced Techniques for Stress Dispersion
If circular holes are required, consider these methods to mimic the benefits of elliptical holes:
- Auxiliary Process Holes: Add equal-diameter process holes adjacent to the main hole. Align the center line connecting the holes parallel to the external force.
- Symmetric Slots: Cut symmetric slots around the circular hole to help disperse internal stress effectively.
Fazit
Preventing stress cracking starts at the drawing board. By adhering to principles of geometric continuity, carefully managing metal insert interfaces, and optimizing hole configurations, designers can create robust plastic products that withstand real-world demands. Implement these strategies to improve product longevity and reduce failure rates.
[^1]: Explore this resource to discover essential design practices that enhance the durability and performance of plastic components. [^2]: Understanding stress cracking is crucial for engineers to prevent costly product failures.
Über den Autor

Alex Yu
Ideal Pro Manufacturing
Alex ist Mitbegründer von Ideal Pro, doch wenn er nicht gerade wichtige Projekte beaufsichtigt oder das technische Team leitet, trifft man ihn wahrscheinlich auf einer langen Radtour, auf der Suche nach dem besten Kaffee der Stadt oder bei der Planung seines nächsten Reiseabenteuers. Mit über 20 Jahren Erfahrung in den Bereichen internationaler Vertrieb und Projektmanagement hat er schon alles gesehen – enge Fristen, knifflige technische Probleme und alles, was dazwischen liegt. Er ist davon überzeugt, dass großartige Arbeit von einem ausgeruhten Geist und einer guten Tasse Kaffee entsteht, und er bringt dieselbe Neugier und Liebe zum Detail in jedes Projekt ein, das er übernimmt. Wenn er nicht im Büro ist, befindet er sich meist irgendwo im Freien, erkundet neue Orte und sammelt Geschichten, die er gerne weitergibt.




 English
 French
 Dutch
 German
 Japanese
 Korean