 Nederlands




What Is Short Shot?
Short shot (also called incomplete filling, underfill) occurs when molten plastic fails to completely fill the mold cavity before solidifying. This defect commonly appears in thin-walled sections, complex geometries, or flow-path endpoints, resulting in missing material and non-conforming parts. The core issue? Excessive flow resistance[^1] preventing melt advancement.
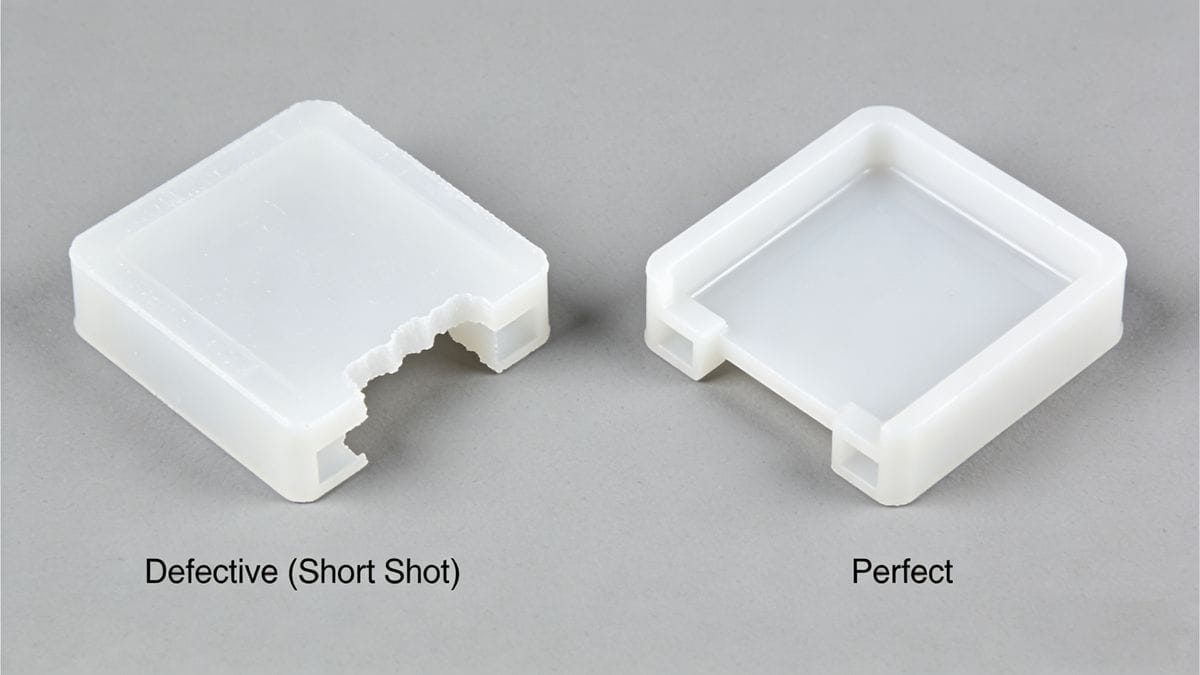
Key influencing factors include:
- Part wall thickness
- Mold & melt temperatures
- Injection pressure & speed[^2]
- Material rheology[^3]
- Gating/venting design
Below is a systematic, engineer-tested guide to diagnose and resolve short shots—optimized for production efficiency and quality control.
13 Root Causes & Actionable Solutions
1. Undersized Injection Molding Machine
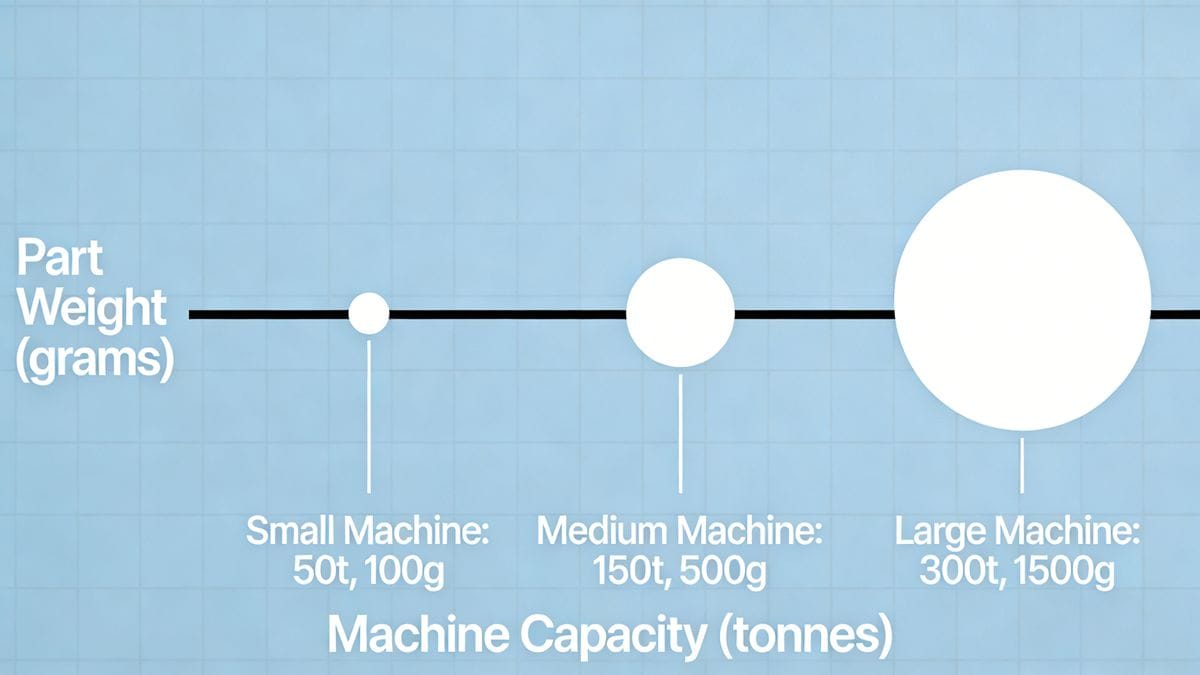
✅ Oplossing: Ensure machine shot capacity exceeds (part + runner) weight by ≥15%. Total shot weight ≤85% of machine’s plasticizing capacity.
[Image: Infographic comparing machine capacity vs. part weight requirements. Alt text: Injection molding machine sizing guide to prevent short shots]
2. Inconsistent Material Feeding
✅ Oplossing: Check for material bridging, non-uniform pellet size, or overheated feed throat. Clean hopper, install cooling jacket, or switch to gravimetric feeding.
3. Poor Material Flowability
✅ Oplossing:
- Enlarge gates, runners, sprue; optimize gate location
- Add flow-enhancing additives (per material specs)
- Reduce regrind ratio ( "When short shots persist after parameter tweaks, suspect mold design first. 70% of chronic short shots trace back to gating, venting, or thermal design—not machine settings."
> — Senior Process Engineer, Automotive Tier-1 Supplier
[^1]: Understanding flow resistance is crucial for optimizing injection molding processes and preventing defects. [^2]: Explore how these parameters influence the quality of molded parts and prevent defects. [^3]: Learn about material rheology to improve flow characteristics and enhance product quality.
Veelgestelde vragen
What Is Short Shot?
Short shot (also called incomplete filling, underfill) occurs when molten plastic fails to completely fill the mold cavity before solidifying. This defect commonly appears in thin-walled sections, complex geometries, or flow-path endpoints, resulting in missing material and non-conforming parts. The core issue? [Excessive flow resistance](https://ideal-pro.com/how-injection-speed-profiling-affects-injection-molding-part-quality-a-technical-guide/)[^1] preventing melt advancement.
Key influencing factors include: Part wall thickness Mold & melt temperatures [Injection pressure & speed](https://ideal-pro.com/how-injection-speed-profiling-affects-injection-molding-part-quality-a-technical-guide/)[^2] [Material rheology](https://ideal-pro.com/essential-injection-molding-process-knowledge-every-newcomer-should-know/)[^3] Gating/venting design
Below is a systematic, engineer-tested guide to diagnose and resolve short shots—optimized for production efficiency and quality control.
1. Undersized Injection Molding Machine
✅ Oplossing: Ensure machine shot capacity exceeds (part + runner) weight by ≥15%. Total shot weight ≤85% of machine’s plasticizing capacity. [Image: Infographic comparing machine capacity vs. part weight requirements. Alt text: Injection molding machine sizing guide to prevent short shots]
2. Inconsistent Material Feeding
✅ Oplossing: Check for material bridging, non-uniform pellet size, or overheated feed throat. Clean hopper, install cooling jacket, or switch to gravimetric feeding.
3. Poor Material Flowability
✅ Oplossing: Enlarge gates, runners, sprue; optimize gate location Add flow-enhancing additives (per material specs) Reduce regrind ratio (
4. Excessive Lubricant or Worn Components
✅ Oplossing: Reduce internal/external lubricant content. Inspect and replace worn screw, check valve, or barrel to minimize melt backflow.
Over de auteur

Alex Yu
Ideal Pro Manufacturing
Alex is medeoprichter van Ideal Pro, maar wanneer hij niet toezicht houdt op belangrijke projecten of leiding geeft aan het technische team, is hij waarschijnlijk bezig met een lange fietstocht, op zoek naar de beste koffie van de stad, of bezig met het plannen van zijn volgende reisavontuur. Met meer dan 20 jaar ervaring op het gebied van internationale handel en projectmanagement heeft hij het allemaal al meegemaakt: strakke deadlines, lastige technische vraagstukken en alles daartussenin. Hij is ervan overtuigd dat uitstekend werk voortkomt uit een uitgeruste geest en een goede kop koffie, en hij brengt diezelfde nieuwsgierigheid en oog voor detail mee in elk project dat hij aanneemt. Als hij niet op kantoor is, bevindt hij zich meestal ergens in de buitenlucht, waar hij nieuwe plekken verkent en verhalen verzamelt om te delen.




 English
 French
 Dutch
 German
 Japanese
 Korean