 한국어



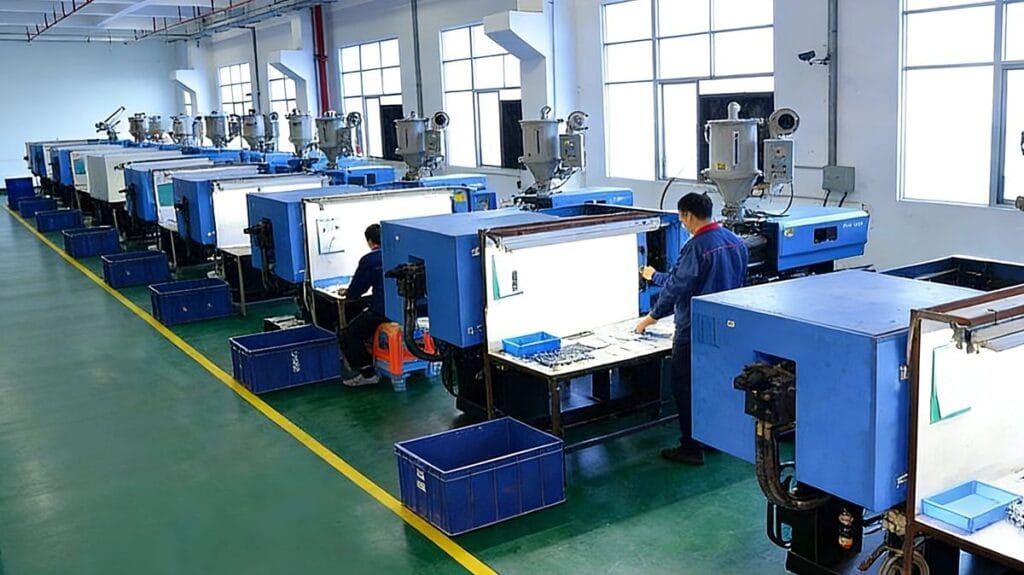
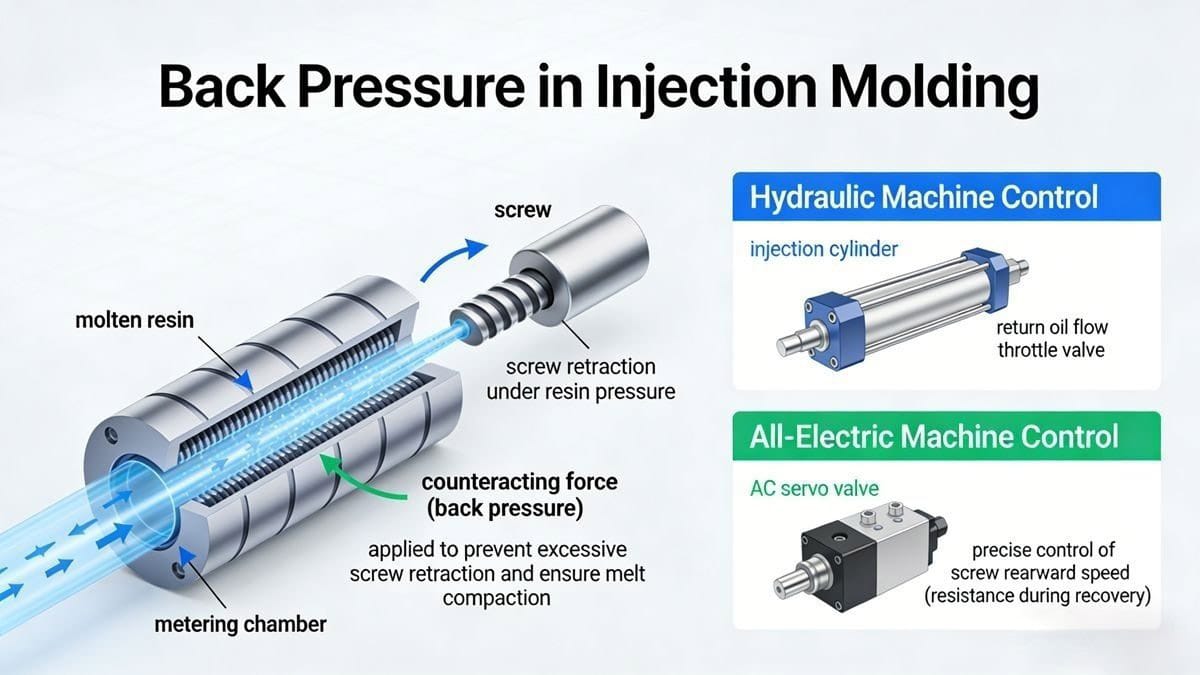
What Is Back Pressure in Injection Molding?
During the plastic melting and plasticization phase, molten resin continuously moves toward the front of the barrel (into the metering chamber), building up pressure that pushes the screw backward. To prevent excessive or uncontrolled screw retraction—and to ensure uniform compaction of the melt—a counteracting force is applied to the screw. This opposing resistance is called 역압[^1] (also known as plasticizing pressure[^2]).
In hydraulic injection molding machines, back pressure is controlled via a return oil flow throttle valve in the injection cylinder. In all-electric machines, it is regulated by an AC servo valve that precisely controls the screw’s rearward speed (i.e., resistance during recovery).
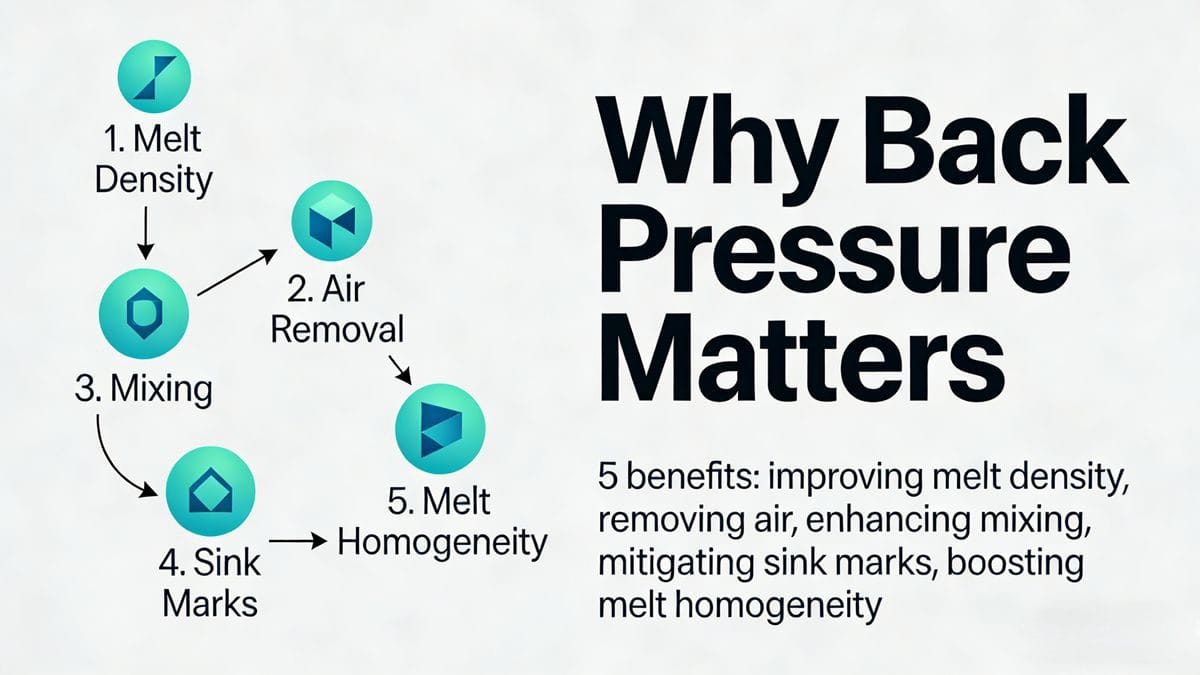
Why Back Pressure Matters: 5 Key Benefits of Proper Adjustment
When correctly set, back pressure significantly enhances both process stability and part quality:
Improves Melt Density & Shot Consistency
Higher back pressure compacts the melt in the barrel, increasing its density. This leads to more consistent shot volume, part weight, and dimensional stability—critical for tight-tolerance components.Removes Trapped Air & Reduces Surface Defects
The compression effect “squeezes out” entrapped air and volatiles, minimizing surface defects such as:- Silver streaks (gas marks)
- Internal voids/bubbles
- Uneven gloss or haze
Result: smoother, more cosmetically acceptable surfaces.
Enhances Mixing & Color Uniformity
By slowing screw retraction, back pressure extends residence time in the shear zone, improving dispersion of:- Colorants (pigments, masterbatches)
- Fillers (e.g., glass fiber, calcium carbonate)
This prevents color streaking, mottling, or inconsistent hue across parts.
Mitigates Sink Marks & Improves Flow at Edges
Optimized back pressure raises melt temperature slightly (via increased shear heating) and improves melt homogeneity—enhancing flow into thin sections, ribs, and corners. This reduces sink marks and improves filling of complex geometries.Boosts Melt Homogeneity & Eliminates Cold Slugs
Better plasticization yields a more uniform melt temperature profile, reducing cold flow lines and eliminating cold slug defects at the gate or runner.
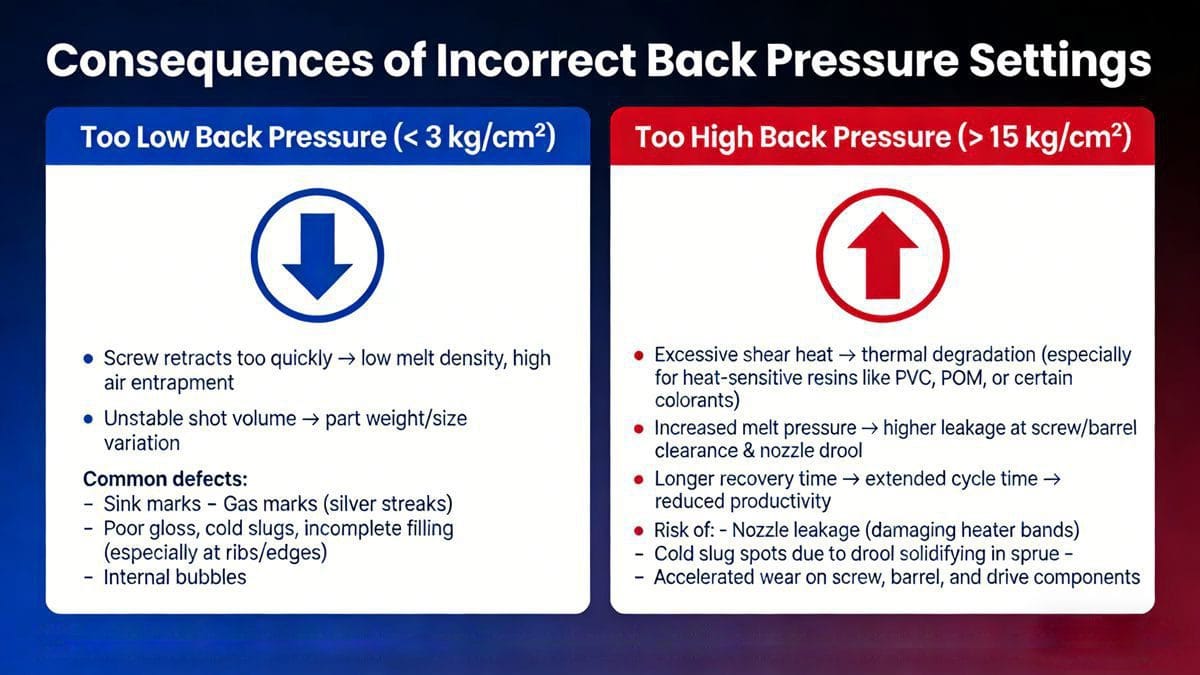
Consequences of Incorrect Back Pressure Settings
? Too Low Back Pressure ( 15 kg/cm²)
- Excessive shear heat → thermal degradation (especially for heat-sensitive resins like PVC, POM, or certain colorants)
- Increased melt pressure → higher leakage at screw/barrel clearance & nozzle drool
- Longer recovery time → extended cycle time → reduced productivity
- Risk of:
- Nozzle leakage (damaging heater bands)
- Cold slug spots due to drool solidifying in sprue
- Accelerated wear on screw, barrel, and drive components
> ⚠️ Note: For thermally sensitive materials, even moderate back pressure (8–10 kg/cm²) may require close monitoring of melt temperature.
How to Optimize Back Pressure: Practical Guidelines
Back pressure must be tuned based on:
- Resin type (e.g., PP vs. PC vs. TPU)
- Drying condition (moisture = more volatiles → needs higher back pressure)
- Part geometry (thin walls, large surface area, inserts)
- Quality requirements (cosmetic vs. structural)
Typical Range:
✅ 3–15 kg/cm² (≈ 0.3–1.5 MPa) for most engineering plastics
- Start low (e.g., 5 kg/cm²), then incrementally increase while monitoring:
- Melt temperature (avoid > material’s max processing temp)
- Recovery time (should not exceed 60–70% of total cycle time)
- Visual defects (gas marks, color streaks, sink)
When to Increase Back Pressure:
- Visible gas marks, color inconsistency, sink marks[^3]
- Large weight/size variation between shots
- Poor filling at edges or ribs
When to Decrease Back Pressure:
- Nozzle drool or leakage
- Material degradation (yellowing, black specks)
- Overly long recovery time
- Cold slugs or runner blockage
For multi-material runs (e.g., switching from ABS to PET), always recalibrate back pressure—material-specific viscosity and thermal behavior demand unique settings.
Final Thoughts: Back Pressure Is a Foundational Parameter
Back pressure is far more than a “fine-tuning” knob—it’s a core lever for controlling melt quality, part consistency, and overall process robustness. Ignoring it risks recurring defects, scrap, and inefficiency. Conversely, mastering back pressure enables:
- Higher first-pass yield
- Reduced need for post-molding correction
- Better repeatability across shifts and machines
Invest time in systematic back pressure trials—document melt temps, recovery times, and part inspections. Combine with DOE (Design of Experiments[^4]) for data-driven optimization.
> ? Pro Tip: Pair back pressure adjustments with screw rotation speed (RPM) and barrel temperature profiling for synergistic improvement.
[^1]: Understanding back pressure is crucial for optimizing injection molding processes and improving part quality. [^2]: Learn about plasticizing pressure to enhance your knowledge of injection molding techniques and their impact on product quality. [^3]: Understanding the causes of sink marks can help you improve the quality of your injection molded products. [^4]: Explore how Design of Experiments can help you systematically optimize injection molding parameters for better results.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean