 한국어



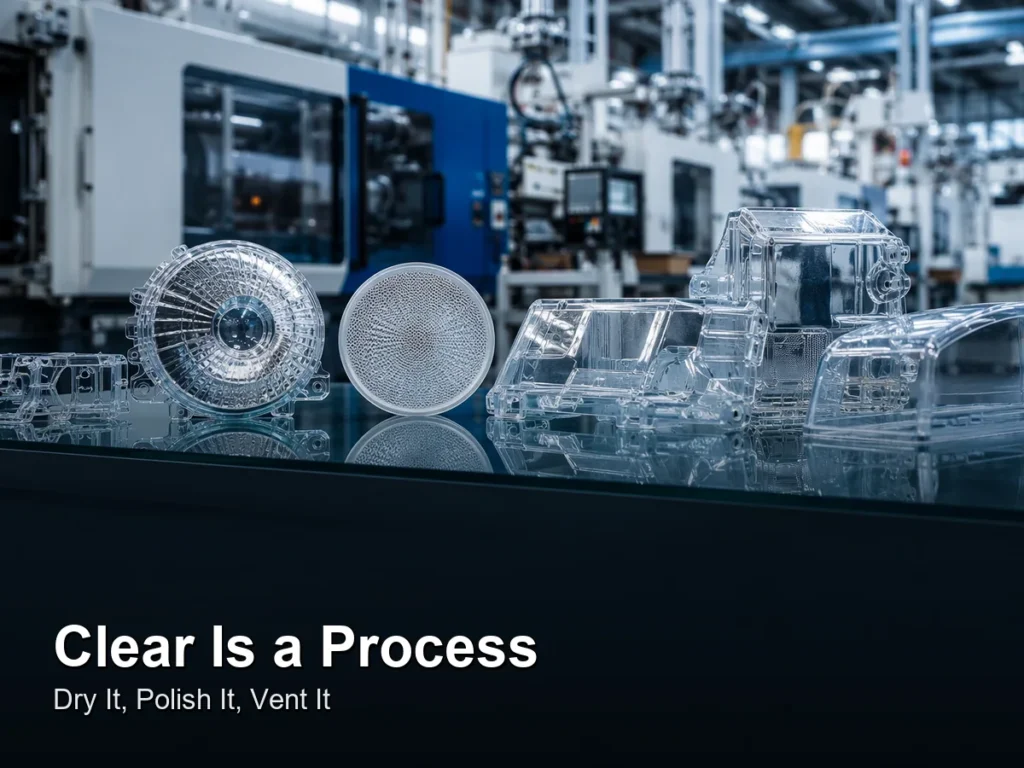
TL;DR the honest version: transparency is not bought with a material datasheet, it is earned by process discipline. Almost every clear part that fails does so because of moisture, contamination, a cold mold or a vent that was never designed — not because PC was the wrong resin. A supplier who quotes your lens without asking how you will dry the resin and what haze number you will accept is quoting a guess.
This guide is for the buyer specifying a lens, a diffuser, a sight window or a cosmetic transparent cover, and for the engineer tired of receiving “we will do our best on clarity” as an answer. It separates transparent from translucent in a way you can measure, tells you which defects come from which setting, and is straight about the things that cannot be fixed after the tool is cut.
Key Takeaways
- Transparent and translucent are different specifications, not different qualities of the same one. One is measured as light transmittance and the other as haze, and an LED diffuser needs the second one high while a lens needs it near zero.
- Drying is the first control, not a precaution. Polycarbonate and PMMA hydrolyse when molded wet, and hydrolysis shows up as gels, splay and a brittleness that no polishing removes.
- Regrind has no place in an optical part. Every thermal pass raises gel count and shifts colour; the saving is measured in resin, the loss is measured in yield.
- The mold steel is the optical surface. Polish grade, vent placement and ejection marks replicate 1:1 into your part — a scratch in the cavity is a scratch in the product, forever.
Why Trust This Guide on Transparent Parts?
The claim we are entitled to make: we mold clear and diffusing parts to a measured acceptance, which means we have also had to explain to a client why a lens they approved on a photograph failed under their own light source.
Author: Alex Yu, co-founder of Ideal Pro — 20+ years on molding programs from consumer optics to automotive lenses, 1000+ mold sets a year, Huzhou facility. LinkedIn.
Basis: our own molding and inspection records 2023-2026, our tool-room polish practice, and published optical property data for the common transparent resins. Where a figure is a working assumption we say so, so you can substitute your supplier’s measured values. Material property claims belong on your inspection sheet, not in a blog post — including ours.
Quick Reference Guide: Transparent VS. Translucent VS. Optical Grade
Three different requirements, three different measurements. Specifying “clear” invites a dispute; specifying transmittance and haze numbers forecloses one.
| Requirement | What you are really asking for | How it is measured | Typical part |
|—|—|—|—|
| Transparent | See through it with minimal distortion | Light transmittance, high | Lens, sight window, cover |
| Translucent / diffusing | Spread the light, hide the source | Haze, high, with transmittance held | LED cover, indicator cap |
| Optical grade | Both numbers plus colour and stress | Transmittance, haze, yellowness index, polariscope | Imaging and sensing optics |
The test method for transmittance and haze on transparent plastics is ASTM D1003. Name it on the drawing, state the sample condition and the instrument geometry, and state whether you measure as-molded or after annealing. A number without a method is an opinion.
Figure 1: Four parts, three different optical specifications. The diffuser on the left is meant to hide; the lens is not.
Which Resins Are Actually Used for Transparent Molding?
Polycarbonate and PMMA carry most of the work. Choice is a trade between impact and scratch resistance, not between “clear” and “less clear”.
Published tables for transparent plastics sometimes list PET, PVC and silicone alongside polycarbonate and acrylic as general injection-molding transparency options. In day-to-day contract molding that list is misleading. Unplasticised PVC is corrosive to tooling and process-unfriendly; PET is a molding specialty rather than a default; silicone is compression or injection-liquid-rubber territory, not a hard clear lens.
| Resin | Where it wins | What it costs you | Watch for |
|—|—|—|—|
| Polycarbonate (PC) | Impact, temperature, toughness | Scratches easily; strictly moisture-sensitive | Drying, internal stress, notch sensitivity |
| PMMA (acrylic) | Clarity, UV and weather, scratch | Brittle; crazes with solvents | Sink in thick zones, crack at bosses |
| COP / COC | Very high clarity, low moisture uptake | Price, limited availability | Gate sizing, cycle sensitivity |
| Clear ABS / SAN | Economical non-optical covers | Yellows with UV | Cosmetic class A is a stretch |
| Nucleated / clarified PP | Dishwasher-safe, chemical resistance | Haze floor above PC and PMMA | Clarifier level and cooling rate |
| Silicone | Flexibility, high temperature, skin contact | Cannot hold a hard optical surface | Flash, contamination, dimensional control |
How to choose in one line: if something can fall on it, PC. If it lives outdoors or gets handled with solvents and cloths, PMMA. If it must pass an optical bench, COP or COC and a budget conversation. Our PC processing guide 그리고 PMMA guide cover the parameter windows; the material decision framework is in material selection.
Why Do Clear Parts Fail More Often Than Any Other Molding Job?
Because a transparent part is a defect magnifier. Everything a black housing hides — a gel, a flow line, a stripe of cold melt, a stress pattern — becomes visible, and the observer is standing two centimetres away with a light behind it.
The failure population is narrow and consistent: moisture, contamination, cold tool, and trapped air. Four causes, and three of them are decided before the first shot is ever attempted.
Moisture. PC and PMMA are hygroscopic enough to pull a damaging amount of water from shop air. Water in a hot melt becomes steam and becomes hydrolysis: silver streaks radiating from the gate, a surface like weak frosted glass, gels that polish into nothing, and a part that fails a drop test it should have passed. This is why a desiccant dryer with a stated dew point is not an optional accessory. Our resin drying guide gives the discipline; on transparent work we treat it as the first specification on the job, not a line item.
Contamination. Reground from another job, dust from a hopper that was never cleaned, release agent migrated from a previous tool. A single contaminant becomes a visible inclusion in a lens. Purging is not optional and mixed material is not “close enough”.
Cold tool and slow fill. Melt that freezes at the flow front leaves a visible transcription of the flow history. The standard answer is a hotter mold — hot water or oil rather than bare water, and on demanding optics a mold temperature controller that holds a face within a couple of degrees.
Trapped air. Burn marks at the end of fill, in a part where everything else is see-through. Vent depth and position are optical decisions on this class of part. Vent depth guide.
Figure 2: Clear, slightly hazy, hazy, frosted. The second one is a defect. The fourth one might be the specification — which is exactly why haze belongs on the drawing.
What Do Gate, Polish and Ejection Decide?
On a transparent part the tool surface and the gate are product features, not tooling details. A clear part replicates the cavity finish with almost no forgiveness.
Polish. The cavity finish transfers 1:1. A SPI-mirror polish is what makes a lens look like a lens; a matte blast finish on the same geometry produces a diffusing part even if you molded it in the clearest resin on earth. If your part must be clear and someone proposes a texture to hide sink, they are telling you they intend to change the optics. Steel grade and polish practice are covered in S136 stainless for polished tooling, and the finishing decision in surface finishing 그리고 which mold finish suits your part.
Gate. A transparent part has a gate witness whether anyone likes it or not, so the job is to decide where the scar goes and what shape it is. Film and tab gates can be placed on a non-critical land and trimmed flush; a concealed gate in a rib or a tunnel gate under a flange moves the defect out of the light path. An undersized or poorly placed gate produces gate blush and a radial flow pattern that is visible forever. The gate design principles are in gate design.
Ejection. A pin mark on a black housing is a dimple. On a clear part it is a lens, and it will show against any background. Sink pins into a land, or move the ejection force to the parting line, and expect that conversation at DFM rather than at T1.
Vents. Vents are open steel, so vent marks replicate onto the part surface. On optics we prefer deeper lands near the parting line and place them where the part later gets a bezel or a gasket.
Figure 3: Gate witness and radial flow on a clear lens. Placed deliberately, this is acceptable. Discovered at T1, it is a tool modification.
What About Internal Stress — Does It Matter If the Part Looks Fine?
Yes, and it is invisible under normal light. Frozen-in orientation and differential cooling leave residual stress that shows up later as crazing with a cleaning agent, dimensional movement, or a failure at a solvent bond.
The reason this matters disproportionately on transparent amorphous resins is that the stress is optically active: view PC or PMMA between crossed polarisers and the stress pattern lights up. That is a real inspection, not a demonstration trick — it tells you where the part will crack when somebody wipes it with the wrong cleaner or screws it down at a boss.
Two controls, in order. Process first: hotter mold, slower fill near the gate, avoid over-packing, and stop chasing a sink by adding holding pressure to an optical part. Annealing second: a controlled soak and slow cool below the heat deflection range relieves much of the residual stress — with the caveats that the part must be supported or it distorts, and PC can take on colour if you are careless with time and temperature.
Annealing is not a rescue for a badly processed part; it is a finishing step for a properly processed one. If a supplier offers annealing as the fix for crazing they should not have created, that is information.
How Do We Take a Clear Part From Drawing to Production?
Six checks, each with a measurable exit condition instead of a photograph in an email.
1. Optical specification first. Transmittance and haze targets per ASTM D1003, colour direction, and which surfaces are optical versus which are merely visible. A lens with two functional faces and one cosmetic face gets three different acceptance rules.
2. Material and drying plan. Grade, drying temperature, drying time, dew point, and the maximum exposure between dryer and hopper. Locked and logged before production.
3. Steel, polish and vent plan. Polish grade per face, gate type and location agreed against the light path, vent lands where they will be hidden.
4. No regrind. Transparent programs run virgin material with the lot recorded. If a sprue has to come back in, it is a written decision with a yield consequence, not a habit — see regrind practice.
5. First article with a polariscope and a section. Stress map, defect map, and the measured optical numbers — not a photo taken next to a window.
6. Production with logged parameters and traceable lots. Our material lot traceability exists so a haze drift can be tied to a batch instead of argued about.
Figure 4: The only inspection that settles a transparency argument. Ask any supplier which instrument, which geometry, which sample condition.
How Do Tolerances, Assembly Stress and Wall Geometry Decide Whether It Stays Clear?
Most clear parts that fail do not fail in the press. They fail six weeks later at an assembly station, where a screwdriver, a rubber gasket or a snap fit puts load into a part that was molded perfectly and left with frozen-in stress.
Clarity and mechanical integrity are usually specified by different people, and the gap between those two specifications is where the returns come from. A transparent part carries two structural handicaps: the resins that are clearest are the ones most sensitive to solvents and stress, and every cosmetic requirement removes material you might otherwise have used for stiffness.
Screw torque is the usual culprit, and it is a design problem
A clear polycarbonate cover driven home with a power bit will craze around the boss — sometimes visibly, sometimes only under a polariscope until the first cleaning agent finds it. Three fixes, in the order they should be tried:
- Control the assembly, not the material. Specify torque, driver speed and the driver geometry on the drawing. A camming-out bit bruises the boss and seeds a crack.
- Give the boss a sink relief and a sane wall ratio. Boss wall at roughly 60% of the adjoining wall, with a relief cored on the back, is what stops a thick hot-spot forming inside a clear section.
- Move the fastener out of the optical zone. Stress birefringence radiates outward from the boss; a few millimetres of separation is often enough to keep it out of the light path.
Get this wrong and the failure is not a molding defect at all, which is why a supplier who only talks about barrel temperature will never find the cause.
Gaskets, snap fits and the creep you can see
A translucent lens clamped by a compressed O-ring carries load permanently, and amorphous transparent resins relieve that load by creeping. Over months the creep appears exactly where you can see it: a dull ring, a shallow surface depression, or a change in light output as the part distorts. Design the seal to sit on a defined land with controlled compression, not on the free optical face.
Tolerance stack: optical position is not dimensional position
A lens sitting 0.2 mm proud of nominal may be dimensionally acceptable and optically useless, because focal shift is amplified at the far end of a light path. Two disciplines follow:
- Specify the optical datum separately from the cosmetic datum. State which face is functional, then hold a tighter tolerance on its position relative to the mounting feature than the housing alone would demand.
- Expect wall variation to move optics. Transparent parts shrink more in thick zones, and the resulting change in lens thickness alters focal length. If optical performance is the point of the part, hold the wall, not just the outline.
| Where it breaks | What it looks like | Fix at the right stage |
|---|---|---|
| Boss under screw torque | Radiating crazes from the boss root | Torque specification, boss relief, 60% wall ratio |
| Clamped seal | Dull ring or shallow depression after months | Defined seal land, limited compression |
| Snap fit | Whitening at the root radius | Larger root radius, shallower engagement |
| Optical datum | Light output drifts part to part | Separate optical tolerance chain, hold wall |
None of this is exotic, and almost none of it belongs to the molding machine — it belongs to the drawing review. That is the conversation we push for before a tool is cut. Our sample approval process exists so optical and mechanical acceptance criteria are agreed against measured parts rather than discovered at the assembly line, and the T1 stage is where the stress map and the dimensions get settled together.
When a Transparent Plastic Part Is the Wrong Answer
Sometimes the honest answer is glass, a coating, or a different design.
It will be cleaned with unknown chemicals. PC and PMMA both craze under the wrong solvent. If you cannot control the wiping agent, the risk belongs to the material selection conversation.
Scratch resistance is the actual requirement. No clear thermoplastic matches glass. A hard coat helps and adds cost and an adhesion risk; if a key lives in the same pocket as your lens, design for it.
The section is thick and cosmetic. Sink in a thick clear wall is unavoidable at some level. Thin the wall, core it, or accept a visual feature.
You want a texture and clarity in the same place. Pick one.
And our own honest limits: ISO 9001:2015, RoHS, REACH. We are not IATF 16949 certified and we do not claim implant-grade medical. For optics we bring measurement and traceability, not certifications we don’t have.
Related Reading From Ideal Pro
- Which injection mold finish is right for your part — deciding polish against texture when the surface is functional.
- S136 stainless tool steel — the corrosion-and-polish choice for optical cavities.
- Regrind in injection molding — why recycled material is a hard limit on optical work.
- Quality assurance — how measured acceptance and lot traceability are run here.
- Injection molding quality agreement — putting defect classes and sampling plans in writing before production.
요약
Transparent molding is a discipline rather than a material. Put a number on the requirement — transmittance and haze per ASTM D1003 — before you choose the resin; dry the material as though it were the primary process parameter, because for PC and PMMA it is; treat the cavity polish, gate and ejector pins as product features that will be transmitted directly into the part; run virgin material on optical work; and inspect with a haze meter and a polariscope rather than daylight and optimism. Our complete guide to flawless finishes on transparent parts covers the finishing and defect-removal side in more depth. Do that and clear parts become predictable. Skip any one of those and you will hear “transparent is hard” from whoever is holding the tool.
Send us the part, the light path, and the cleaning agent it will meet in service. You will get a materials and process recommendation with the drying and polish plan stated, and a first-article inspection method you can audit.
+86 136 5621 3638 ✉ [email protected] ✑ Request a quote · 문의하기
Sources
- ASTM D1003 — standard test method for haze and luminous transmittance of transparent plastics (method to be named on your drawing).
- Ideal Pro molding and inspection records — clear and diffusing parts, 2023-2026, Huzhou facility.
- Ideal Pro tool-room practice — cavity polish grades, S136 tooling, vent and gate placement on optical faces.
- Ideal Pro internal material database — resin behaviour on hydrolysis, crazing and annealing response.
What is the difference between transparent and translucent?
Transparent means light passes with little scattering, so you can see through it. Translucent means light passes but is scattered, so you cannot see through it. They are measured separately: transmittance for the first, haze for the second. A lens wants high transmittance and low haze; a diffuser wants high transmittance and high haze, which is why “clear” is not a specification.
Why do my clear parts have silver streaks from the gate?
In the large majority of cases, moisture. Wet polycarbonate or PMMA flashes to steam at the nozzle and throws splay from the gate. The fix is drying discipline — correct temperature, correct time, desiccant dew point, and a limit on how long material may sit in the hopper — not a higher injection speed, which usually makes the pattern worse.
Can I use regrind on a transparent part?
Not on optical work. Each thermal pass increases gel count and shifts colour, so the resin saving is repaid in yield and in a haze number that drifts batch to batch. If a sprue must go back in, make it a written decision with a percentage cap and a measured acceptance limit, not a habit.
Does annealing fix a clear part that is crazing?
Annealing relieves much of the frozen-in stress that makes a part vulnerable, but it is a finishing step for a properly processed part, not a rescue for an over-packed one. It also carries its own risks: unsupported parts distort, and polycarbonate can discolour if held too long or too hot. Fix the process first, then anneal.
Which is clearer, PC or PMMA?
Both are used for transparent work and both transmit well; PMMA is the more weather- and scratch-tolerant of the two and is often the choice outdoors, while PC is chosen when the part must survive impact. Choose by failure mode rather than by datasheet clarity, and require the measured numbers for the exact grade you are buying.
How should I specify clarity on a drawing?
Name the method and the numbers: transmittance and haze per ASTM D1003, the instrument geometry, the sample condition, and which faces are optical. Add colour direction, and state whether the part is measured as-molded or after annealing. Two words — “must be clear” — guarantee a disagreement with your supplier.
Does Ideal Pro mold transparent parts?
Yes, for lenses, windows, diffusers and cosmetic covers, with polish and gate planning at DFM and inspection by measured haze and transmittance rather than appearance alone. Send the part, the light path, and what cleans it in service — the last question is the one most quotations skip.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.


 English
 French
 Dutch
 German
 Japanese
 Korean