 한국어



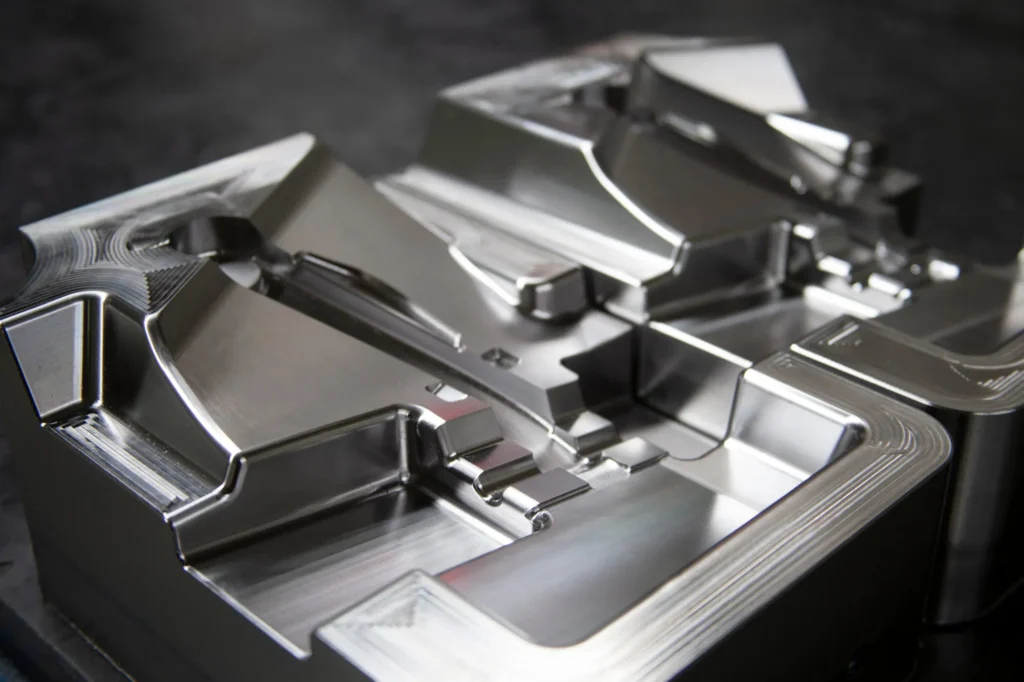
What is injection mold surface treatment?
Here, injection mold surface treatment refers to the texture of the product surface. As we all know, injection molded products are made by injecting molten plastic material into a mold to form a specific shape, and then cooling and solidifying it into the final product. The surface texture is generated directly by the mold itself, meaning that no additional post-processing work such as polishing, painting, or oxidation is required. Therefore, the surface texture of injection molded products corresponds to the processing of the mold surface, specifically the polishing and finishing of the mold during the production process. With this understanding, we can now look at some common surface treatment methods we use.
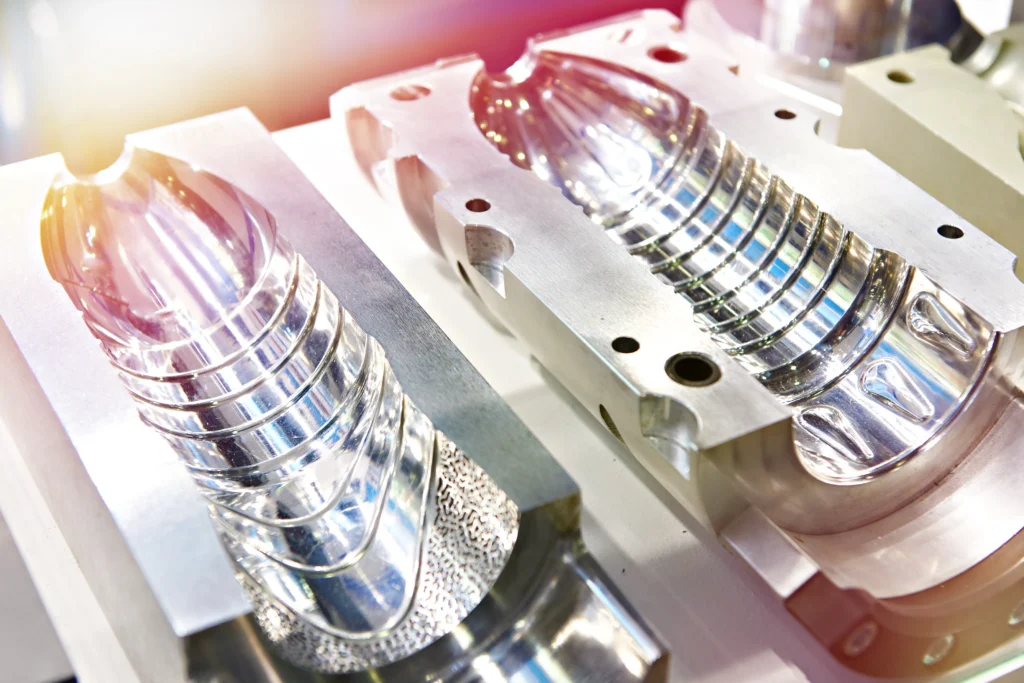
SPI mold surface treatment
The most commonly used surface finishes are standardized by the Plastics Industries Society (SPI). These finishes range from the highest grade, mirror finish (SPI A), to semi-gloss finishes (SPI B), and fine and coarse matte textures (SPI C and SPI D). These finishes enhance the appearance of transparent polymer parts by improving their reflectivity or transparency. Mirror finishes are ideal for parts that require a glossy or transparent look, but they are also more prone to showing signs of use and typically require longer processing times and are more expensive. Matte finishes, on the other hand, offer a softer look and help conceal fingerprints or scratches on frequently handled items. They are also faster to process and more cost-effective.
| Finishing type | SPI Number | describe | application | roughness (Ra μm) | ||
| SPI-A1 | #3 Diamond Polishing | Highly polished or transparent parts, optically clear | 0.012-0.025 | |||
| diamond | SPI-A2 | #6 Diamond Polishing | Highly polished or transparent parts | 0.025 – 0.050 | ||
| SPI-A3 | #15 Diamond Polishing | High to medium polished parts, non-optical lenses | 0.050-0.100 | |||
| SPI-B1 | 600 particle size | Medium polished parts | 0.05 – 0.10 | |||
| Paper | SPI-B2 | 400 particle size | Medium polished parts | 0.10 – 0.15 | ||
| SPI-B3 | 320 gravel | Medium to low polished parts | 0.28 – 0.32 | |||
| SPI-C1 | 600 stones | Low-polish parts | 0.35 – 0.40 | |||
| Stone | SPI-C2 | 400 stones | Low-polish parts | 0.35 – 0.40 | ||
| SPI-C3 | 320 stones | Low-polish parts |
| |||
| SPI-D1 | #11 Glass Beads | Satin finish | 0.80 – 1.00 | |||
| Dry sandblasting | SPI-D2 | #240 Alumina Sandblasting | Dull finish | 1.00 – 2.80 | ||
| SPI-D3 | #24 Alumina Sandblasting | Dull finish | March 20——6:00 PM |
VDI 3400 mold texture
VDI 3400 surface finish refers to the texture standard of the German Association of Engineers (Verein Deutscher Ingenieure). VDI has set the standard for mold cavity surfaces in the European market and globally. VDI 3400 is mainly processed by EDM during mold making. VDI consists of electrical discharge particles of different sizes, depths, and densities.
| VDI Value | describe | application | Roughness (Ra µm) |
| VDI 12 | 600 stones | Low-polish parts | 0.40 |
| VDI 15 | 400 stones | Low-polish parts | 0.56 |
| VDI 18 | Dry spray glass beads | Satin finish | 0.80 |
| VDI 21 | Dry blasting #240 oxide | Dull finish | 1.12 |
| VDI 24 | Dry blasting #240 oxide | Dull finish | 1.60 |
| VDI 27 | Dry blasting #240 oxide | Dull finish | 2.24 |
| VDI 30 | Dry blasting #24 Oxide | Dull finish | 3.15 |
| VDI 33 | Dry blasting #24 Oxide | Dull finish | 4.50 |
| VDI 36 | Dry blasting #24 Oxide | Dull finish | 6.30 |
| VDI 39 | Dry blasting #24 Oxide | Dull finish | 9.00 |
| VDI 42 | Dry blasting #24 Oxide | Dull finish | 12.50 |
| VDI 45 | Dry blasting #24 Oxide | Dull finish | 18.00 |
The VDI 3400 surface finish standard is primarily achieved through electrical discharge machining (EDM) and is an international guideline for creating matte textures on molds. EDM can produce a range of textures from fine to coarse, depending on the selection. Some textures have close equivalents, such as SPI D-3 and VDI 33, which look very similar. Similarly, VDI 12 corresponds to SPI C-1 in terms of texture quality.
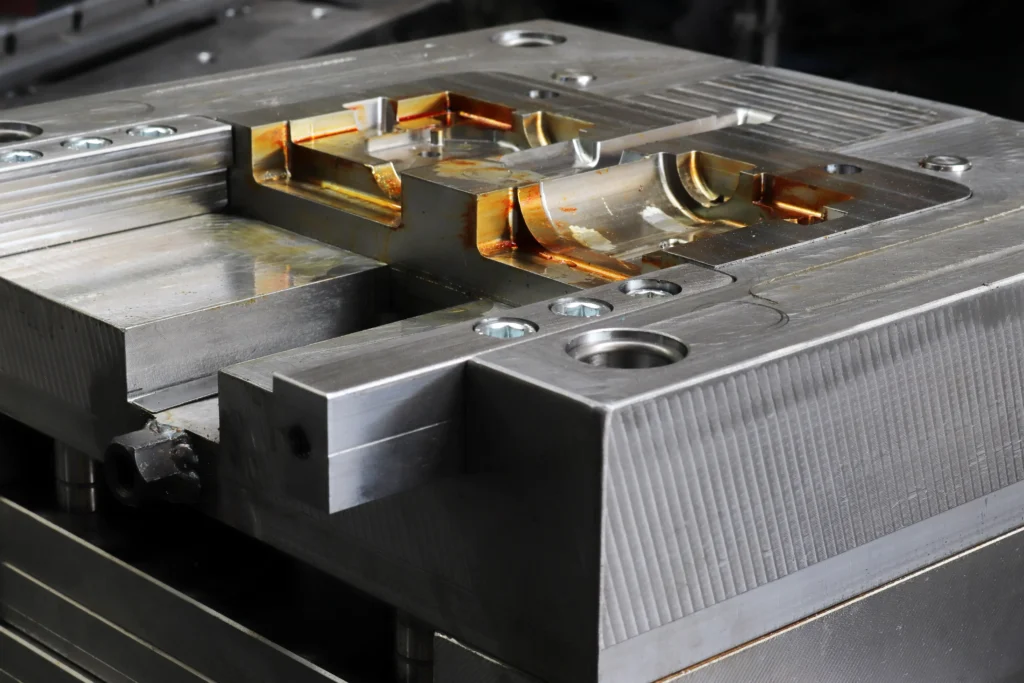
Injection molding surface treatment options
A lower surface finish value results in a finer mold and product surface, which means longer mold production time and higher costs. Therefore, it’s not always necessary to choose the highest grade when selecting mold surface finish. The decision should be made based on the product’s usage environment and specific requirements. For example, for externally invisible plastic parts, a surface finish of SPI-B2 (the industry default unless otherwise specified) or lower is sufficient. For products requiring a transparent or mirror-like finish, a standard of SPI-A3 or higher is necessary.
Finally, the surface treatment of the mold is significantly influenced by the mold manufacturing method, especially the draft angle of the product. In injection molding, almost every product requires a draft angle (which helps remove the product from the mold), typically ranging from 1 to 10 degrees. The rougher the product surface, the larger the required draft angle. Therefore, if you need a product with a surface almost perpendicular to the mold opening direction, you cannot choose a very rough surface treatment. If you are unsure about the right mold treatment for your product, feel free to consult Ideal Pro’s professional engineers and advisors. We are happy to offer you free consultation and assistance; let’s get started!
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean