 日本語



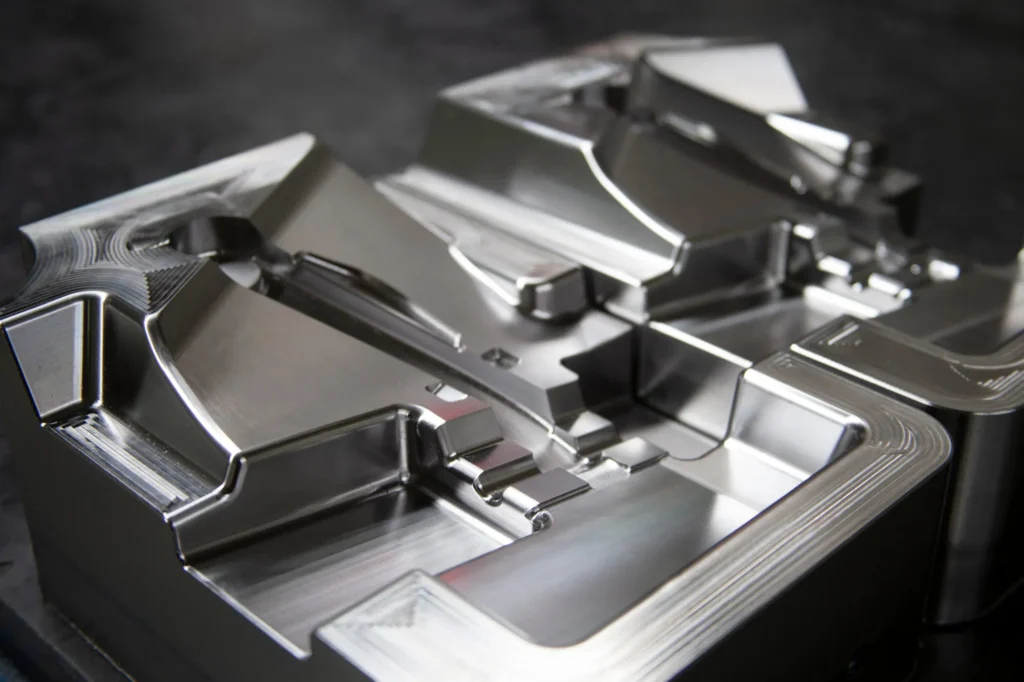
射出成形金型の表面処理とは何ですか?
Here, injection mold surface treatment refers to the texture of the product surface. As we all know, injection molded products are made by injecting molten plastic material into a mold to form a specific shape, and then cooling and solidifying it into the final product. The surface texture is generated directly by the mold itself, meaning that no additional post-processing work such as polishing, painting, or oxidation is required. Therefore, the surface texture of injection molded products corresponds to the processing of the mold surface, specifically the polishing and finishing of the mold during the production process. With this understanding, we can now look at some common surface treatment methods we use.
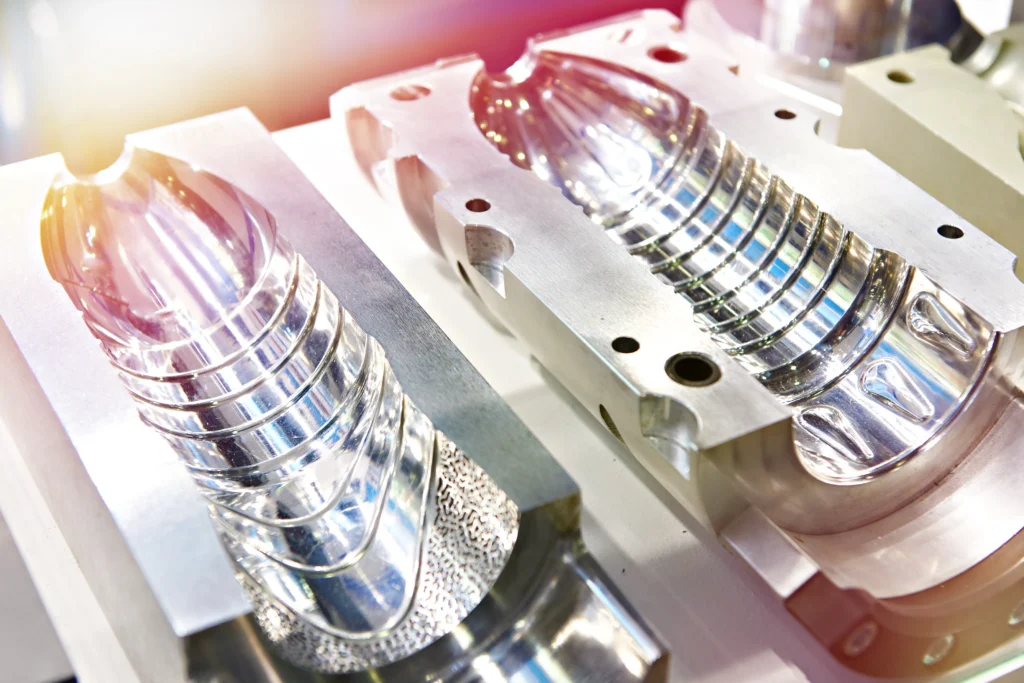
SPI金型表面処理
The most commonly used surface finishes are standardized by the Plastics Industries Society (SPI). These finishes range from the highest grade, mirror finish (SPI A), to semi-gloss finishes (SPI B), and fine and coarse matte textures (SPI C and SPI D). These finishes enhance the appearance of transparent polymer parts by improving their reflectivity or transparency. Mirror finishes are ideal for parts that require a glossy or transparent look, but they are also more prone to showing signs of use and typically require longer processing times and are more expensive. Matte finishes, on the other hand, offer a softer look and help conceal fingerprints or scratches on frequently handled items. They are also faster to process and more cost-effective.
| 仕上げタイプ | SPI番号 | 説明する | application | 粗さ (Ra μm) | ||
| SPI-A1 | #3 Diamond Polishing | 高度に研磨された部品または透明な部品、光学的に透明 | 0.012-0.025 | |||
| ダイヤモンド | SPI-A2 | #6 Diamond Polishing | 高度に研磨された部品または透明な部品 | 0.025 – 0.050 | ||
| SPI-A3 | #15 Diamond Polishing | 高度から中程度の研磨が施された部品、非光学レンズ | 0.050-0.100 | |||
| SPI-B1 | 粒子サイズ600 | 中程度の研磨が施された部品 | 0.05 – 0.10 | |||
| 紙 | SPI-B2 | 粒子サイズ400 | 中程度の研磨が施された部品 | 0.10 – 0.15 | ||
| SPI-B3 | 320砂利 | 中程度から低程度の研磨が施された部品 | 0.28 – 0.32 | |||
| SPI-C1 | 600個の石 | 低光沢部品 | 0.35 – 0.40 | |||
| 石 | SPI-C2 | 400個の石 | 低光沢部品 | 0.35 – 0.40 | ||
| SPI-C3 | 320個の石 | 低光沢部品 |
| |||
| SPI-D1 | #11 Glass Beads | サテン仕上げ | 0.80 – 1.00 | |||
| 乾式サンドブラスト | SPI-D2 | #240 Alumina Sandblasting | つや消し仕上げ | 1.00 – 2.80 | ||
| SPI-D3 | #24 Alumina Sandblasting | つや消し仕上げ | March 20——6:00 PM |
VDI 3400 金型テクスチャ
VDI 3400 surface finish refers to the texture standard of the German Association of Engineers (Verein Deutscher Ingenieure). VDI has set the standard for mold cavity surfaces in the European market and globally. VDI 3400 is mainly processed by EDM during mold making. VDI consists of electrical discharge particles of different sizes, depths, and densities.
| VDIの価値 | 説明する | application | 表面粗さ(Ra µm) |
| VDI 12 | 600個の石 | 低光沢部品 | 0.40 |
| VDI 15 | 400個の石 | 低光沢部品 | 0.56 |
| VDI 18 | ドライスプレーガラスビーズ | サテン仕上げ | 0.80 |
| VDI 21 | ドライブラスト処理 #240酸化物 | つや消し仕上げ | 1.12 |
| VDI 24 | ドライブラスト処理 #240酸化物 | つや消し仕上げ | 1.60 |
| VDI 27 | ドライブラスト処理 #240酸化物 | つや消し仕上げ | 2.24 |
| VDI 30 | ドライブラスト #24酸化物 | つや消し仕上げ | 3.15 |
| VDI 33 | ドライブラスト #24酸化物 | つや消し仕上げ | 4.50 |
| VDI 36 | ドライブラスト #24酸化物 | つや消し仕上げ | 6.30 |
| VDI 39 | ドライブラスト #24酸化物 | つや消し仕上げ | 9.00 |
| VDI 42 | ドライブラスト #24酸化物 | つや消し仕上げ | 12.50 |
| VDI 45 | ドライブラスト #24酸化物 | つや消し仕上げ | 18.00 |
The VDI 3400 surface finish standard is primarily achieved through electrical discharge machining (EDM) and is an international guideline for creating matte textures on molds. EDM can produce a range of textures from fine to coarse, depending on the selection. Some textures have close equivalents, such as SPI D-3 and VDI 33, which look very similar. Similarly, VDI 12 corresponds to SPI C-1 in terms of texture quality.
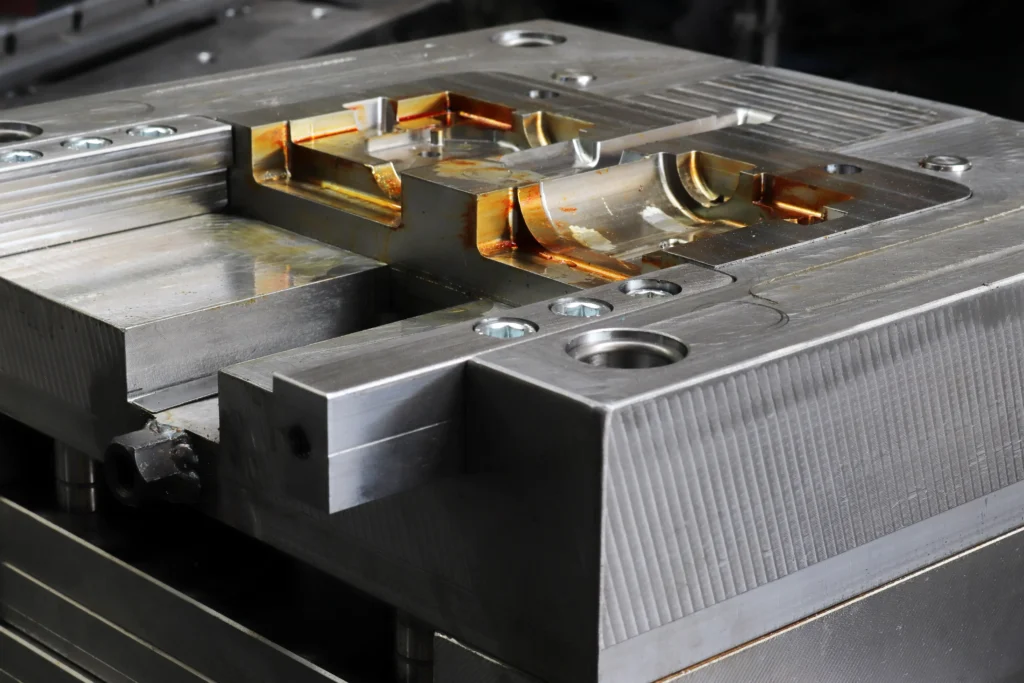
射出成形表面処理オプション
A lower surface finish value results in a finer mold and product surface, which means longer mold production time and higher costs. Therefore, it’s not always necessary to choose the highest grade when selecting mold surface finish. The decision should be made based on the product’s usage environment and specific requirements. For example, for externally invisible plastic parts, a surface finish of SPI-B2 (the industry default unless otherwise specified) or lower is sufficient. For products requiring a transparent or mirror-like finish, a standard of SPI-A3 or higher is necessary.
Finally, the surface treatment of the mold is significantly influenced by the mold manufacturing method, especially the draft angle of the product. In injection molding, almost every product requires a draft angle (which helps remove the product from the mold), typically ranging from 1 to 10 degrees. The rougher the product surface, the larger the required draft angle. Therefore, if you need a product with a surface almost perpendicular to the mold opening direction, you cannot choose a very rough surface treatment. If you are unsure about the right mold treatment for your product, feel free to consult Ideal Pro’s professional engineers and advisors. We are happy to offer you free consultation and assistance; let’s get started!
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean