 한국어



In the injection molding process, the mold cavity is initially filled with air before the plastic melt enters. Additionally, the plastic melt itself generates a significant amount of gas during injection.
During mold filling, all these gases must be expelled from the cavity. The primary pathways for gas escape generally include:
- Gaps between mold inserts and ejector pins.
- The parting line of the mold.
- Dedicated vents and exhaust grooves.
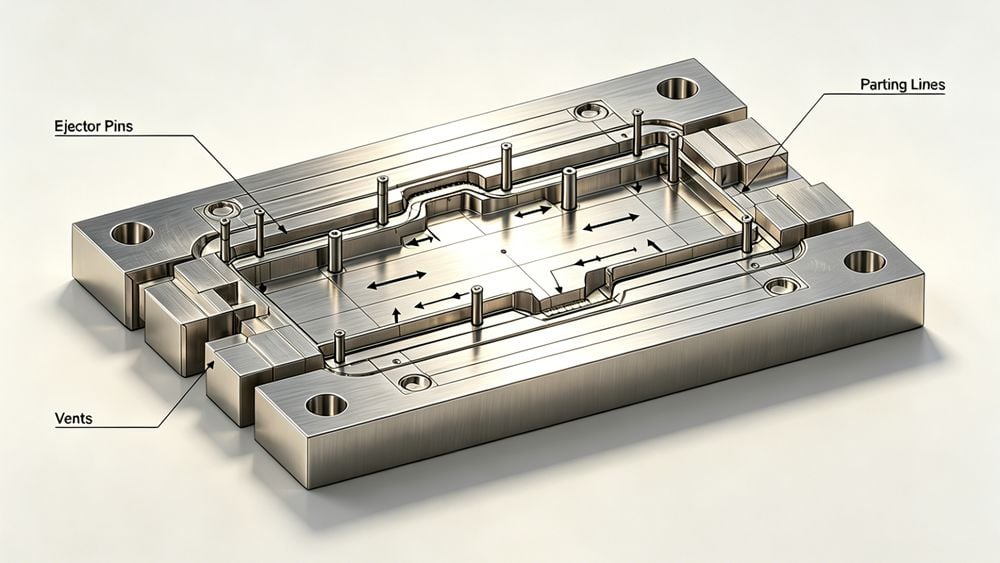
The Consequences of Poor Venting
When venting is inadequate, the gas within the cavity becomes compressed as the plastic melt is continuously injected. The greater the degree of compression, the stronger the resistance against the advancing melt.
Simultaneously, the plastic melt loses energy during flow, causing its temperature to drop and its fluidity to decrease. Faced with the obstruction of compressed gas, the consequences typically manifest in two ways:
- Short Shots or Burning: The melt fails to overcome the resistance of the compressed gas, forcing it to stop advancing. This results in short shots (incomplete filling) or burnt marks on the part.
- Mold Expansion: The melt eventually breaks through the air barrier, but the excessive pressure required to do so—particularly in molds with multi-point gates—causes the mold to expand or flash.
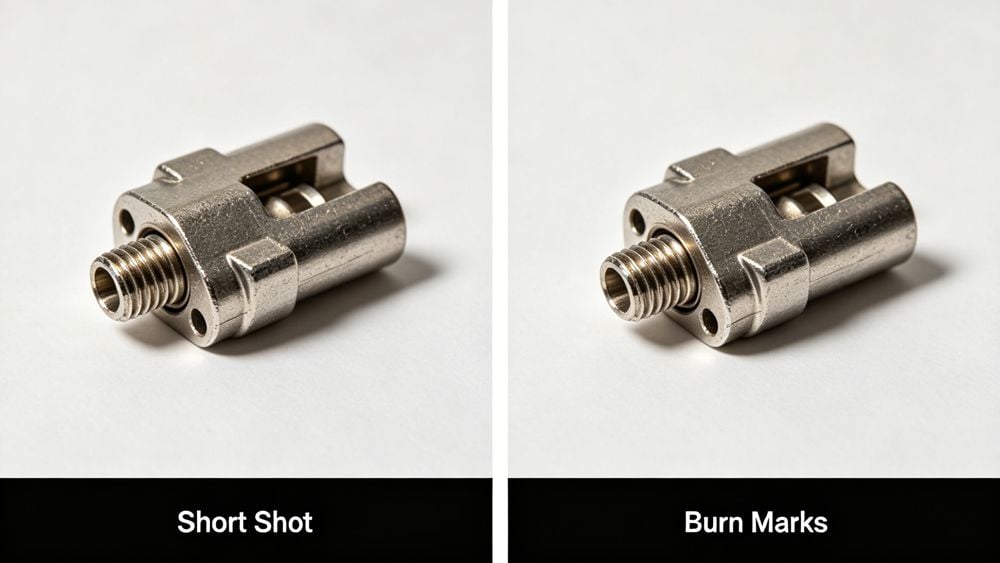
Long-Term Mold Deformation
Molds, especially those with multi-point gating systems, are susceptible to deformation after prolonged use. The center area of the gate is directly subjected to the injection pressure from the machine's screw. Consequently, this area has the highest probability of expansion, which ultimately becomes a major factor leading to product rejection.
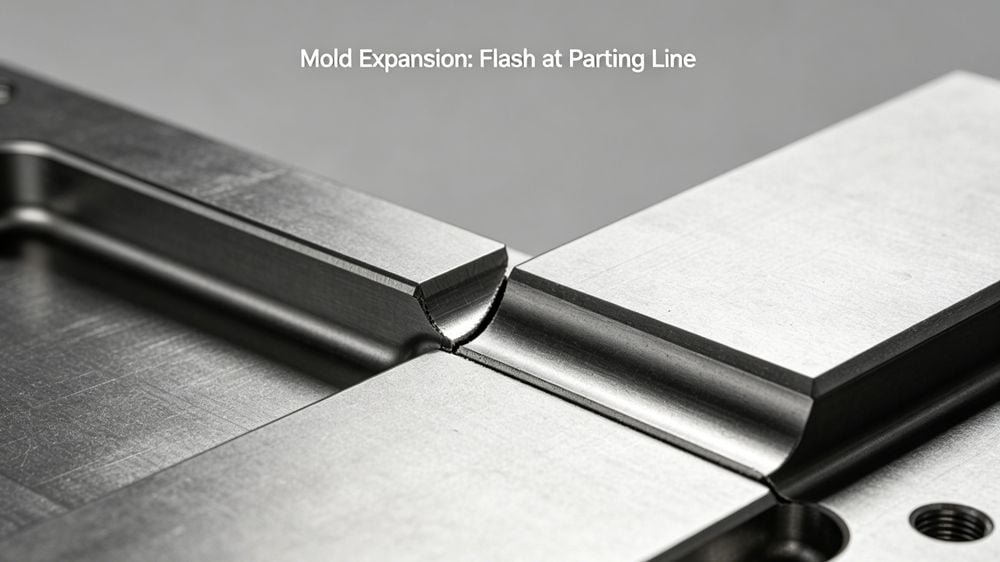
Comparison of Venting Issues
| Issue | Primary Cause | Resulting Defect |
|---|---|---|
| Air Trapping | Inadequate vents or blocked exhaust paths | Short shots, burn marks, or voids |
| Mold Expansion | Excessive injection pressure overcoming gas resistance | Flash, dimensional inaccuracy, parting line mismatch |
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean