 한국어



Thermoplastic Elastomers (TPE) have revolutionized modern manufacturing, bridging the gap between the flexibility of traditional rubber and the high-speed processing of plastics. However, working with TPE requires a nuanced understanding of its unique properties.
~에서 IDEAL PRO, we’ve spent over 18 years delivering turnkey manufacturing solutions and guiding clients through nearly 3,000 diverse product developments. Through this experience, we’ve learned that TPE success relies on more than just selecting the right resin—it demands precision engineering from design to mass production.
In this comprehensive guide, we break down everything you need to know about TPE injection molding, from material selection and DFM guidelines to troubleshooting common defects.
What is TPE Injection Molding?
TPEs are a class of copolymers consisting of both hard thermoplastic segments and soft elastomeric segments. This dual-phase structure gives TPE its unique ability to stretch like rubber while being melted and molded like plastic.
TPE vs. Thermoset Rubber & Silicone
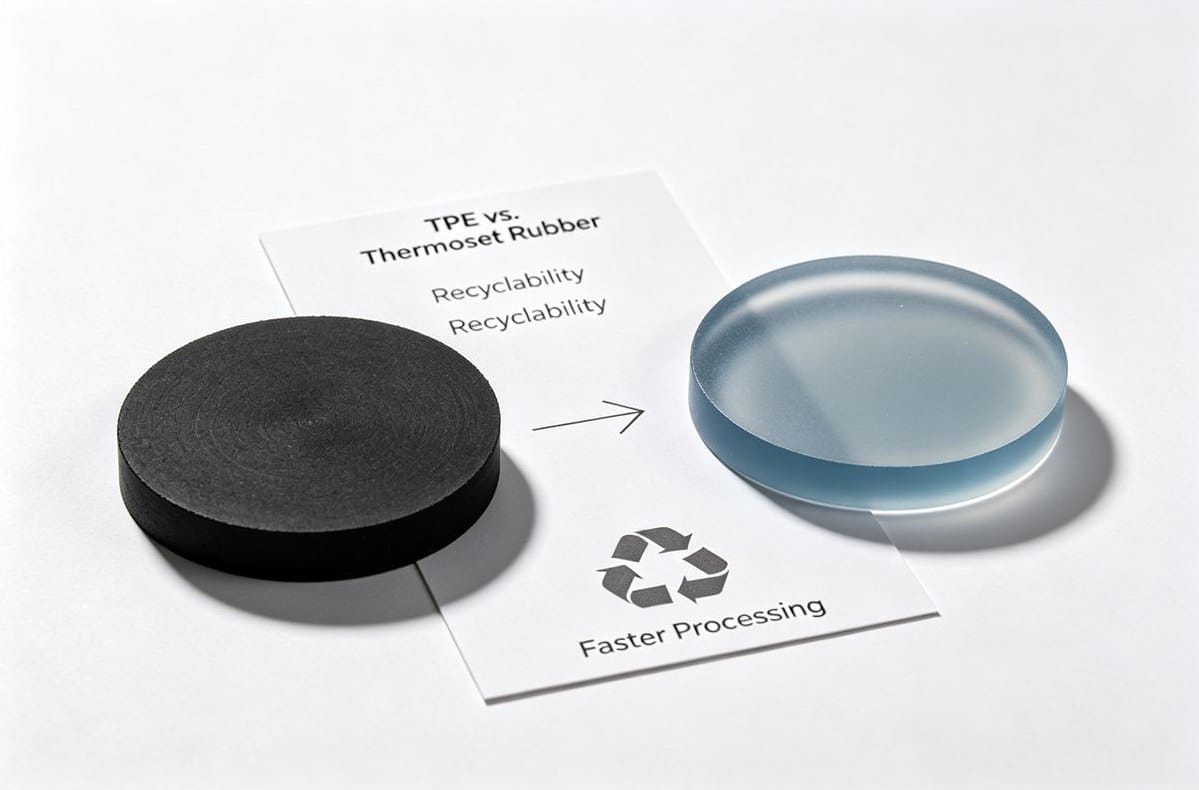
Unlike thermoset rubbers that undergo irreversible chemical cross-linking (vulcanization), TPEs are non-crosslinked. This fundamental difference offers massive advantages for global buyers:
- Faster Cycle Times: No curing time means significantly faster production.
- 100% Recyclability: Sprues, runners, and rejected parts can be reground and reused.
- Design Flexibility: Ideal for complex overmolding and multi-shot molding.
Choosing the Right TPE Material: Properties & Applications
Selecting the correct TPE family is critical for balancing performance, aesthetics, and cost. Here is a quick-reference matrix for the most common grades:
| TPE Family | Key Characteristics | Ideal Applications |
|---|---|---|
| SBC (Styrenics) | Soft-touch, excellent clarity, low cost | Consumer grips, toys, soft gaskets |
| TPU (Urethanes) | High abrasion resistance, toughness, clear | Phone cases, footwear, industrial wheels |
| TPV & TPO (Olefins) | Weather/UV resistant, low density, durable | Automotive seals, bumpers, outdoor trims |
| COPE & PEBA | High-temp resistance, superior fatigue life | Medical tubing, sports equipment, auto boots |
Advanced TPE
사출 성형 Process Parameters
Processing TPE requires precise control, as these materials are highly sensitive to temperature and shear.
Moisture Management
Hygroscopic TPEs like TPU, COPE, and PEBA must be dried before processing to prevent splay, bubbles, and degraded mechanical properties. Typical drying parameters are 80°C–100°C for 2–4 hours, targeting a moisture content below 0.05%.
Precision Temperature & Pressure Control
- Barrel & Melt Temp: Generally ranges from 170°C to 230°C. Overheating can cause thermal degradation, while underheating leads to short shots. To learn more about resin thermal damage, read our guide: Why Does Plastic Degrade in Injection Molding?
- Mold Temp: Maintained between 30°C and 70°C to ensure even cooling and minimize warpage.
- Injection Speed: Multi-stage profiling is essential. A slower initial speed allows air to escape, followed by high speed to fill the cavity before the material cools.
Overmolding Compatibility
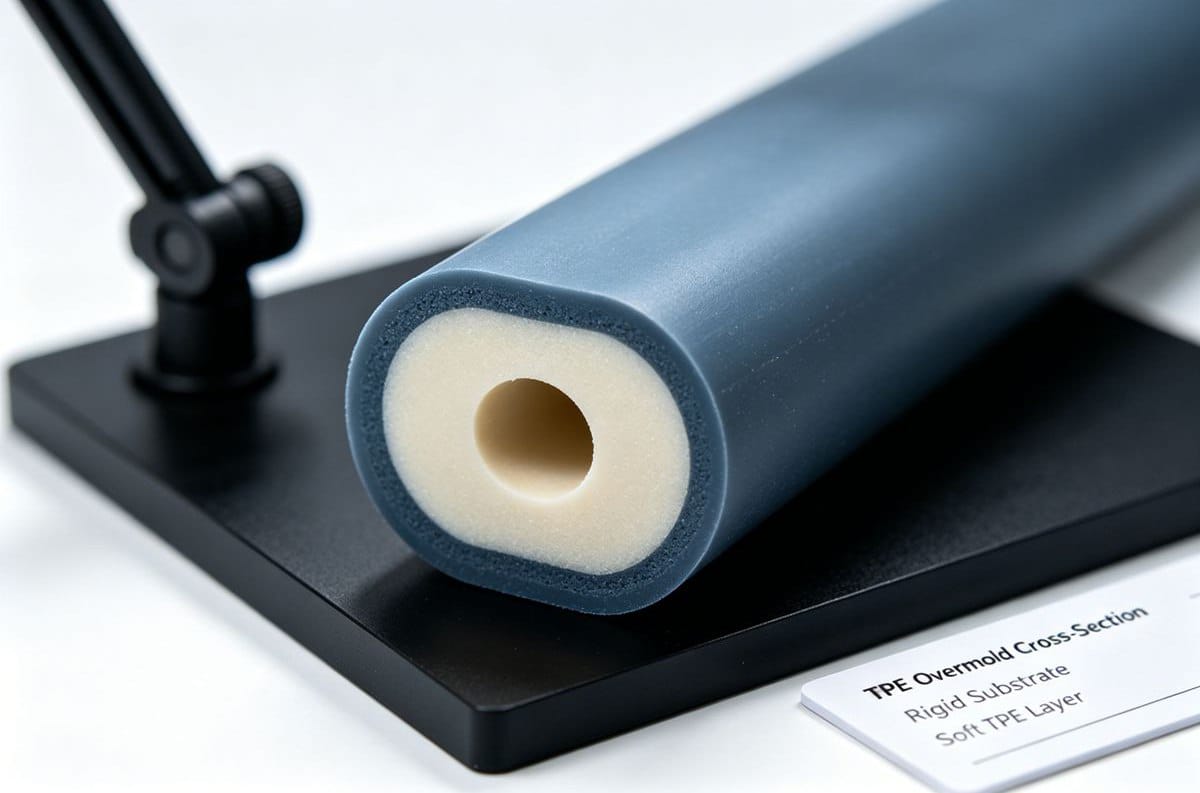
TPE is widely used for "soft-over-hard" applications. Ensuring a strong chemical or mechanical bond between the TPE and the rigid substrate (PP, ABS, PC, Nylon) requires matching material families and optimizing the melt temperature during the second shot. If you plan two-shot TPE products, check our dedicated design guide: TPE 투샷 사출 성형 제품의 설계 고려 사항
Critical DFM Guidelines for TPE Mold Design
Designing molds for TPE differs significantly from rigid plastics. At IDEAL PRO, our technical teams always optimize DFM before cutting steel to prevent costly rework.
- Wall Thickness: Maintain uniform walls between 1.0mm and 3.0mm. Thick sections cool slower and are prone to sink marks and voids.
- 드래프트 분석: Because TPE is flexible and can grip the mold, a minimum draft angle of 1° to 2° is required. Softer, high-friction grades may require 3° or more.
- Ejection Systems: Avoid small ejector pins that can puncture or tear soft materials. Use ejector plates or large-diameter pins acting on stiff sections.
- 하소연: TPE traps air easily. Shallow vent grooves (0.01–0.02 mm) at the end of flow paths are necessary to prevent burn marks and short shots.
Troubleshooting Common TPE Molding Defects
Even with perfect DFM, process tuning is often required. Here are proven solutions for frequent issues:
| Common Defect | Primary Cause | Engineering Solution |
|---|---|---|
| Flash / Burrs | Excessive injection pressure or poor mold clamping | Reduce injection pressure; verify clamp tonnage and mold sealing surfaces. |
| 싱크 자국 | Uneven cooling in thick wall sections | Core out thick areas; optimize packing pressure and cooling time. |
| Poor Adhesion | Incompatible substrate or low melt temp | Verify material compatibility; increase TPE melt temp to improve bonding. |
| Splay / Bubbles | Moisture in resin or thermal degradation | Dry material properly; reduce barrel temperature and residence time. |
Global Industry Applications
TPE’s versatility makes it indispensable across multiple sectors:
- Consumer Electronics: Ergonomic grips, waterproof seals, and shock-absorbing protective housings.
- 자동차: Under-hood seals, interior dash trims, and EV battery gaskets.
- 의료기기: FDA-compliant wearable bands, flexible tubing, and ergonomic surgical instrument grips.
- Industrial & Sporting Goods: Waterproof grommets, vibration dampeners, high-flex fatigue-resistant components.
Sustainability & Total Cost of Ownership
For procurement and sustainability officers, TPE offers undeniable financial and environmental benefits. The elimination of vulcanization drastically reduces energy consumption and cycle times. Furthermore, the closed-loop recycling of TPE scrap minimizes material waste, significantly lowering the Total Cost of Ownership compared to silicone or liquid rubber mass production.
Final Checklist: Selecting the Right TPE Grade
Don't just select a TPE grade—engineer your entire process around it. When starting your next project, evaluate your required Shore hardness, chemical exposure, temperature limits, and overmolding substrate.
Ready to bring your TPE product to life? ~에서 IDEAL PRO, our end-to-end turnkey solutions cover everything from rapid prototyping to full-scale production. Whether you need DFM optimization or high-volume manufacturing, our expert team is ready to ensure your success.
자주 묻는 질문
Can TPE be used for double-shot overmolding?
Which TPE grade works best for outdoor UV exposure?
Is TPE medical grade FDA & EU REACH compliant?
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean