 한국어




Why Cooling System Design Is Critical in Injection Molding
In 사출 성형[^1] , an optimally designed mold cooling system is non-negotiable. Plastic parts must solidify to sufficient rigidity before ejection—otherwise, residual stress or external forces cause warpage, sink marks, or dimensional inaccuracies.
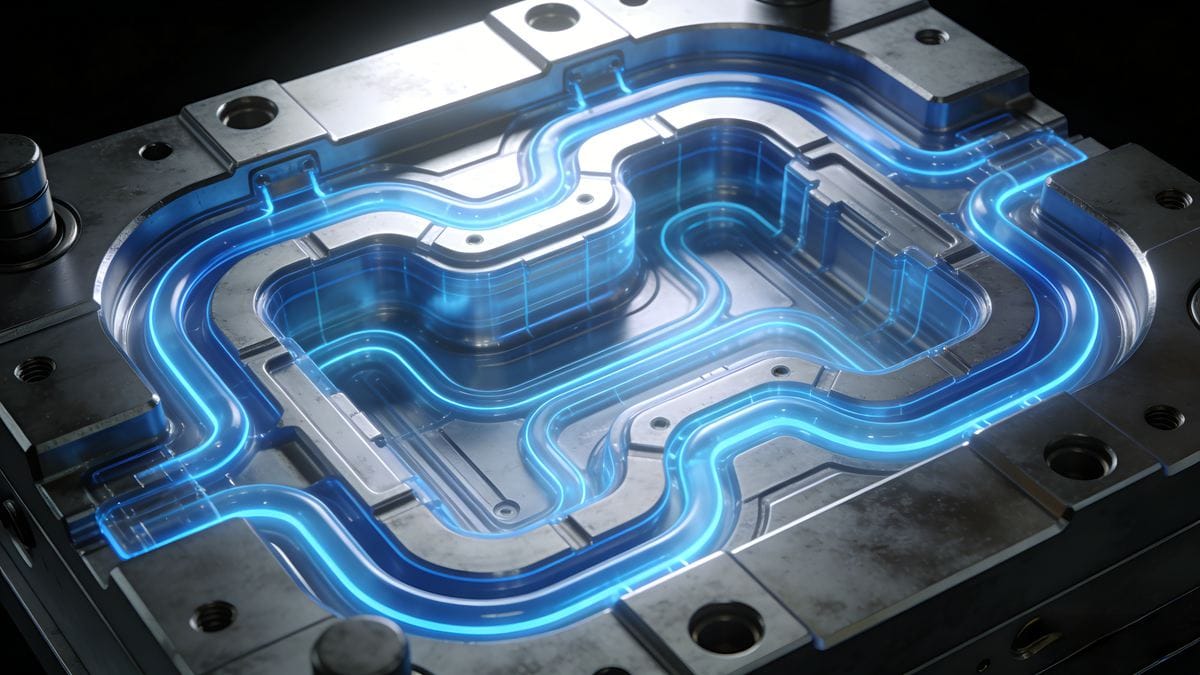
무엇보다 중요한 점은, cooling time consumes 70–80% of the total molding cycle. A precision-engineered cooling system slashes cycle times, boosts throughput, reduces energy costs, and enhances part quality. Conversely, poor cooling design leads to:
- Extended production cycles
- Higher operational costs
- Non-uniform shrinkage and part deformation
Heat Dissipation Mechanics: Data-Driven Insight
Experimental studies confirm:
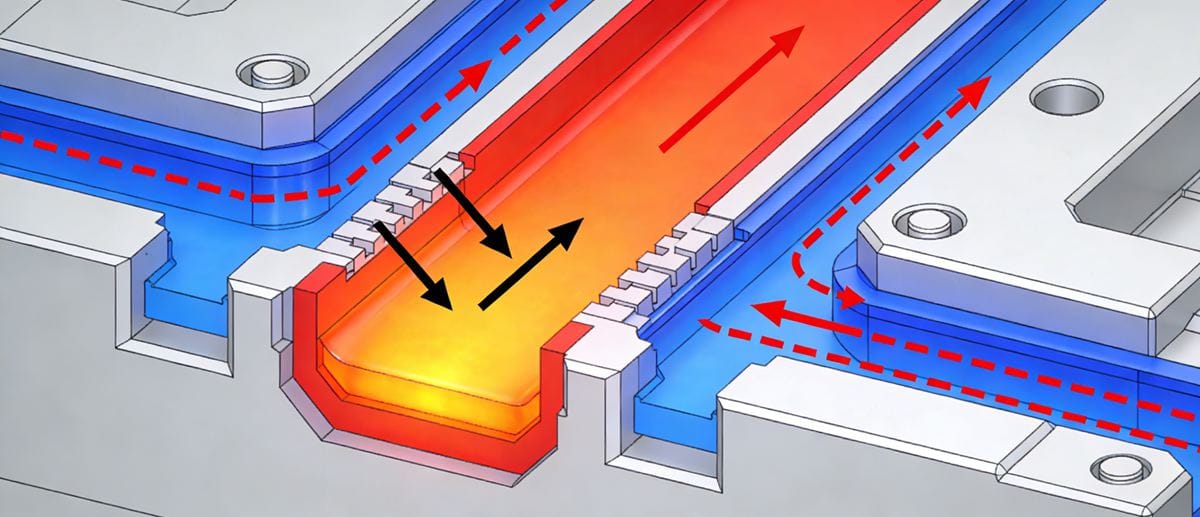
- ? 95% of heat transfers from molten plastic → mold steel → cooling channels (via conduction & convection)
- ? 5% dissipates into ambient air through radiation/convection
Coolant (typically water or glycol mix) absorbs heat via turbulent flow[^2]. Residual heat gradually dissipates through the mold structure post-cycle.
Cooling Time’s Role in the Molding Cycle
The full injection molding cycle comprises:
- Mold closing
- Injection/filling
- Packing/holding
- Cooling (70–80% of total time)
- Ejection
Parts must cool below their Heat Deflection Temperature (HDT)[^3] before ejection to prevent:
- Warpage from residual stress relaxation
- Deformation from ejector pin pressure
7 Key Factors Influencing Cooling Rate
| Factor | Impact on Cooling Efficiency |
|---|---|
| Part Wall Thickness | Cooling time ∝ (thickness)². Doubling thickness = 4× longer cooling |
| Mold Material Conductivity | High-conductivity steels (e.g., beryllium copper inserts) accelerate heat extraction |
| Cooling Channel Layout | Channels closer to cavity, larger diameter, higher density = superior thermal control |
| Coolant Flow Rate | Turbulent flow (Re > 4,000) maximizes convective heat transfer |
| Coolant Properties | Low viscosity + high thermal conductivity + lower temp = optimal performance |
| Plastic Material | High thermal conductivity (e.g., filled nylons) or low specific heat = faster cooling |
| Processing Parameters | Higher melt/mold temps or lower ejection temp = extended cooling requirement |
[Image: Comparison graphic – uniform vs. non-uniform cooling channel layout[^4]s with thermal simulation overlay. Alt text: "Cooling channel design impact: uniform layout prevents warpage in thick-walled plastic components"]
Essential Cooling System Design Rules (SEO-Optimized Checklist)
✅ Uniformity First: Position channels symmetrically relative to cavity surfaces to prevent thermal gradients.
✅ Proximity Matters: Maintain 1–1.5× channel diameter distance from cavity surface (e.g., 12mm channel → 12–18mm spacing).
✅ Standardize Components: Use ISO-standard channel diameters (e.g., 8mm, 10mm, 12mm) for machining ease and maintenance.
✅ Flow Optimization: Design for turbulent flow; avoid dead zones with proper inlet/outlet placement.
✅ Material-Specific Tuning: Adjust channel density for thick sections or high-heat plastics (e.g., PEEK, PSU).
✅ Thermal Simulation: Validate layout with Moldflow® or similar CAE tools pre-manufacturing.
✅ Maintenance Access: Include quick-connect fittings and corrosion-resistant materials (e.g., stainless steel lines).
Final Takeaway
Mastering cooling system design transforms molding efficiency. By aligning channel geometry, coolant dynamics, material science, and thermal simulation, manufacturers achieve:
✨ Shorter cycles
✨ Higher part consistency
✨ Reduced scrap rates
✨ Sustainable cost savings
Optimize your mold cooling strategy today—because every second saved in cooling multiplies across thousands of production cycles.
[^1]: Explore this resource to discover essential techniques and innovations that enhance injection molding efficiency and part quality. [^2]: Understand how turbulent flow maximizes heat transfer and improves cooling efficiency. [^3]: Learn how HDT affects part quality and performance during the injection molding process. [^4]: Explore the critical role of channel design in achieving uniform cooling and preventing defects.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean