 한국어



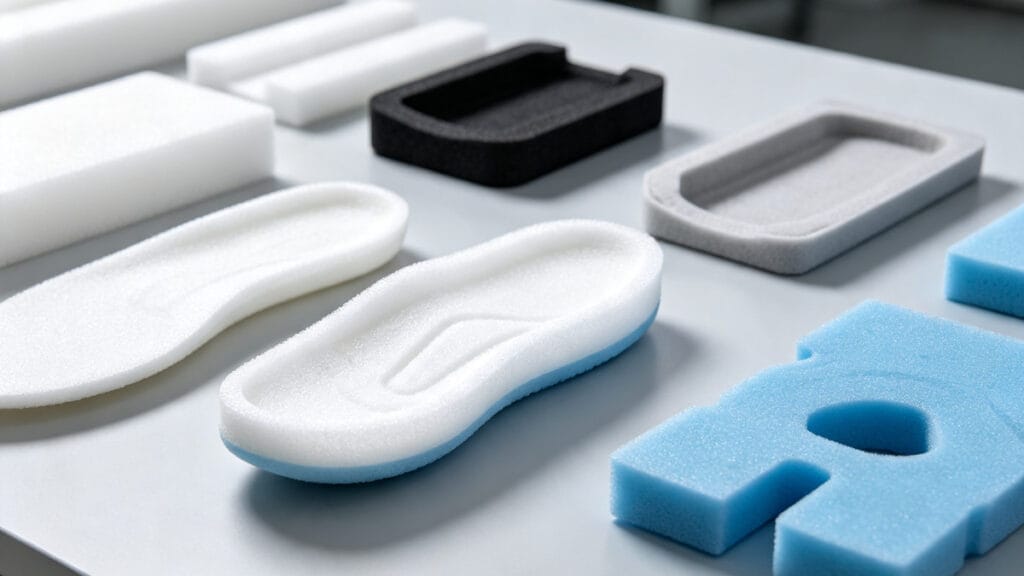
Ethylene-Vinyl Acetate (EVA) foam is a cornerstone material in modern manufacturing, widely used in footwear, packaging, sports equipment, and insulation. However, achieving the perfect balance of softness, resilience, and durability requires a deep understanding of EVA foaming processes and chemical formulations.
Whether you are in footwear manufacturing or industrial foam production, this comprehensive guide breaks down the core technologies, essential additives, and processing methods behind high-quality EVA foam.
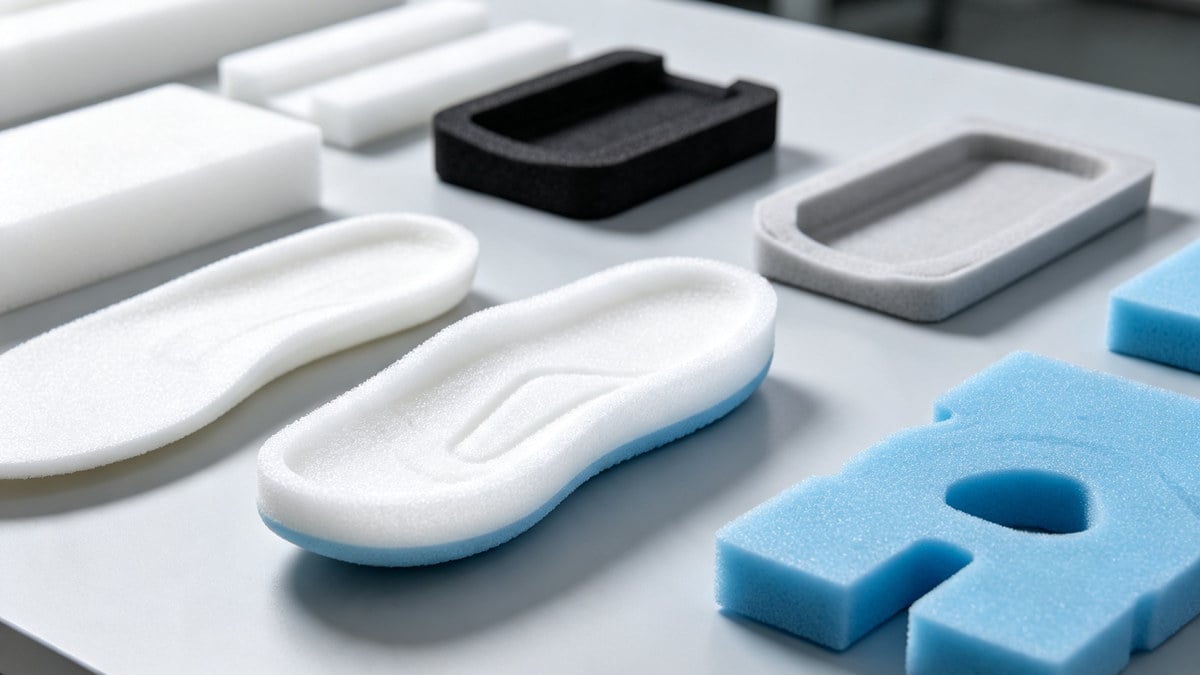
Classification of EVA Foaming Processes
EVA foam can be produced through several distinct manufacturing methods, each suited for different product requirements:
- Compression Molding: Includes primary foaming and secondary foaming.
- Injection Foaming: Commonly used for MD (midsoles) and flip-flops, similar to mainstream plastic injection molding principles introduced in our injection molding technical guide.
- Continuous Foaming: Typically used for EPE (foam sheets).
- Extrusion Foaming: Mainly used for producing rigid or flexible foam boards.
Generally, the industry relies on three primary manufacturing techniques: Injection Foaming, Mold-in Small Foaming (Secondary Midsole), 및 Traditional Flatbed Large Foaming.
The 3 Main EVA Foaming Technologies
A. Injection Foaming (The Industry Future)
Injection foaming is a highly advanced, single-step process that produces a finished product directly from the mold. Similar to plastic injection molding, it differs primarily in mold temperature control and mold-opening timing.
- 장점: High precision, excellent dimensional stability, and highly automated.
- 단점: Requires high-precision molds and significant initial capital.
- Application: Currently the mainstream choice for premium athletic shoe midsoles. For full injection molding process parameter optimization rules, check our dedicated article: Mastering Injection Molding Speed Segmentation Rules.
B. Mold-in Small Foaming (Secondary Midsole Process)
Widely used in athletic footwear, this two-step process offers great flexibility:
- Primary Foaming: Compounded EVA pellets (e.g., 7470M) are weighed and placed into a mold to create a rough, oversized blank. The key challenge here is balancing the formulation and mold design to control both the expansion ratio and hardness simultaneously.
- Secondary Molding: The rough blank is buffed to remove the skin and pressed into a final product mold. It undergoes heating (typically 125°C–135°C) at a pressure of 50 kg/cm², followed by water cooling.
- 장점: Excellent dimensional stability and superior physical properties.
C. Traditional Flatbed Large Foaming
Still popular among smaller factories due to low equipment costs, this method produces large foam boards that are later die-cut and edge-ground into final products.
- Processing Parameters: Foaming time is dictated by board thickness (approx. 90–110 seconds/mm), with temperatures ranging from 160°C–170°C and pressures around 150 kg/cm².
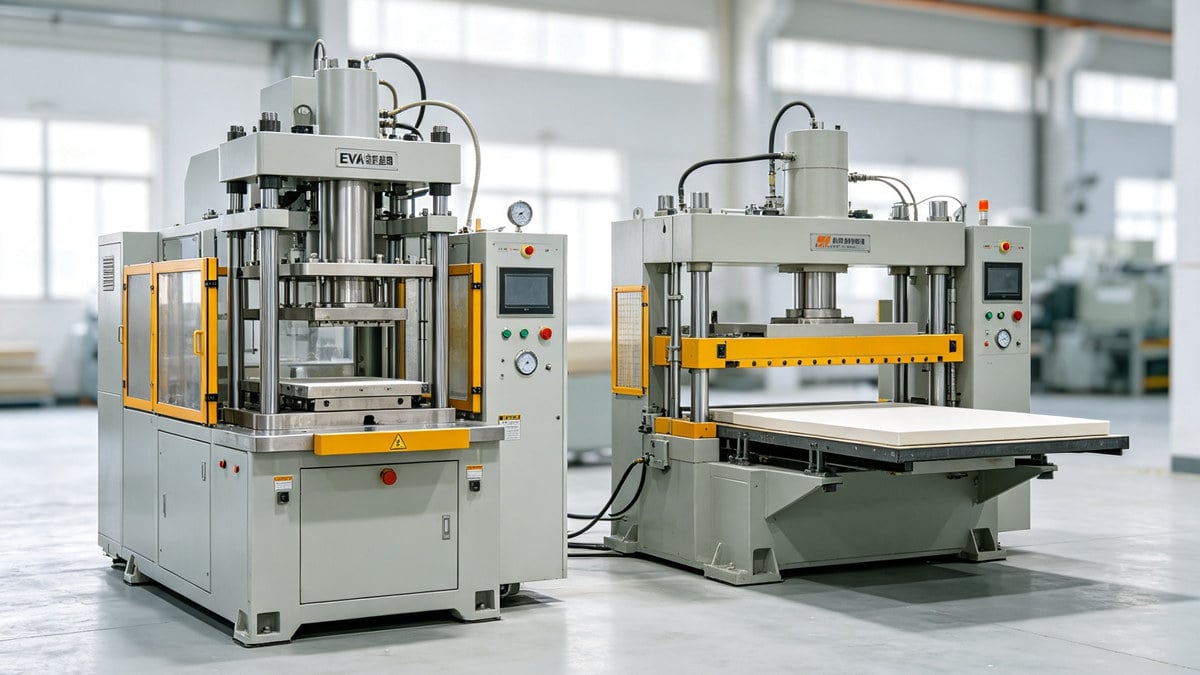
Essential EVA Foam Formulation & Additives
The performance of EVA foam is dictated by its chemical recipe. Below is a breakdown of the core ingredients and functional additives:
Base Resins
- EVA / LDPE: LDPE allows for higher expansion ratios and creates harder, less resilient foams, ideal for insulation, flip-flops, and packaging. Our Polyethylene (PE) Injection Molding Guide covers LDPE’s full processing characteristics for foam applications.
- EPDM: Added to significantly boost elasticity.
- Natural Rubber (NR): Incorporated to enhance slip resistance.
Chemical Additives Matrix
| Additive Category | Common Types | Function & Characteristics |
|---|---|---|
| Blowing Agents | High / Medium / Low Temp | High Temp: High expansion but affects color. Medium Temp: Ideal for injection/small molds. Low Temp: Best for MD and color-sensitive products. |
| Crosslinkers | DCP, BIPB, TAIC | DCP: Cost-effective but has a strong odor. BIPB: Odorless, reduces irritation. TAIC: Co-agent that accelerates crosslinking efficiency. |
| Zinc Oxide (ZnO) | Grade A, Active, Carbonate | Grade A: Best physical properties but pricey/risk of heavy metals. Active: Lower cost, safer. Carbonate: Fast foaming, suited for budget products. |
| Colorants | Masterbatch, Powder, Sand | Masterbatch: Best dispersion & color accuracy. Powder: Cheap but poor dispersion/polluting. Sand: Good dispersion, less pollution. |
| Lubricants | Stearic Acid, EBS | Improves machine processing, enhances melt flow, and gives the final product a better hand-feel and density. |
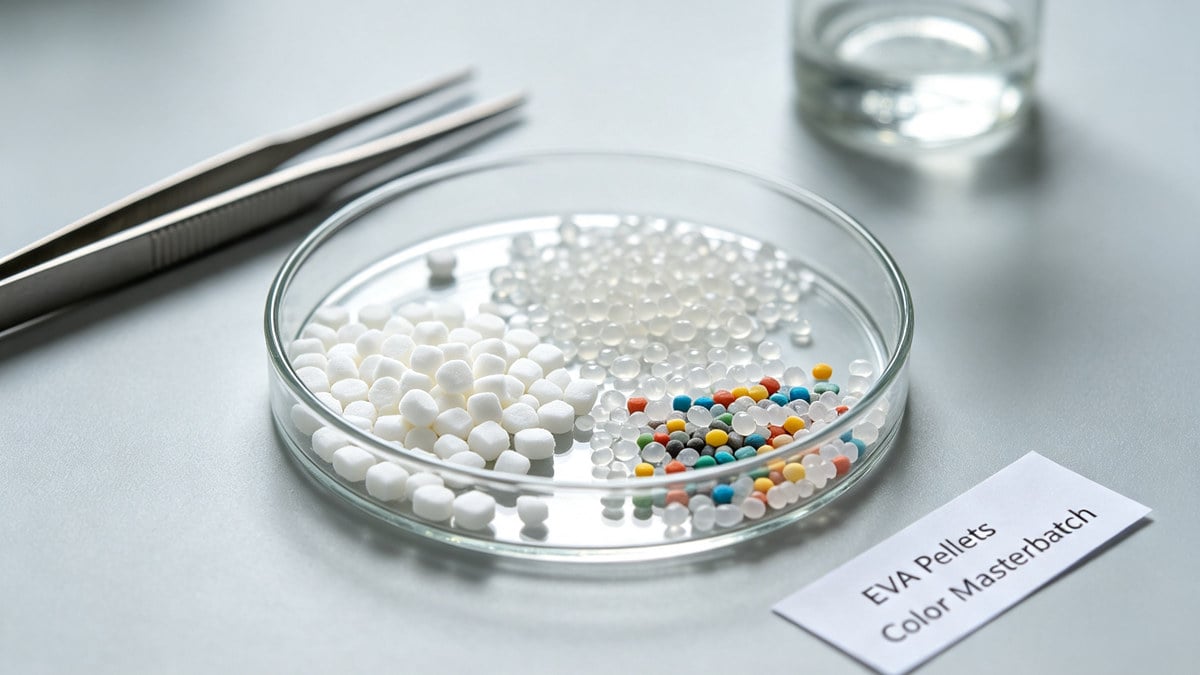
Functional Additives for Specialized Applications
Beyond the base formulation, modern EVA foam often requires specialized additives to meet specific industry standards:
- Wear-Resistant Agents: Crucial for outsoles to extend product lifespan.
- Anti-Slip Agents: Prevents slipping in low-friction environments.
- Flame Retardants: Enhances fire safety, typically measured by the Oxygen Index (OI).
- Antibacterial Agents: Essential for footwear and medical applications to prevent odor and bacterial growth.
- Anti-static / Conductive Agents: Required for electronic packaging to prevent electrostatic discharge (ESD).
EVA belongs to thermoplastic elastomer material families; read our full TPE material guide to compare EVA, TPU, TPE foam performance differences: Thermoplastic Elastomers (TPE) Injection Molding Guide.
Final Thoughts
Choosing the right EVA foaming process and formulation is a delicate balance of cost, performance, and production capability. While injection foaming is paving the way for the future of athletic footwear, traditional flatbed and mold-in processes remain vital for diverse industrial applications. Understanding your additives—from odorless crosslinkers to functional flame retardants—is the key to engineering superior foam products.
Are you looking to optimize your EVA foam production line or need advice on formulation? Leave a form below or contact our team of polymer experts!
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean