 한국어




Polypropylene, commonly known as PP, is renowned for its excellent resistance to bending fatigue, earning it the nickname "Hinge Plastic" or "Bǎi zhé jiāo" in Chinese. PP is a semi-transparent, semi-crystalline thermoplastic that boasts high strength, excellent electrical insulation, low moisture absorption, a high heat deflection temperature, low density, and high crystallinity.
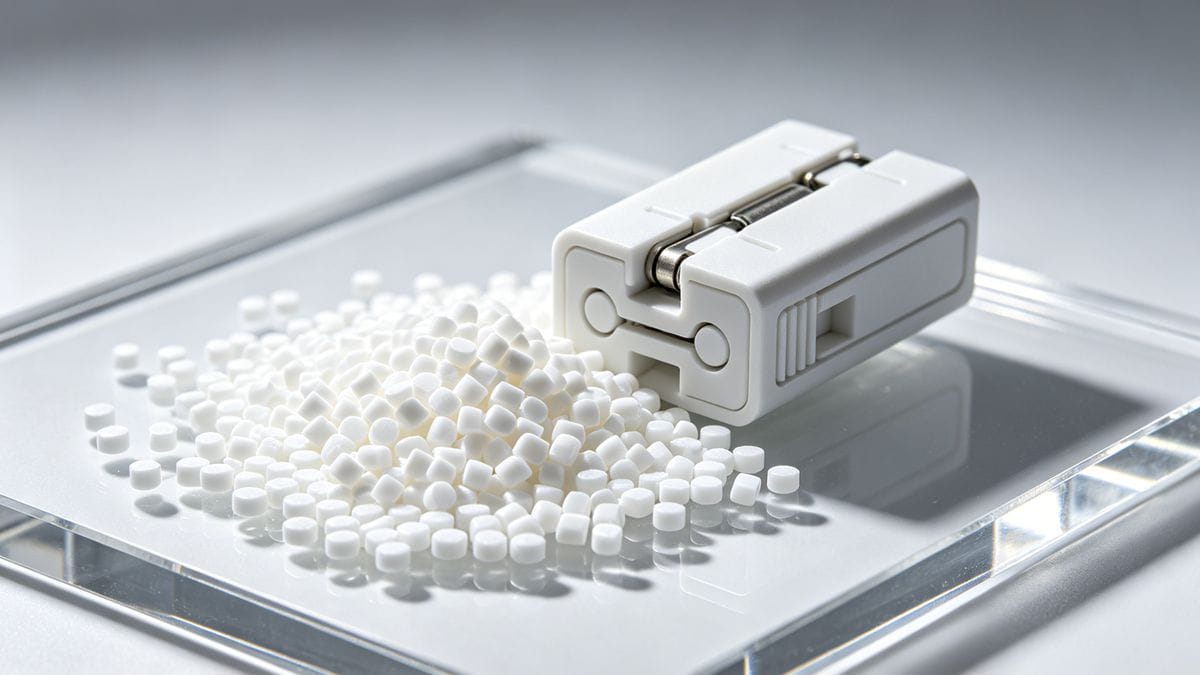
To enhance its properties for specific applications, PP is often modified with fillers such as glass fiber, mineral fillers, or thermoplastic rubber. The flow rate of PP varies significantly depending on its grade, but generally, its fluidity falls between that of ABS and PC.
Here is a detailed breakdown of the injection molding process for Polypropylene[^1].
1. Material Preparation and Handling
Pure PP is a semi-transparent ivory white granule that can be colored in various shades.
- Coloring: On standard injection molding machines, PP is typically colored using masterbatches (color concentrate). However, machines with independent plasticizing elements that enhance mixing (like certain Hongmeida models) can also use color powder.
- Recycling: The proportion of recycled material should not exceed 15%. Exceeding this limit can lead to decreased strength, degradation, and color variation.
- Drying: Generally, PP does not require special drying treatment before 사출 성형[^2], provided it is stored properly.
> ? Pro Tip: For outdoor applications, ensure the PP compound includes UV stabilizers and carbon black to prevent degradation from sunlight.
2. Injection Molding Machine Selection
There are no special requirements for the injection molding machine itself. However, due to the high crystallinity of PP, it is advisable to use a computer-controlled machine capable of high injection pressures and multi-stage control.
- Clamping Force: Generally calculated at 3800 t/m².
- Shot Volume: The injection volume should ideally be between 20% and 85% of the machine's capacity.

3. Mold and Gate Design
Mold design is critical for PP due to its shrinkage characteristics.
- Mold Temperature: Typically 50–90°C. Use higher mold temperatures for parts with strict dimensional requirements. The core temperature should be at least 5°C lower than the cavity temperature.
- Runners: Sprue diameter should be 4–7mm.
- Gates:
- Pin gates: Length 1–1.5mm, diameter can be as small as 0.7mm.
- Edge gates: Keep length short (approx. 0.7mm), depth at half the wall thickness, and width at twice the wall thickness.
- 하소연: The mold must have excellent venting. Venting slots should be 0.025mm–0.038mm deep and 1.5mm thick.
- Avoiding Sink Marks: Use large, round sprues and circular runners. Ribs should be thin (approx. 50–60% of the wall thickness).
- Wall Thickness: Products made from homopolymer PP should not exceed 3mm in thickness to avoid air traps; copolymer PP is required for thicker walls.
4. Processing Parameters Table
To help you visualize the optimal settings, here is a summary of the key processing parameters:
| 매개변수 | Recommended Setting | Notes |
|---|---|---|
| 용융 온도 | 240°C (Range: 160–275°C) | Do not exceed 275°C to prevent decomposition. |
| 금형 온도 | 50°C – 90°C | Higher temp for better gloss and dimensions. |
| 사출 압력 | 1500 – 1800 bar | High pressure helps reduce shrinkage. |
| 배압 | 5 bar | Increase slightly for color masterbatch. |
| 사출 속도 | High Speed | Reduces internal stress; use slow speed for textured surfaces. |
5. Melt Temperature Details
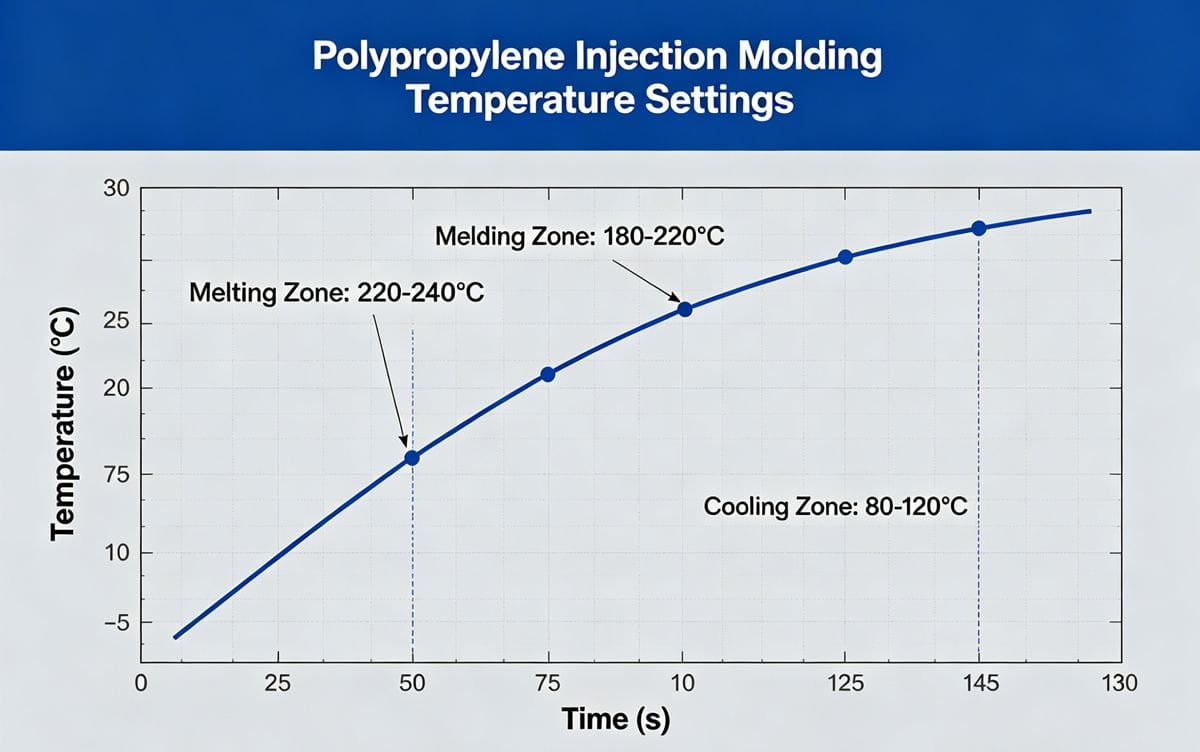
While the melting point of PP is between 160°C and 175°C, and its decomposition temperature is around 350°C, the processing temperature should never exceed 275°C. The optimal melt temperature[^3] for the melt section is around 240°C.
6. Injection Speed
To minimize internal stress and warpage, high-speed injection is generally recommended. However, for certain grades of PP or specific mold designs, high speed may cause air traps or flow marks.
- Textured Surfaces: If you notice light/dark streaks radiating from the gate on a textured surface, switch to low-speed injection combined with a higher mold temperature.
7. Injection and Holding Pressure
PP requires relatively high injection pressure (1500–1800 bar). The holding pressure[^4] should be approximately 80% of the injection pressure.
- Switch-over Point: Switch to holding pressure at roughly 95% of the full stroke.
- Duration: Use a longer holding time to ensure proper packing and reduce shrinkage.
8. Post-Processing
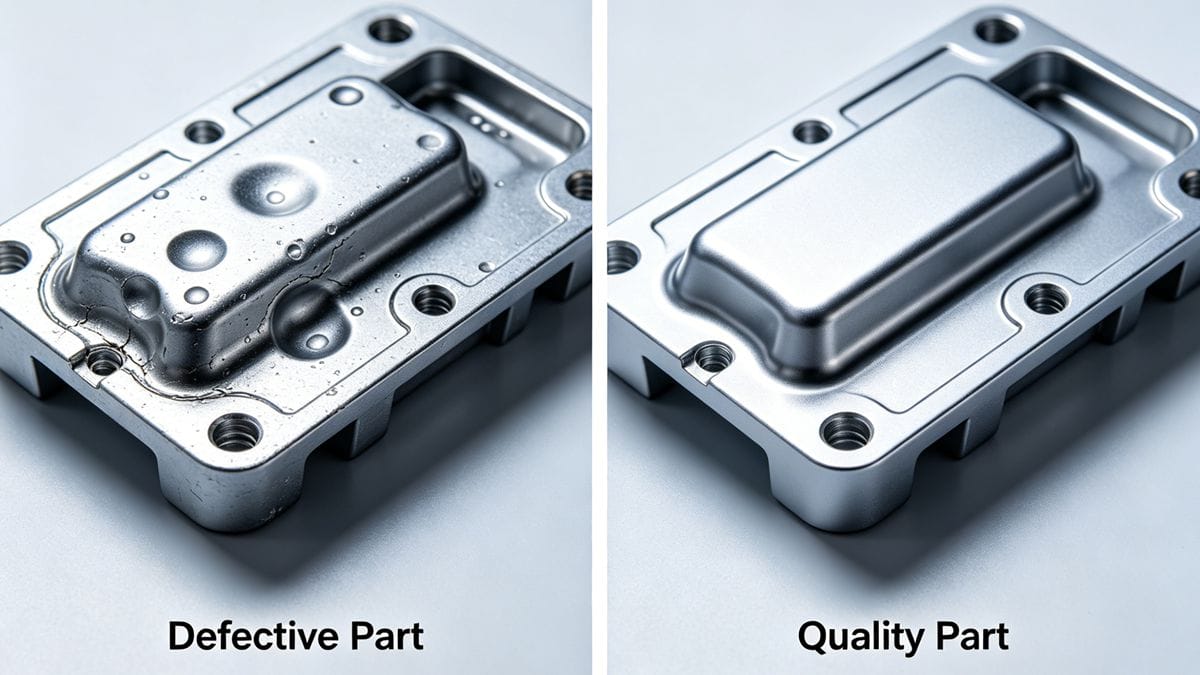
To prevent dimensional changes caused by post-crystallization shrinkage, finished products often require a post-treatment process, such as soaking in hot water.
[^1]: Explore the diverse applications and unique properties of Polypropylene, a versatile thermoplastic. [^2]: Learn about the injection molding process, a key technique in manufacturing plastic products. [^3]: Learn why melt temperature is crucial in the injection molding process and how it affects product quality. [^4]: Explore the role of holding pressure in injection molding and its impact on product integrity.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean