 日本語



Polyethylene (PE)[^1] is one of the most widely used crystalline raw materials in the plastics industry. Understanding its unique processing characteristics—from moisture resistance to shrinkage behavior—is essential for manufacturing high-quality parts.
In this post, we break down the processing performance and key molding conditions for PE.
PE Processing Characteristics
To optimize your 射出成形[^2] cycle, you must understand how Polyethylene behaves under heat and pressure.
- Moisture Resistance: PE has extremely low hygroscopicity (moisture absorption 注: Because shrinkage directionality is obvious, parts are prone to deformation and warping. Uniform mold cooling is critical to minimize this.
- Crystallinity: PE has high crystallization ability. Mold temperature directly affects the crystallinity of the part. Higher mold temperatures lead to slower cooling, higher crystallinity, and increased strength.
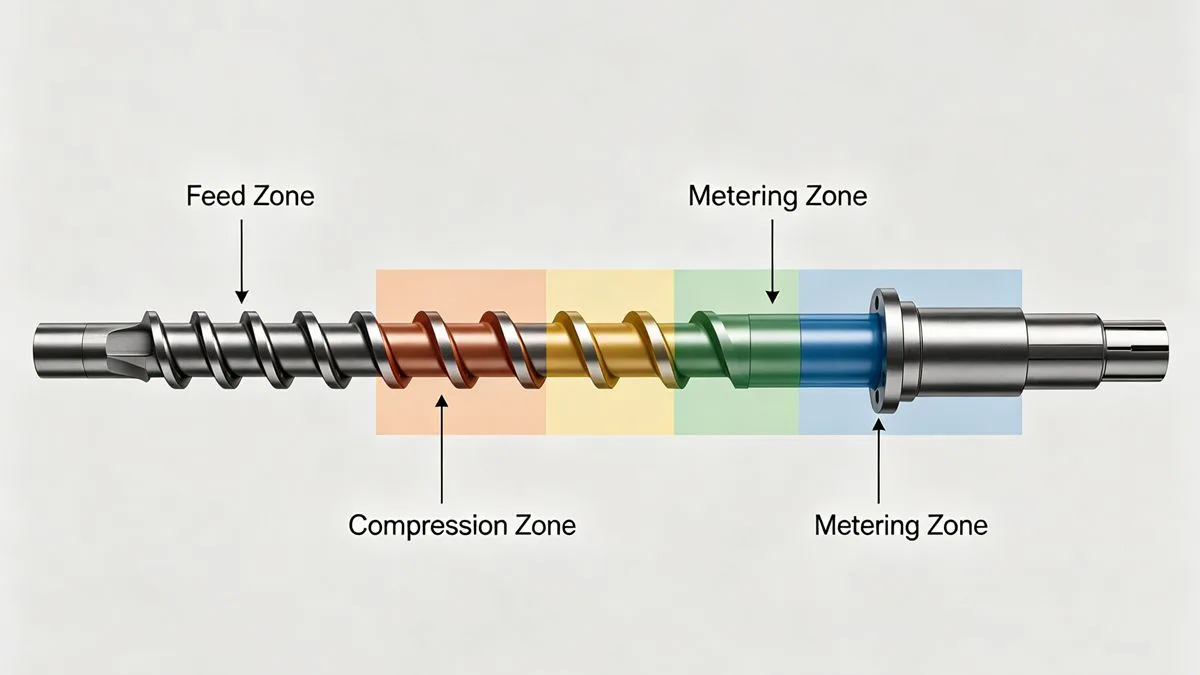
- Thermal Properties: Although PE has a low melting point, it has a high specific heat capacity. Therefore, the plasticizing unit requires high heating power to maintain efficiency.
- Oxidation Sensitivity: While PE has good thermal stability (no decomposition below 300°C), the melt oxidizes easily. Avoid prolonged contact between the melt and oxygen to prevent quality degradation.
- 退場: PE parts are soft and easy to eject. Parts with shallow undercuts can often be forced off the mold (forced ejection).
Key Molding Parameters
Setting the correct machine parameters is vital. Below is a breakdown of the optimal conditions for LDPE and HDPE.
温度管理
The barrel temperature depends on the density of the PE and the Melt Flow Rate (MFR). Since PE is crystalline, the barrel temperature should be at least 10°C above its melting point.
| パラメータ | LDPE (Low Density) | HDPE (High Density) | Notes |
|---|---|---|---|
| Barrel Temp | 140°C – 200°C | Up to 220°C | Rear zone: Lowest temp.Nozzle/Front zone: Highest temp. |
| Mold Temp | 30°C – 45°C | 40°C – 65°C | Higher mold temp = Higher crystallinity & strength. |
Pressure & Cooling
- 射出圧力[^3]: Because PE flows so well, you should aim for the lowest effective pressure.
- General Range: 50 – 100 MPa.
- Simple/Thick Parts: Use lower pressure.
- Thin-Walled/Complex Parts: Use higher pressure to ensure filling.
- Cooling Time: PE cools slowly and must be cooled sufficiently. Ensure your mold has an efficient cooling system to reduce cycle times.
3. Gate Design and Troubleshooting
The design of the feed system (gate) plays a crucial role in the final quality of the PE part.
- Gate Selection: If using a direct sprue gate, be aware that it can increase residual stress and cause uneven flow orientation, leading to significant warping. Carefully select gate dimensions to balance flow.
- Viscosity Behavior: PE melt viscosity is not strongly affected by shear rate changes (non-Newtonian behavior is less pronounced than other plastics). Temperature fluctuations in the flow state have minimal impact on the molding process, making PE a stable material to work with.
Summary Table: Quick Reference
| 特徴 | Recommendation |
|---|---|
| Drying Required? | No (unless recycled/wet stored). |
| Flowability | Excellent (Good for thin walls). |
| Main Challenge | Controlling shrinkage and warpage. |
| Ideal Application | Caps, containers, household goods, toys. |
By controlling the mold temperature and ensuring uniform cooling, you can leverage Polyethylene's excellent flow and toughness to produce durable, high-quality components.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean