 Français



Why Do Custom Plastic Injection Products Crack? A Comprehensive Troubleshooting Guide
Plastic injection molding[^1] is a precise art, but defects can still occur. One of the most frustrating issues manufacturers face is cracking in injection-molded parts.
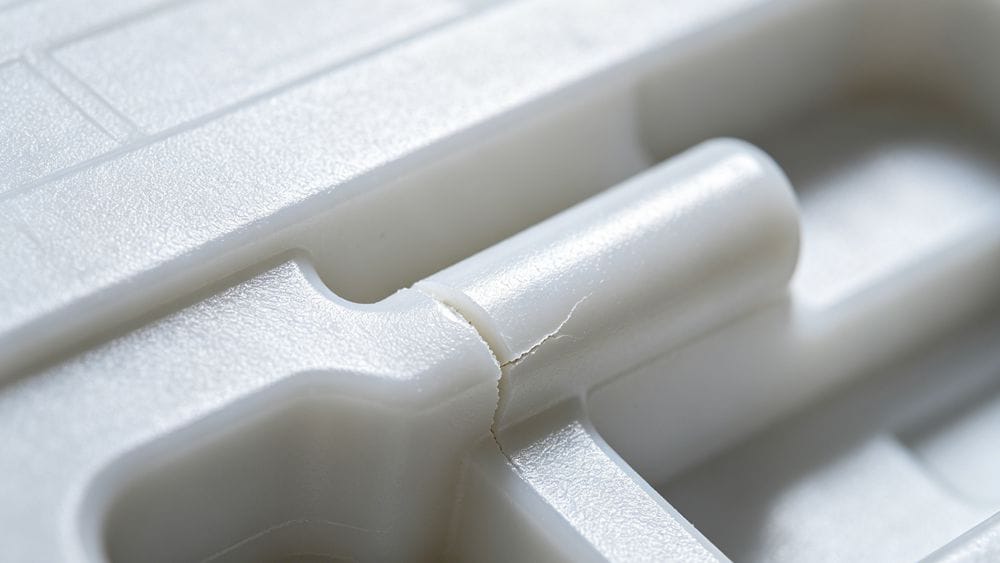
Cracking can manifest as surface crazing (silky cracks), micro-cracks, stress whitening (white marks at stress points), or complete fracture. These defects can happen immediately during demolding or later during the product's application.
In this guide, we break down the root causes of these cracks—ranging from processing errors to mold design flaws[^2]—and provide actionable solutions. > Point à retenir : Cracking is rarely caused by a single factor. It is usually a combination of residual stress, external force, and material weakness.
1. Processing Factors (Machine Settings)
Improper machine settings are the most common cause of internal stress leading to cracks.
- Excessive Pressure & Speed: If the injection pressure is too high, the filling speed is too fast, or the packing time is too long, the part will suffer from excessive internal stress.
- Demolding Speed: If the mold opens too quickly or with too much force, it can physically pull and crack the part, especially if it hasn't cooled sufficiently.
- Contrôle de la température :
- Mold Temperature: If the mold is too cold, the part may not release easily, leading to stress.
- Material Temperature: If the barrel temperature is too high, the plastic may degrade (burn), reducing its mechanical strength.
- Weld Lines: Poor processing can lead to weak weld lines where the plastic flow fronts meet, creating weak points prone to cracking.
Solutions :
- Réduire la pression et la vitesse d'injection.
- Shorten injection and holding times.
- Adjust the mold opening speed to be smoother.
- Annealing: Perform heat treatment (annealing) immediately after molding to relieve residual stress.
2. Questions relatives à la conception des moules
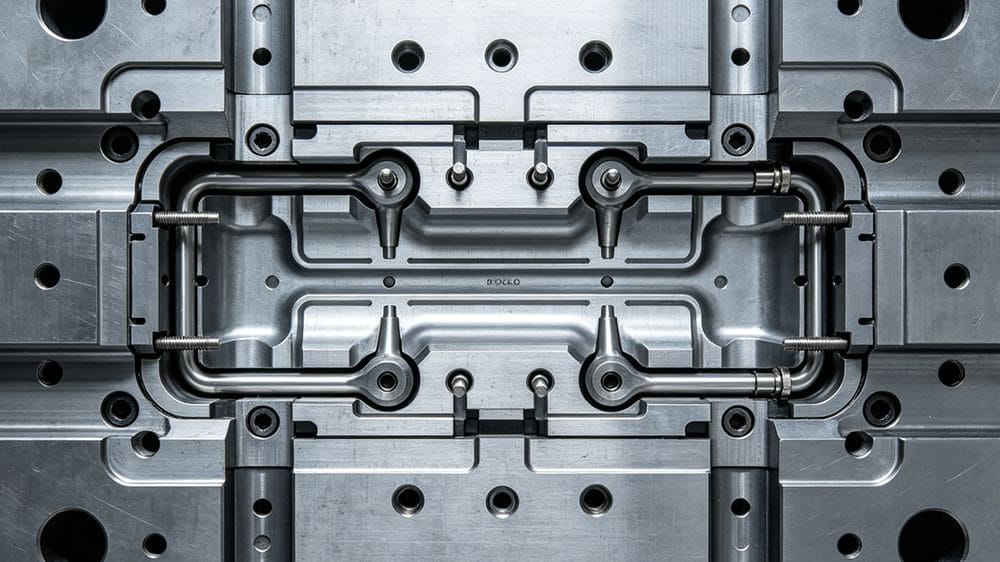
The physical design of the mold dictates how the plastic flows and cools. Flaws here create inherent weak points.
- Ejection System: If the ejector pins are unbalanced, too few, or have too small a surface area, the ejection force concentrates on small areas, causing cracks.
- Sharp Corners: Sharp corners act as stress concentrators.
- Metal Inserts: Using metal inserts can be problematic because metal and plastic shrink at different rates during cooling, creating high internal stress around the insert.
- Vacuum Lock: Deep-draw parts need air vents. Without them, a vacuum forms, making the part stick and potentially crack during ejection.
Solutions :
- Ensure sufficient draft angles and polished cavity surfaces.
- Use fillets (rounded corners) instead of sharp angles to distribute stress.
- Minimize the use of metal inserts or design the mold to accommodate shrinkage differences.
- Add vents to deep cavities to prevent vacuum formation.
3. Material Selection & Quality
Even with a perfect mold and machine, bad material will result in failure.
- Matériaux recyclés : Using too much regrind (recycled plastic) lowers the tensile strength and impact resistance of the part.
- Moisture: Many engineering plastics (like Nylon or PC) are hygroscopic. If not dried properly, moisture reacts with the polymer during melting (hydrolysis), causing the material to become brittle and crack.
- Contamination: Mixing different types of plastics or using contaminated raw materials will compromise structural integrity.
4. Machine & Process Factors
- Plasticizing Capacity: The injection molding machine must be sized correctly.
- Too Small: The plastic won't mix or melt thoroughly, leading to brittleness.
- Too Large: The plastic stays in the barrel too long and degrades due to heat.
- Back Pressure & Screw Speed: Excessive contre-pression[^3] or screw speed generates shear heat, degrading the material properties.
Summary: Troubleshooting Table
Here is a quick reference guide to help you diagnose the source of the cracking.
| Catégorie | Potential Cause | Recommended Solution |
|---|---|---|
| Processing | High Injection Pressure / Speed | Lower pressure; Reduce injection speed. |
| Processing | High Residual Stress | Increase mold temp; Anneal part after molding. |
| Conception des moules | Sharp Corners / Bad Geometry | Add radius (fillets) to corners; Avoid sharp transitions. |
| Conception des moules | Ejection Issues | Polish cavity; Increase draft angle; Balance ejector pins. |
| Matériau | Moisture / Wet Resin | Dry material properly before processing. |
| Matériau | Too much Recycled Content | Reduce regrind ratio; Use virgin material. |
| Machine | Degradation | Check barrel temperature; Ensure correct screw size. |
Conclusion
Cracking in custom plastic injection products is a complex issue that requires a systematic approach to solve. By analyzing the paramètres de traitement, conception de moules, et material quality, you can identify the root cause.
Start by checking your material drying process and reducing injection speeds, as these are the most common culprits. If problems persist, review your mold design for stress concentrators like sharp corners or insufficient draft angles.
Need help with your injection molding project? Contact us today for expert manufacturing solutions.
[^1]: Explore this resource to discover essential best practices that enhance quality and efficiency in plastic injection molding. [^2]: Identifying mold design flaws is crucial for improving product quality. [^3]: Understanding back pressure can help optimize your injection molding process.
À propos de l'auteur

Alex Yu
Ideal Pro Manufacturing
Alex est le cofondateur d’Ideal Pro, mais lorsqu’il ne supervise pas des projets clés ou ne dirige pas l’équipe technique, vous le trouverez sans doute en train de faire une longue balade à vélo, à la recherche du meilleur café de la ville, ou en train de planifier sa prochaine aventure de voyage. Fort de plus de 20 ans d’expérience dans le commerce international et la gestion de projets, il a tout vu : délais serrés, problèmes techniques complexes et tout ce qui se trouve entre les deux. Il est convaincu qu’un travail de qualité naît d’un esprit bien reposé et d’une bonne tasse de café, et il apporte cette même curiosité et ce même souci du détail à chaque projet qu’il entreprend. Lorsqu’il n’est pas au bureau, il se trouve généralement en plein air, à explorer de nouveaux endroits et à glaner des anecdotes à partager.




 English
 French
 Dutch
 German
 Japanese
 Korean