 Deutsch



Einführung
Selecting the right colorant for engineering plastics is a complex process. While many organic pigments, inorganic pigments, and solvent dyes work well for general thermoplastics, high-performance materials like Nylon (Polyamide) have strict requirements.
Below, we explore the five critical performance characteristics colorants must possess for successful Nylon injection molding[^1].
1. Heat Resistance and Lightfastness
The processing temperature of the resin dictates the stability requirements for the colorant. As shown in the table below, Polyamide (Nylon) requires some of the highest processing temperatures among engineering plastics[^2].
Processing Temperatures and Colorant Requirements by Resin Type
| Resin Type | Processing Temp (℃) | Key Colorant Requirements |
|---|---|---|
| Polyamid (Nylon) | 270 - 290 | Heat resistance, Water-free, Good dispersion |
| Polyester | 270 - 290 | Heat resistance, Non-migrating, Neutral pH |
| ABS | 230 - 310 | Heat resistance, Good dispersion |
| Polypropylene | 230 - 280 | Heat resistance, Good dispersion |
| Polyurethane | 210 - 270 | Lightfastness, Acid/Reduction resistance |
| PMMA | 200 - 230 | Fastness, Heat resistance, Non-migrating |
| PVC | 180 - 250 | Good dispersion, Acid resistance |
| Polystyrene | 180 - 240 | Fastness, Good solubility |
| Polycarbonat | 150 - 200 | Heat resistance, Water-free, Good dispersion |
| HDPE | 160 - 230 | High thermal stability, Non-migrating |
| LDPE | 150 - 220 | Excellent fastness, Non-migrating |
> Anmerkung: Due to the high processing temperatures of Polyamide, colorants must exhibit exceptional thermal stability. Many organic pigments can negatively affect the properties of the Nylon melt, limiting the selection to specific high-performance pigments with good lightfastness.
2. Chemical Stability
There must be no chemical reaction between the colorant and the resin, nor should the colorant promote resin decomposition.
Polyamide resins (PA) are highly active. In their molten state, they exhibit reducing properties, which can easily cause colorants to shift in hue or degrade. Therefore, the choice of colorants for Nylon is limited to those with high chemical inertness.
3. Migration Resistance
Migration refers to the movement of the colorant within the polymer or to the surface. There are three main types:
- Solvent Extraction: Leaching of color in water or organic solvents.
- Contact Migration: Staining of adjacent objects or packaging.
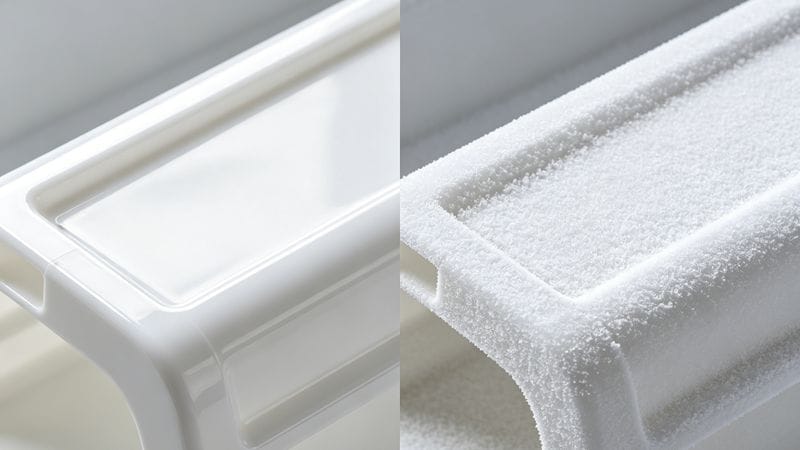
- Blooming (Surface Frosting): The colorant has high solubility at high heat but low solubility at room temperature, causing it to migrate to the surface as the part cools.
Inorganic vs. Organic: Generally, inorganic pigments are heterogeneously dispersed in polymers and rarely bloom. In contrast, organic pigments have varying degrees of solubility in polymers, making them more prone to migration issues.
4. Tinting Strength
Tinting strength determines the dosage of colorant required to achieve the target color.
- Particle Size: Generally, tinting strength increases as the pigment particle size decreases.
- Organic vs. Inorganic: Organic pigments[^3] typically have higher tinting strength than inorganic pigments.
- Mixing: Tinting strength can be significantly improved when colored pigments are used in combination with white pigments.
5. Dispersion
For optimal coloring results, the colorant must be uniformly dispersed in the polymer as microscopic particles.
Pigments often contain many aggregated particles. To achieve the desired quality, high shear force is required during the compounding process to break down large aggregates into smaller clusters. Poor dispersion leads to color streaks and weak points in the final part.
[^1]: Explore this resource to gain insights into optimal techniques and tips for successful Nylon injection molding. [^2]: Explore this resource to gain in-depth knowledge about engineering plastics, their properties, and applications in various industries. [^3]: Organic pigments can offer vibrant colors and higher tinting strength, making them valuable for specific applications.
Über den Autor

Alex Yu
Ideal Pro Manufacturing
Alex ist Mitbegründer von Ideal Pro, doch wenn er nicht gerade wichtige Projekte beaufsichtigt oder das technische Team leitet, trifft man ihn wahrscheinlich auf einer langen Radtour, auf der Suche nach dem besten Kaffee der Stadt oder bei der Planung seines nächsten Reiseabenteuers. Mit über 20 Jahren Erfahrung in den Bereichen internationaler Vertrieb und Projektmanagement hat er schon alles gesehen – enge Fristen, knifflige technische Probleme und alles, was dazwischen liegt. Er ist davon überzeugt, dass großartige Arbeit von einem ausgeruhten Geist und einer guten Tasse Kaffee entsteht, und er bringt dieselbe Neugier und Liebe zum Detail in jedes Projekt ein, das er übernimmt. Wenn er nicht im Büro ist, befindet er sich meist irgendwo im Freien, erkundet neue Orte und sammelt Geschichten, die er gerne weitergibt.




 English
 French
 Dutch
 German
 Japanese
 Korean