 한국어



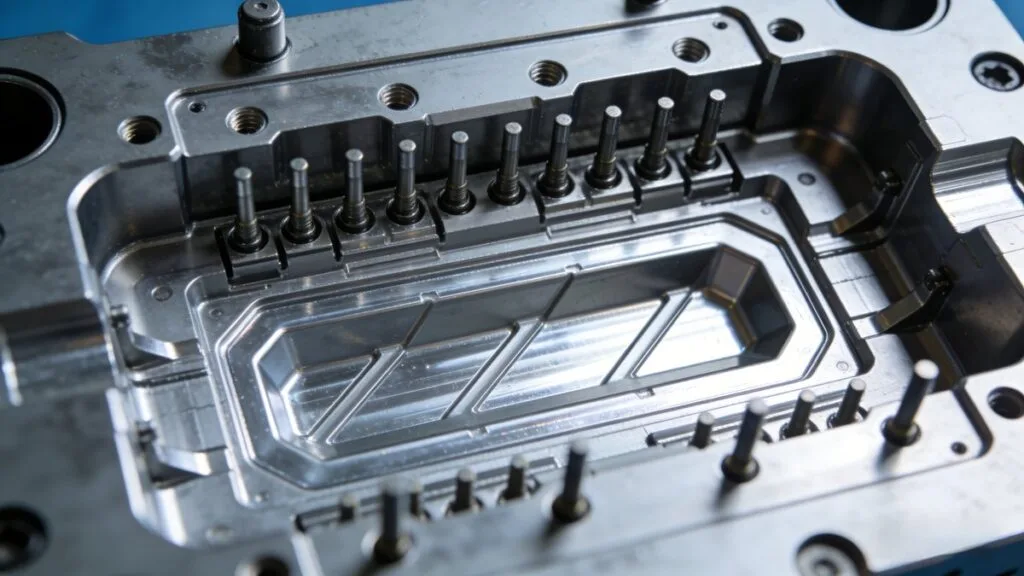
Cracking in injection-molded parts[^1]—whether visible as fine surface crazing, micro-cracks, ejection whitening, full fractures, or damage caused by sticking to the mold (e.g., part or runner adhesion)—can severely compromise product quality and reliability. Cracks may appear immediately after demolding (demolding cracks) or later during use (in-service cracks[^2]).
Below are the primary root causes, categorized by origin—and practical solutions to prevent them.
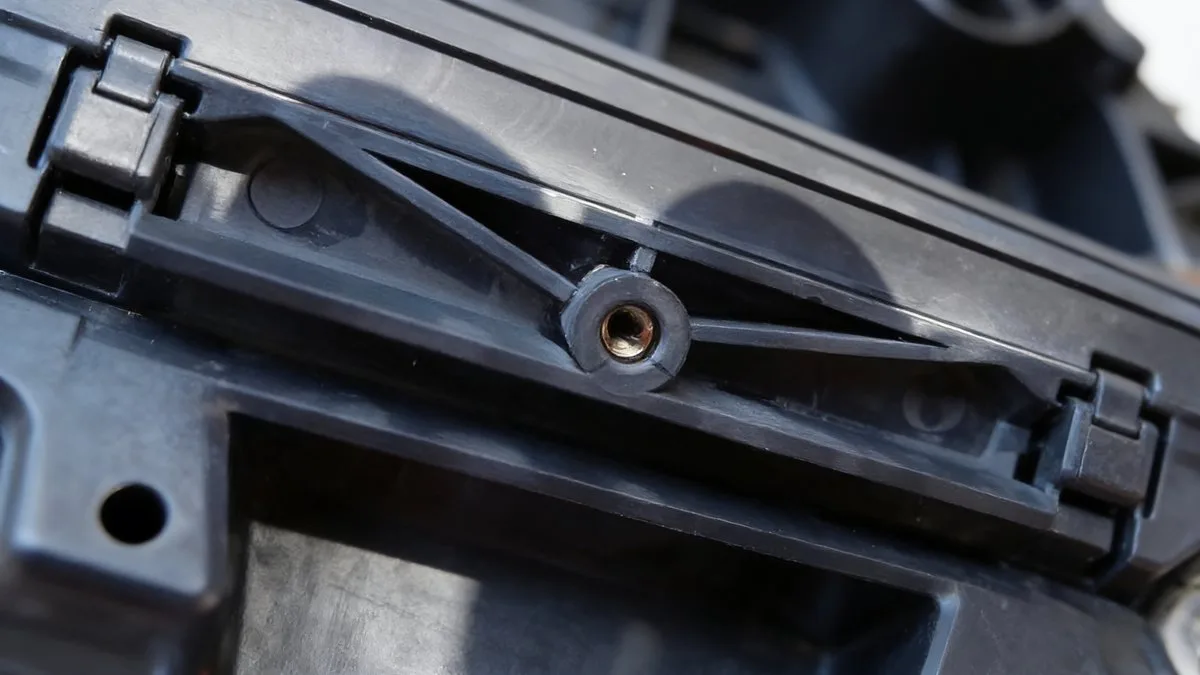
1. Processing Factors
(1) Excessive Processing Parameters[^3]
Overly high injection pressure, fast injection speed, excessive filling volume, or prolonged injection/holding times can generate excessive internal stress, leading to cracking.
(2) Improper Demolding Practices
Rapid or forceful ejection can mechanically stress the part. Adjust ejection speed and pressure to avoid sudden pulling forces that cause demolding cracks.
(3) Mold & Material Temperature Control
- Raise mold temperature slightly to improve part release and reduce thermal stress.
- Lower melt temperature appropriately to prevent thermal degradation—especially critical for heat-sensitive resins.
(4) Weld Lines & Material Degradation
Weld lines (melt fronts meeting) and polymer degradation weaken mechanical strength. Optimize gate location, venting, and processing conditions to minimize these issues.
(5) Mold Release & Surface Contamination
Use mold release agents sparingly and correctly. Regularly clean mold surfaces to remove condensation, oil mist, or residue that may interfere with release or cause surface defects.
(6) Residual Stress Relief
Post-molding annealing (heat treatment) immediately after production helps relieve internal stresses and significantly reduces the risk of delayed cracking.
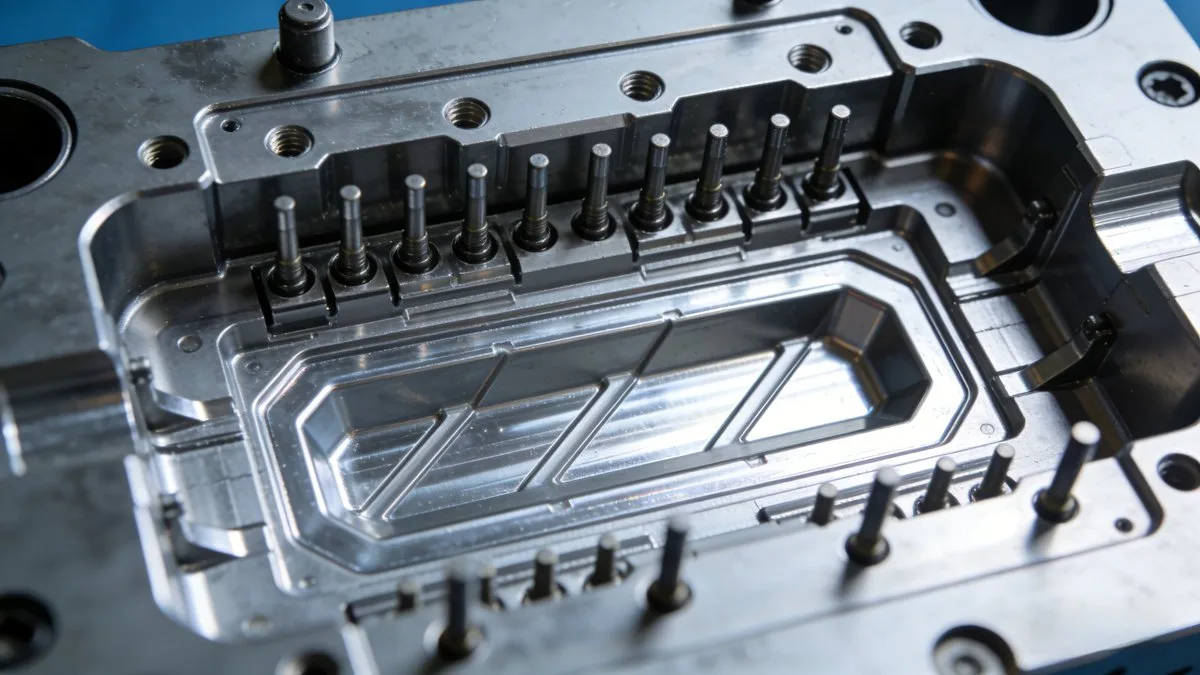
2. Mold Design Issues
(1) Uneven Ejection System
Ensure balanced ejection: sufficient ejector pin count and cross-sectional area, adequate draft angles, and highly polished cavity surfaces—all help prevent localized stress concentration during ejection.
(2) Poor Part Geometry[^4]
Avoid sharp corners, thin sections, or abrupt transitions. Use generous fillets and radii to distribute stress evenly and prevent stress concentration points.
(3) Metal Inserts
Minimize use of metal inserts—differential shrinkage between metal and plastic creates high internal stresses. If unavoidable, design insert geometry carefully (e.g., knurling, undercuts) to improve bonding and reduce stress.
(4) Vacuum Trapping in Deep Cavities
For deep-cavity parts, incorporate air vents or vacuum break channels to prevent vacuum lock, which makes ejection difficult and risks part deformation or cracking.
(5) Runner & Gate Design
- Ensure the sprue is large enough so that the gate “frozen” only after part ejection—this avoids pulling forces during release.
- The sprue bushing must fit tightly with the nozzle to prevent cold slug drag, which can cause the part to stick to the fixed half.
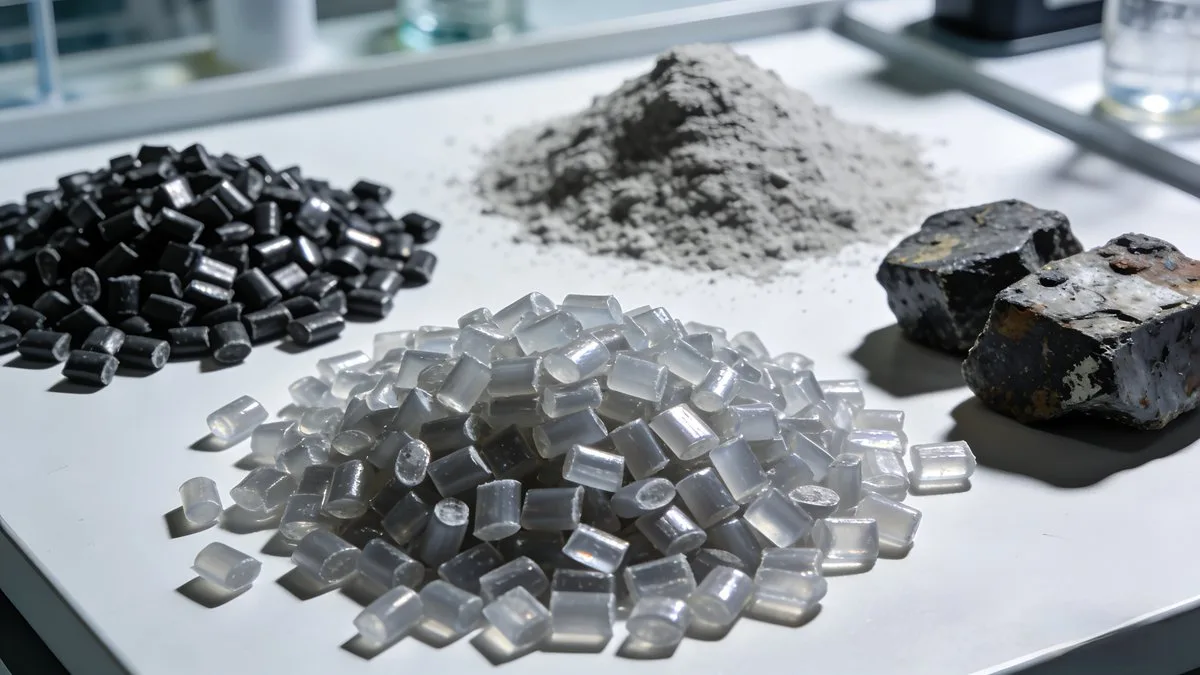
3. Material-Related Causes
(1) High Recycled Content
Excessive regrind or recycled material reduces tensile strength and impact resistance—leading to brittle failure and cracking.
(2) Moisture Absorption
Hygroscopic resins (e.g., PA, PET, PC) must be thoroughly dried before processing. Moisture can cause hydrolysis, degrading molecular weight and mechanical properties—resulting in ejection cracks or in-service failure.
(3) Incompatible or Contaminated Materials
Using resin grades unsuited for the application (e.g., wrong grade for high-temp use), or contaminated batches (e.g., foreign polymers, dust, degraded particles), can lead directly to premature cracking.
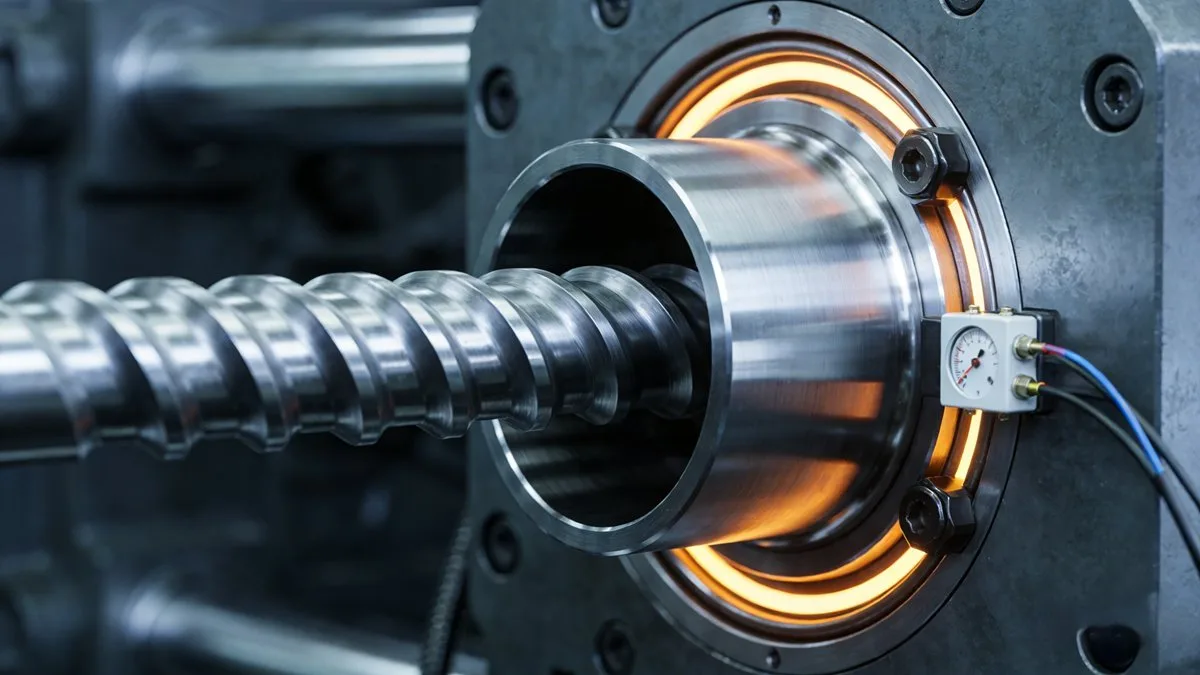
4. Machine-Related Factors
(1) Mismatched Plasticizing Capacity
- Too small a barrel/screw capacity → incomplete melting/mixing → weak, brittle parts.
- Too large a capacity → excessive residence time → thermal degradation → loss of mechanical integrity.
Ensure your machine’s (plasticizing) capability matches the shot size and material requirements.
Final Tip: A Holistic Approach Wins
Cracking is rarely due to a single factor—it’s usually a combination of processing, mold, material, and equipment issues. Conduct systematic root-cause analysis (e.g., DOE, FMEA) and validate fixes with prototype testing.
[^1]: Explore this resource to discover effective strategies and insights for enhancing the quality and reliability of injection-molded parts. [^2]: Exploring in-service cracks will provide insights into maintaining product reliability during usage. [^3]: Learn how processing parameters impact product quality and how to optimize them for better results. [^4]: Learn how to design parts effectively to minimize stress concentration and enhance durability.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean