 한국어



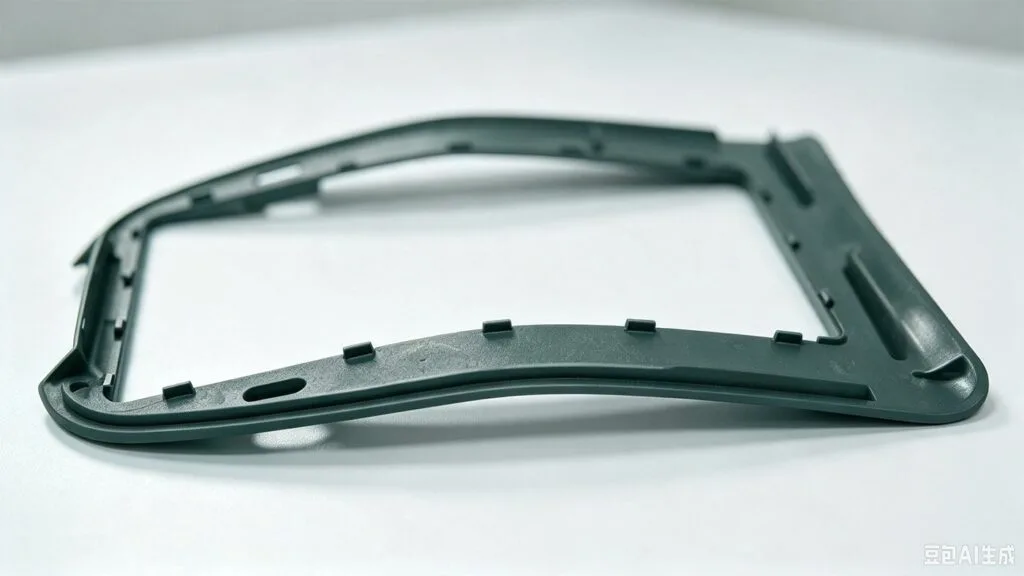
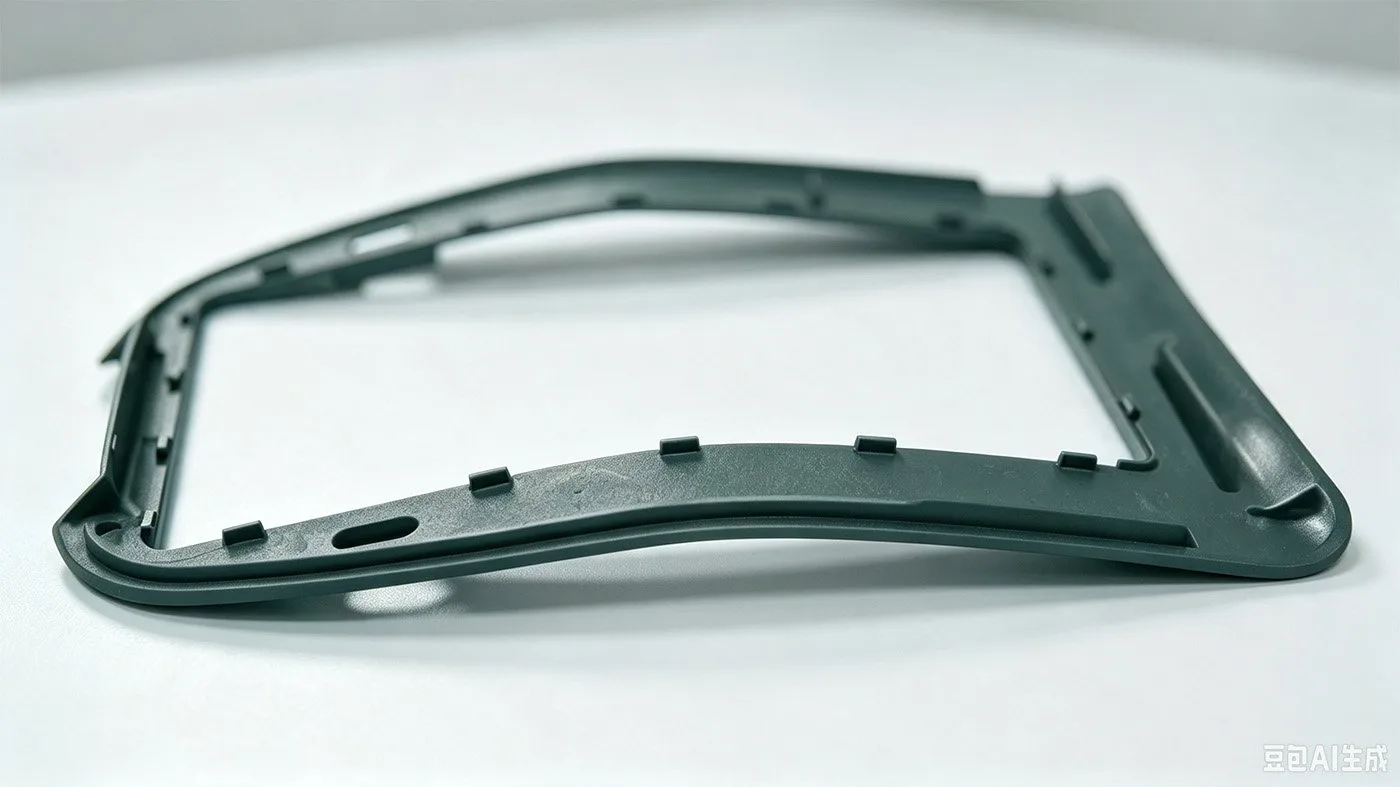
Large, flat injection molding parts are notoriously difficult to manufacture. Due to their expansive surface area, these parts experience significant shrinkage. When combined with severe molecular orientation and uneven mold cooling, the shrinkage rates vary across different directions. This inconsistency frequently leads to warpage and twisting, especially in thin-walled large panels.
Furthermore, if a flat part features support ribs on one side, the differential cooling and shrinkage will inevitably cause the part to warp toward the ribbed side.
Completely eliminating warpage in large flat parts is a complex challenge. However, through extensive production experience, we have identified four highly effective strategies to mitigate this issue and improve dimensional stability. > Related reading: Injection Molding Warpage: Causes, Prevention, and Correction Methods
Optimize Gating with Multi-Point Injection
The first line of defense is mold design. Transitioning to a multi-point gating system (typically using a 3-plate mold) is highly recommended. For large flat parts requiring injection molding machines of 24 oz (or equivalent tonnage) and above, aim for at least 4 gate points.
This balanced filling pattern significantly reduces the degree of molecular orientation and minimizes the gap between shrinkage rates in different directions, resulting in a much flatter final part. > Learn more about gate design best practices: The Advantages of Using Small Gates in Injection Molding: A Complete Guide
Increase Mold Temperature for Uniform Cooling
Rapid cooling is a primary culprit for warpage. By properly increasing the mold temperature, you can slow down the cooling rate and reduce thermal gradients that cause deformation.
For example, when molding ABS, maintain the mold temperature at 60°C (140°F) or higher. This not only prevents warpage caused by rapid quenching but also helps relax the molecular orientation within the polymer matrix.
Maximize Packing Pressure and Hold Time
Arguably the most critical processing parameter is packing pressure and hold time. Increasing the injection/packing pressure and significantly extending the hold time forces more material into the cavity to compensate for volumetric shrinkage.
As a standard industry practice, extending the hold time by 10 to 15 seconds is a highly effective method to increase part dimensions, reduce overall shrinkage, and dramatically improve flatness. > Full parameter tuning reference: 사출 성형 파라미터 조정 가이드
Post-Mold Jigging and Thermal Fixturing
If the first three measures do not yield the desired flatness, post-mold fixturing (jigging) is your final solution. While effective, this technique requires precision and practice.
The key is to eject the part early while it is still at an elevated temperature (it should still be quite hot to the touch). Immediately place the part into a custom-designed fixture on a workbench to lock in its shape.
⚠️ Critical Considerations for Jigging
- Fixture Design: The jig must be precisely engineered to match the target geometry.
- Springback Compensation: Plastic exhibits elastic recovery (springback) as it cools. You must design the fixture to over-correct the part.
- Cooling Time: Springback typically stabilizes after about 12 hours.
- Ejection Temperature: The lower the ejection temperature, the greater the springback. Always calculate the required "over-bend" amount based on your specific material and cooling parameters.
Quick Reference: Warpage Reduction Strategies
To help you troubleshoot on the production floor, here is a quick summary of our recommended solutions:
| Strategy | Key Action | Primary Benefit |
|---|---|---|
| Multi-Point Gating | Use 4+ gates for large parts | Reduces molecular orientation & uneven shrinkage |
| 금형 온도 | Keep ABS molds ≥ 60°C | Prevents thermal shock & relaxes polymer chains |
| Packing Parameters | Increase pressure & hold time (+10-15s) | Compensates for volumetric shrinkage |
| Thermal Fixturing | Jig part while hot; over-correct | Forces dimensional stability during cooling |
Final Thoughts
Achieving perfect flatness in large injection-molded parts requires a holistic approach, combining smart mold design, precise thermal management, optimized processing parameters, and careful post-mold handling.
Have you encountered severe warpage in your flat panel projects? What techniques worked best for you? Share your experiences in the form below!
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean