 한국어



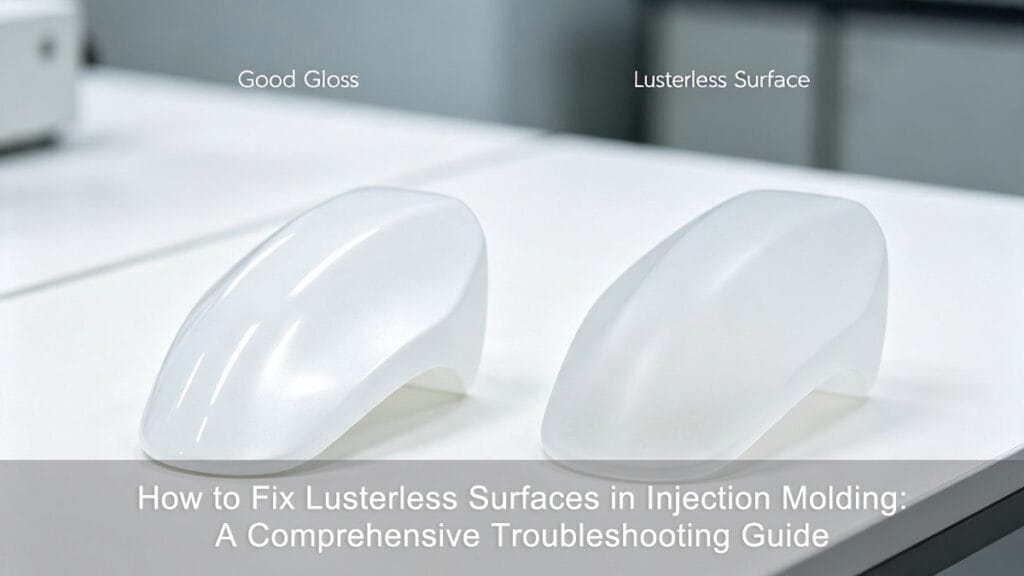
Introduction: What is a Lusterless Surface?
In 사출 성형, surface finish is often the first indicator of part quality. A lusterless surface defect manifests as a hazy, matte, or uneven finish lacking brilliance. For transparent components, this defect also results in reduced optical clarity.
Because the plastic part's surface is essentially a negative replica of the mold cavity, lusterless issues can stem from a wide variety of factors. In this guide, we will break down the three primary culprits—Mold Issues, Processing Parameters, and Raw Materials—and provide actionable solutions to restore that perfect, glossy finish.
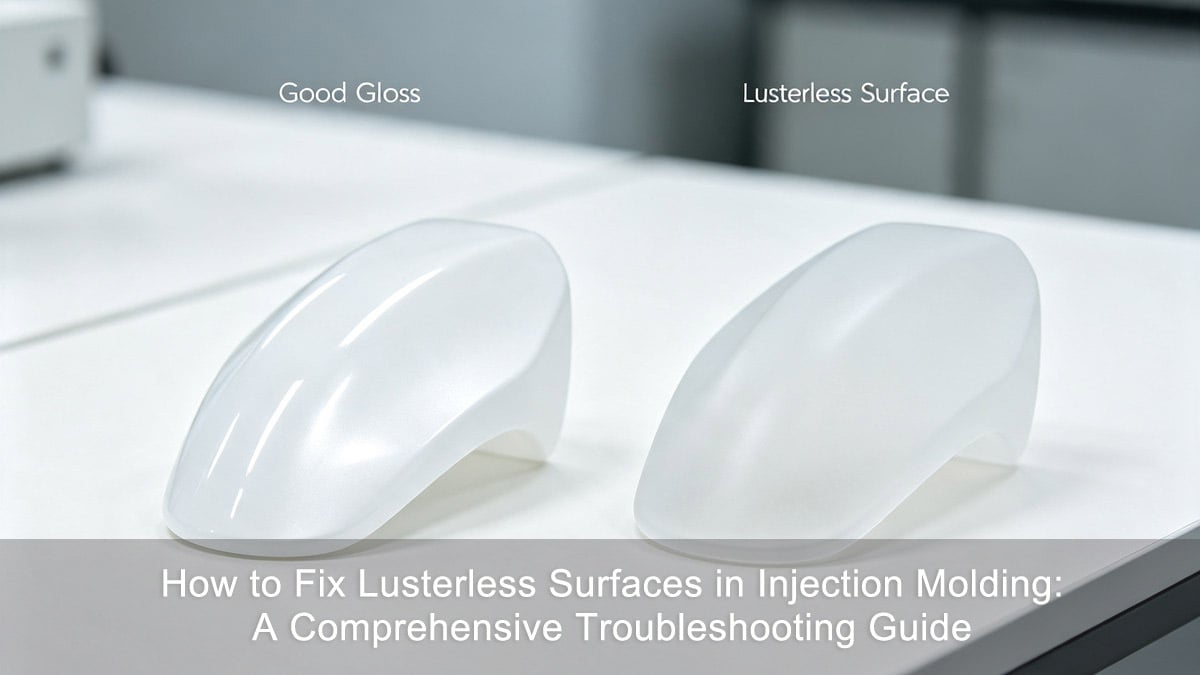
1. Mold-Related Causes & Solutions
Since the mold cavity directly dictates the part's surface, any imperfection will be faithfully reproduced on the plastic, leading to a lusterless appearance.
Cavity Surface Quality
Scratches, corrosion, or micro-pores on the mold surface will transfer directly to the part. Additionally, excessive or improperly chosen mold release agents, oil, or moisture can leave a dull, lusterless film.
- 솔루션: Maintain high cavity polish standards (e.g., mirror polishing or chrome plating). Keep the mold impeccably clean and use mold release agents sparingly and correctly.
Mold Temperature Control
Mold temperature plays a massive role in surface replication. If the mold is too cold, the melt solidifies instantly upon contact, failing to capture the mold's fine details and resulting in a lusterless surface. Conversely, excessively high temperatures can also cause darkening.
- 솔루션: Optimize mold temperature. For most engineering plastics (excluding PS, ABS, and AS), temperatures above 100°C (212°F) improve gloss. Using warm water in the cooling circuit helps transfer heat rapidly without extending cycle times, while also reducing residual stress. As covered in our in-depth guide to injection molding surface defects like dark spots and gloss inconsistencies, mold temperature imbalance is one of the most overlooked gloss killers.
Mold Design Flaws
Poor gating, inadequate venting, abrupt wall thickness changes, or insufficient draft angles can cause turbulent flow, leading to lusterless surfaces.
- 솔루션: Ensure smooth transitions (use radii), optimize gate sizing, and verify proper venting to prevent gas traps. You can follow our draft angle & wall thickness design guidelines to eliminate flow turbulence at the design stage.
2. Processing Parameter Adjustments
Even with a perfect mold, incorrect machine settings can ruin the surface finish and cause lusterless defects.
Key Processing Variables
- Injection Speed & Pressure: Too fast or too slow speeds, low injection pressure, or insufficient holding pressure can cause incomplete surface replication.
- Temperature: Low barrel or nozzle temperatures lead to poor plasticization.
- Fillers: In fiber-reinforced plastics, poor dispersion or random orientation can create a matte, lusterless appearance.
Targeted Fixes for Specific Defects
| Defect Symptom | Probable Cause | Recommended Solution |
|---|---|---|
| Dark spots near gate or wall transitions | High shear stress / Turbulent flow | Reduce injection speed; enlarge gate area; add radius transitions. |
| Milky white haze on surface | 과도한 사출 속도 | Lower the injection speed to reduce shear heating. Our article on high-gloss surface haze troubleshooting explains haze formation mechanisms in detail. |
| Visible fibers / Lusterless texture | Poor filler dispersion | Switch to better-flowing resin or use a screw with higher mixing capability. |
Master core machine settings with our complete injection molding parameters tuning guide to fine-tune speed, pressure and temperature for consistent gloss results.
3. Raw Material & Resin Issues
Sometimes, the problem is in the hopper. Material inconsistencies are a frequent but easily overlooked cause of lusterless defects.
Moisture and Volatiles
Excess moisture or volatiles in the resin will condense between the melt and the mold wall during injection, causing a lusterless finish.
- 솔루션: Always pre-dry hygroscopic materials according to manufacturer specifications. This issue is especially critical for transparent resins, as outlined in our transparent plastic injection molding troubleshooting guide.
Thermal Degradation
If the material or colorant degrades due to excessive heat, the resulting chemical changes will dull the surface.
- 솔루션: Use high-temperature-resistant resins and colorants; verify barrel temperatures.
Crystalline Resin Challenges
Crystalline plastics cool unevenly, which can lead to a rough, lusterless surface. Thick-walled parts are especially prone to this if cooling is insufficient.
- 솔루션: Precisely control mold and processing temperatures. For thick parts, use a secondary cold-press cooling fixture immediately after ejection to ensure uniform crystallization.
Material Contamination
Recycled materials, incompatible resins, or uneven pellet sizes disrupt uniform plasticization.
- 솔루션: Limit regrind ratios, sieve out irregular pellets, and ensure strict material segregation.
빠른 문제 해결 체크리스트
Before diving into complex mold modifications, run through this quick diagnostic table:
| 카테고리 | Checkpoint | Action Item |
|---|---|---|
| 곰팡이 | Cavity Cleanliness | Wipe down mold; check release agent usage. |
| 곰팡이 | Mold Temp | Increase temp gradually (use warm water if needed). |
| 프로세스 | 사출 속도 | Adjust up/down to test surface replication. |
| 프로세스 | Holding Pressure | Increase to ensure surface packing. |
| 재료 | Moisture Content | Dry resin thoroughly before processing. |
| 재료 | Regrind Ratio | Reduce recycled material percentage. |
결론
Fixing lusterless surfaces in injection molding requires a systematic approach. Always start by inspecting the mold and verifying your drying processes before tweaking complex machine parameters. By understanding the interplay between mold design, processing conditions, and raw material properties, you can consistently produce high-gloss, premium-quality plastic parts.
Have you encountered other tricky surface finish defects in injection molding? Share your experiences and solutions in the form below!
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean