 한국어



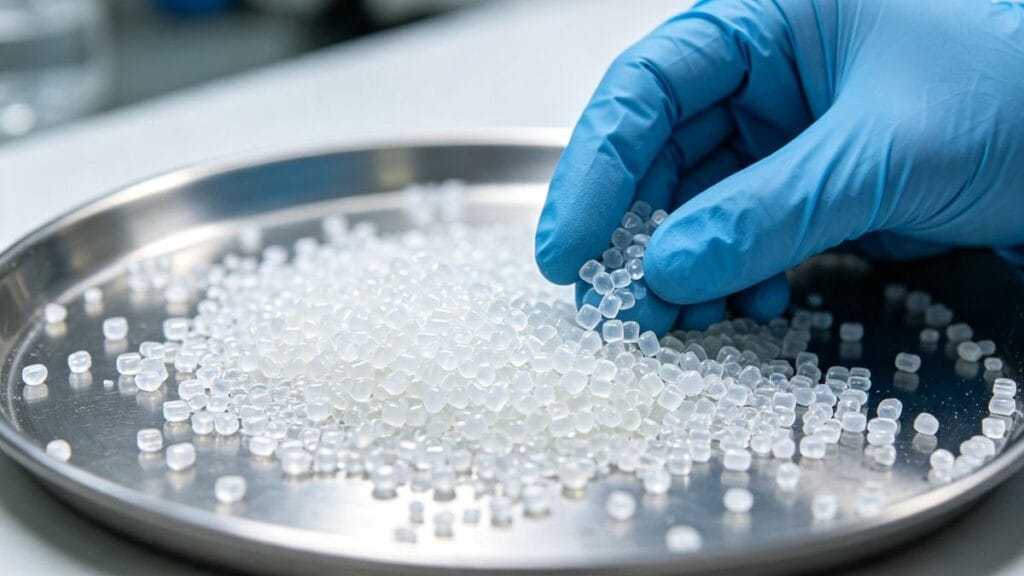
Incomplete injection molding (often referred to as "short shots") is one of the most common challenges in plastic manufacturing. Fortunately, it is usually highly solvable. When standard process adjustments fail to yield results, the root cause often lies in mold design or equipment limitations.
In this guide, we will break down the four primary causes of incomplete molding and provide actionable solutions to get your production back on track.
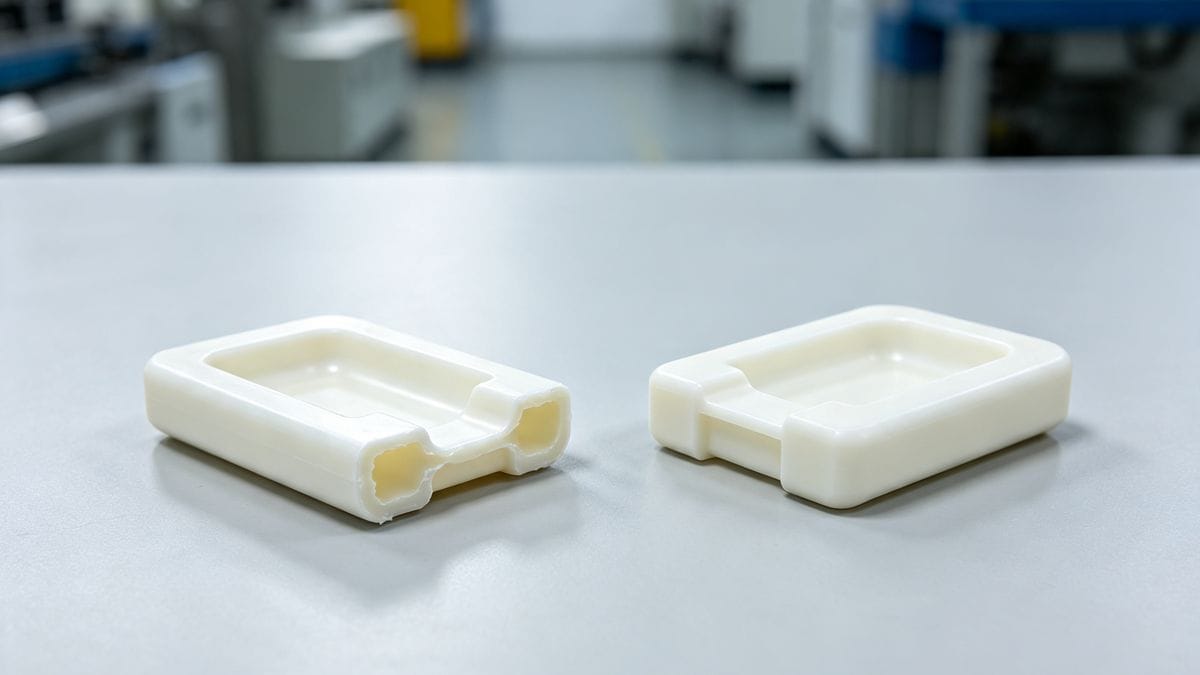
Equipment Issues: Is Your Machine the Problem?
Even the best mold cannot compensate for equipment limitations. Check these critical machine parameters first:
- Insufficient Plasticizing Capacity: If the part weight exceeds the machine’s maximum injection capacity, material supply will be inadequate. Even if the part is near the limit, the plastic may not have enough residence time in the barrel to melt properly. 솔루션: Upgrade to a larger injection molding machine, especially for materials with narrow melting ranges like Nylon 66.
- Inaccurate Temperature Readings: A faulty thermocouple or aging heater band can cause the actual melt temperature to be much lower than the display indicates. Always verify your heating elements.
- Nozzle Sizing & Blockages: A nozzle that is too small restricts flow and cools the material, while one that is too large reduces injection pressure. Additionally, check for carbonized deposits, poor alignment with the sprue bushing, or mechanical issues causing nozzle deflection.
- Material Bridging: Plastic pellets can prematurely melt and clump together in the feed throat due to excessive heat, poor drying, or excess lubricant. This creates a "bridge" that blocks material flow. 솔루션: Clear the blockage and adjust the feed throat cooling.
- Cold Slugs & Drool: If the nozzle temperature is too high or backpressure is excessive, molten plastic can drool into the cold sprue, solidify, and block the gate. Reduce nozzle temperature and backpressure to prevent this.
- Cycle Time Too Short: Rapid cycles may not allow sufficient heating time for the plastic, especially during voltage fluctuations. Adjust the screw recovery time to ensure proper pre-heating without affecting the injection phase.
Mold Design: Optimizing Flow & Venting
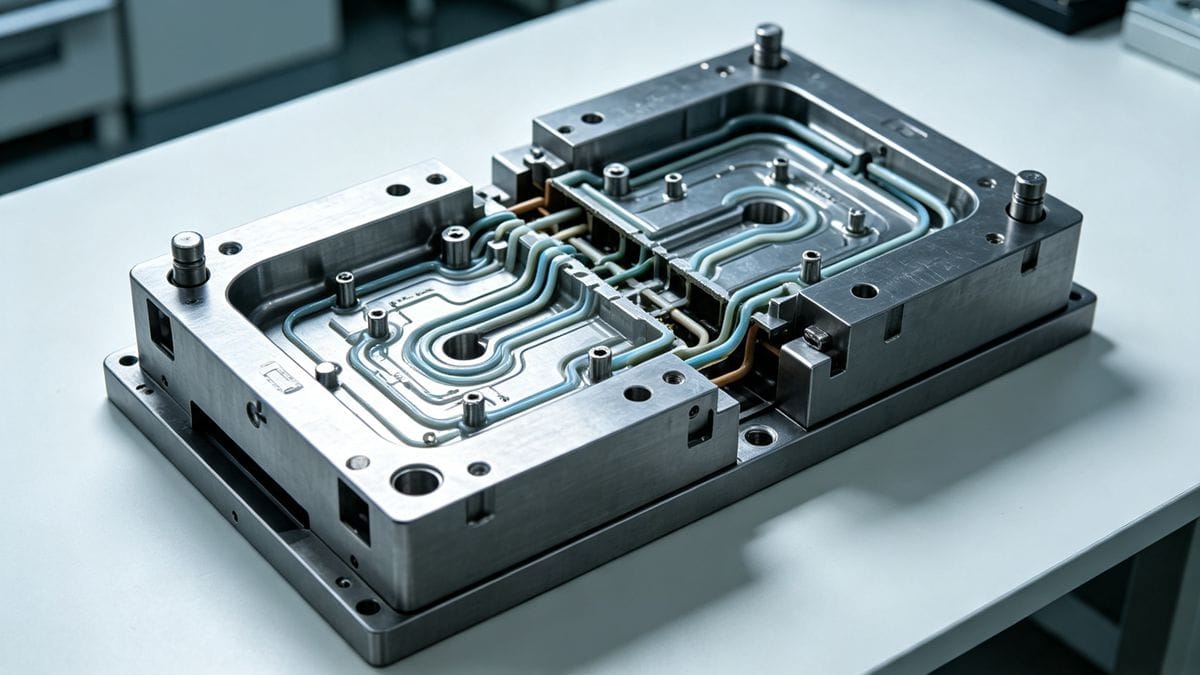
When process tweaks aren't enough, the mold itself may need modification.
- Runner System Defects: Runners that are too small, thin, or long create excessive flow resistance. Opt for circular runners and ensure they are free of debris or sharp corners. For multi-cavity molds, balance the runner and gate sizes to ensure equal filling pressure across all cavities.
- Poor Mold Design: Complex geometries, excessive wall thickness transitions, or inadequate gate placement can hinder flow. Consider adding secondary runners or adjusting wall thickness in thin sections.
- Inadequate Venting: Trapped air is a leading cause of short shots, especially in deep ribs, corners, and thin-walled areas. Add effective vent channels, relocate gates to allow air escape, or use vented ejector pins/inserts.
- Unbalanced Multi-Cavity Molds: If some cavities fill while others don't, consider reducing the number of active cavities to guarantee part quality.
Processing Parameters: Fine-Tuning the Cycle
Your processing window might need a strategic adjustment. Here is a quick reference table for common parameter-related defects:
| Processing Issue | Root Cause | Recommended Solution |
|---|---|---|
| Inaccurate Shot Size | Poor metering, low backpressure, or excessive cushion. | Increase shot size, raise backpressure, and reduce cushion volume. |
| Low Injection Pressure | High melt viscosity or low barrel temperature. | Increase injection pressure and extend injection time. |
| Slow Injection Speed | Complex geometry or high-viscosity materials (e.g., toughened ABS). | Switch to high-speed injection to overcome flow resistance. |
| Low Melt Temperature | Insufficient barrel/nozzle heating or heat loss to mold. | Increase barrel zones temperature; use external heater if needed. |
You can learn more about how pressure, speed and temperature settings directly lead to underfill defects in our guide: Mastering Injection Molding Speed Segmentation: Rules & Optimization
Raw Material: The Importance of Flowability
Never underestimate the impact of your raw material. Recycled or regrind plastics often exhibit increased viscosity due to oxidative degradation and molecular chain scission. This increases flow resistance and generates more gas, leading to pressure loss.
Pro Tip for Improving Flow: To enhance the flowability of difficult materials, consider adding external lubricants such as stearic acid or silicone oil (viscosity 300–600 cm²/s). Lubricants not only improve melt flow but also increase process stability and reduce gas-related resistance in the cavity.
Final Thoughts
Troubleshooting incomplete injection molding requires a systematic approach. Always start with the easiest fixes—verifying temperatures, checking for blockages, and adjusting processing parameters—before moving on to costly mold modifications.
For a full checklist covering all mainstream molding flaws including short shots, check out: 16 Common Injection Molding Defects: Root Causes & Solutions
If you want more targeted mold and process fixes specifically for underfill defects, read our dedicated troubleshooting article: 12 Proven Solutions to Fix Injection Molding Short Shots
Have you encountered stubborn short shots in your production? Share your experiences or questions in the form below!
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean