 한국어



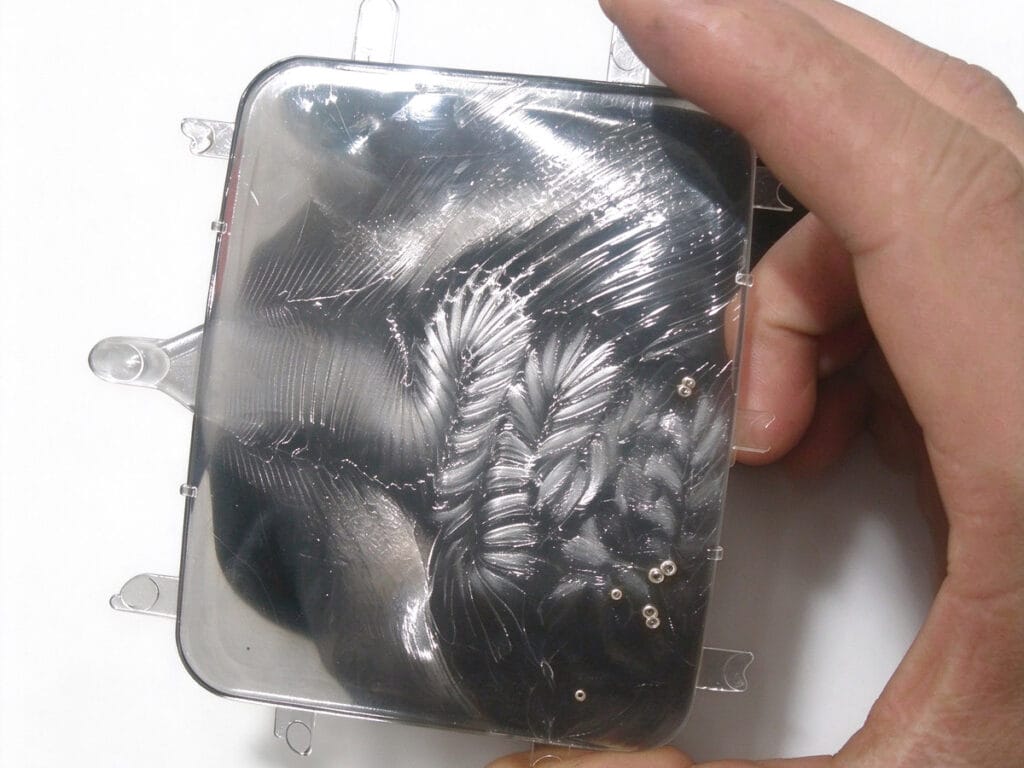
사출 성형 시 게이트 부근에 생기는 흐릿하고 얼룩진 자국을 해결하는 방법
Cloudy, mottled marks appearing near the gate are among the most common and frustrating 사출 성형 표면 결함. They ruin part aesthetics, increase scrap rates, and often stall production while engineers chase the root cause. The good news is that these blemishes are highly preventable once you understand the two main failure mechanisms behind them: melt fracture 그리고 irregular pulsing flow.
In this guide, we break down why hazy, streaked zones form around the gate, how crystalline polymers make the problem worse, and step-by-step process and mold corrections that eliminate them. You'll also find structured troubleshooting tables, expert fixes, and an FAQ to get your production back to glossy, uniform surfaces faster.
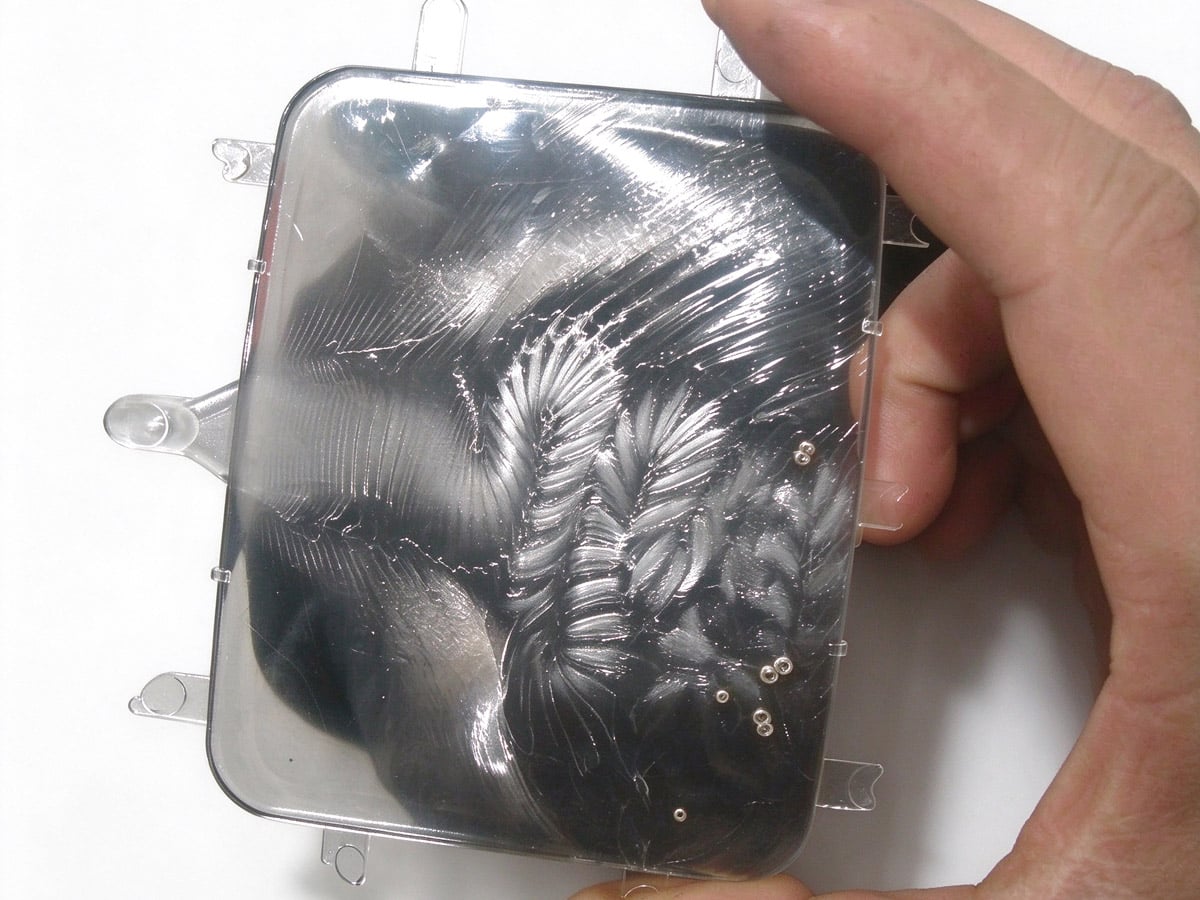
What Causes Cloudy, Mottled Marks Near the Gate?
Two distinct mechanisms produce these surface blemishes, and each needs a different fix. Misdiagnosing them—treating melt fracture as a flow issue, or vice versa—wastes cycles and can worsen the defect.
1. Melt Fracture (Frozen Skin Rupture)
When molten polymer enters the cavity, it first solidifies into a thin surface skin (shell) against the mold wall. If the incoming melt then pushes against this fragile skin during filling, the skin can tear, shift, or wrinkle. The result is scratches, wrinkles, and alternating light/dark bands across the part surface.
This is especially visible on low-melt-index LDPE parts, where you can see clear repeating dark-and-light zones. The bands usually start a short distance from the gate and can cover the entire surface—thin-wall parts are the most susceptible, because the skin layer is thinner and the filling pressure is proportionally higher before the cavity is completely filled.
How to fix it: The most reliable cure is to slow down both the cooling of the melt during filling and the formation rate of the skin layer. Practically, this means raising the mold temperature 또는 raising the local temperature at the fracture zone. For localized heating, small cartridge (tubular) electric heaters installed near the gate and at the fracture site work well.
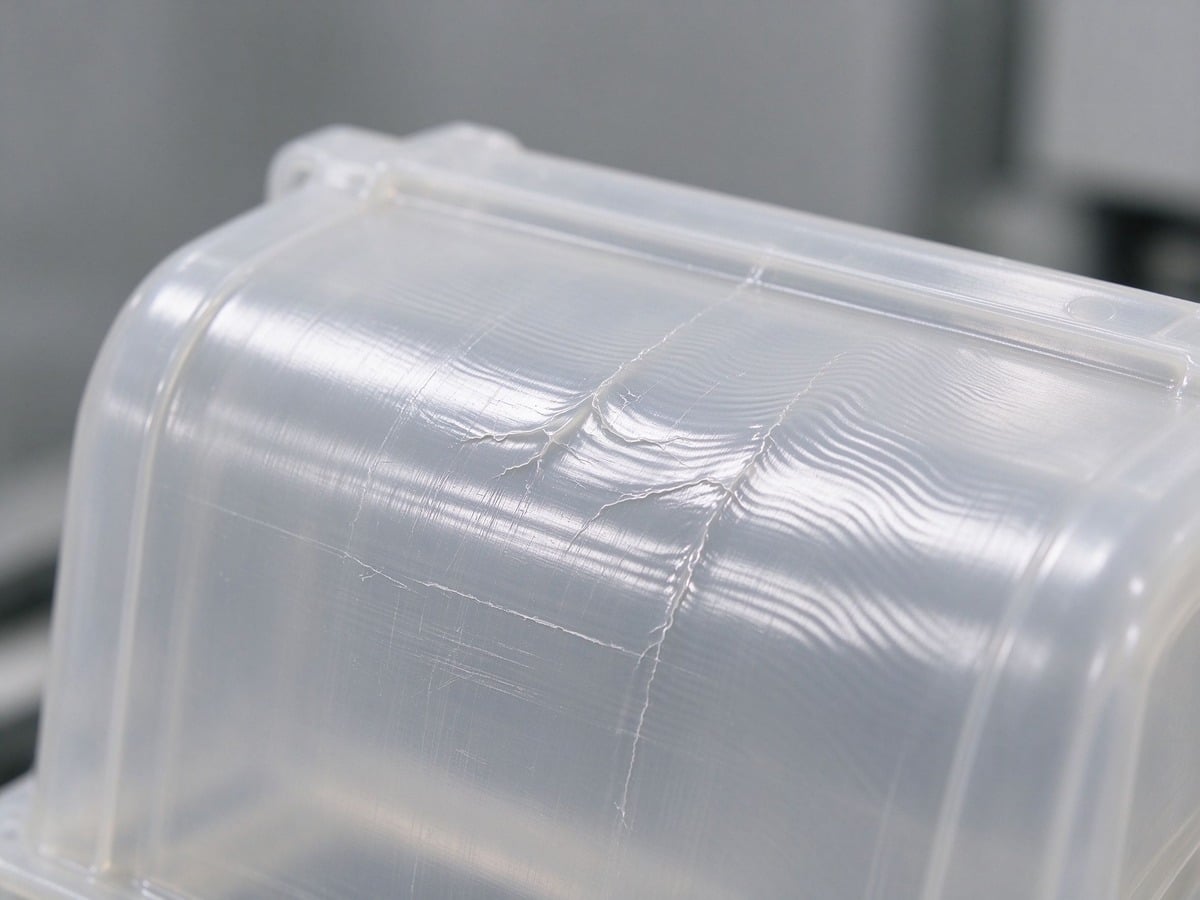
2. Irregular Pulsing Flow in the Cavity
The second mechanism is about flow behavior. How the melt flows depends on its rheological (flow) properties and on the gate cross-section, which sets the shear rate at the mold entrance. When the gate is very small and the injection rate is very high, the melt enters the cavity as a thin, bent, jet-like stream. If this stream cools quickly, it fails to fuse cleanly with the irregularly moving melt that follows—producing cloudiness and mottled marks right around the gate.
Sometimes a small amount of cold material (cold slug) travels along the cavity wall, which pushes the cloudy zone to a spot farther away from the gate.
How to fix it: Improve fusion by letting the melt flow more uniformly—larger gates, fan gates, better venting, and slower injection speeds all help (detailed in the tables below).
Why Crystalline Polymers Are Harder to Fix
Crystalline (semi-crystalline) resins such as PA, POM, PP, PBT and PET make this defect noticeably harder to eliminate. Why? Because these materials:
Have a high melting temperature and a narrow processing window;
Solidify faster than amorphous polymers once cooling begins;
Form irregular flow at sudden wall-thickness changes and abrupt flow-direction turns, giving the disturbed melt very little time to fuse with the rest of the cavity fill.
As a result, cloudy and mottled zones form more readily and are more stubborn to remove.
Crystalline vs. Amorphous Polymers: Key Differences
| Property | Crystalline (e.g., PA, POM, PP, PBT) | Amorphous (e.g., ABS, PC, PS) |
|---|---|---|
| Melting temperature | High, sharp melting point | Gradual softening, no sharp melt point |
| Solidification speed | Fast | Slower |
| Processing temperature window | Narrow | Broad |
| Flow irregularity risk | High (rapid cooling + short fusion time) | Lower |
| Difficulty fixing cloudy/mottled marks | Harder | Easier |
Step-by-Step Fixes for Cloudy, Mottled Marks Near the Gate
To remove these defects, work through the process parameters first, then the 금형 설계, and finally the material/additive side.
A. Process Parameter Adjustments
| Adjustment | How It Helps |
|---|---|
| Raise mold temperature | Slows skin-layer formation and melt cooling, improving fusion |
| Raise barrel (cylinder) temperature | Lowers melt viscosity, promotes smoother, more uniform flow |
| Raise nozzle temperature | Prevents early solidification and cold slug formation at the nozzle |
| Reduce screw forward (injection) speed | Lowers shear rate, reduces jetting and irregular pulsing flow |
B. Mold Design Adjustments
| Adjustment | How It Helps |
|---|---|
| Enlarge the gate cross-section | Lowers shear rate at the entrance; reduces jetting and irregular flow |
| Prefer a fan gate | Spreads melt across a wider front, reducing turbulence and improving fusion |
| For tunnel (submarine) gates: enlarge the top/small-end size | A too-small top leaves residual cold material at the gate that disrupts filling and worsens irregular flow |
| Improve mold venting (gas venting) | Trapped air disrupts uniform flow; proper venting stabilizes the melt front |
C. Material & Additive Adjustments
| Adjustment | How It Helps |
|---|---|
| Reduce lubricant dosage | Excessive lubricant disrupts melt homogeneity and surface appearance |
| Choose the right lubricant grade/type | A compatible grade keeps flow stable without surface streaking |
빠른 문제 해결 체크리스트
Confirm whether the defect is melt fracture (wrinkles, scratches, alternating bands) or irregular flow (cloudy, mottled, jetting).
Process first: raise mold, barrel, and nozzle temperatures; slow the injection speed.
Then mold: enlarge the gate, switch to a fan gate, fix tunnel-gate top size, improve venting.
Material last: reduce and re-select the lubricant.
Document the before/after parameters so the fix is repeatable.
관련 읽기
How to Fix Lusterless Surfaces in Injection Molding – A Comprehensive Troubleshooting Guide
How Injection Molding Process Parameters Affect Product Performance – Complete Guide 2026
자주 묻는 질문
Q1: What do cloudy, mottled marks near the gate look like?
Q2: What is melt fracture in injection molding?
Q3: Why is the defect worse with crystalline polymers?
Q4: What is the fastest way to remove cloudiness near the gate?
Q5: Should I use a fan gate to prevent this defect?
Q6: Can mold venting really fix a surface cloudiness problem?
*
Need a custom injection molding partner that ships defect-free parts? *[Contact our team](https://ideal-pro.com/contact/)* for DFM review, tooling, and low-to-mid volume production.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean