 한국어



Heat-resistant ABS[^1] is a powerhouse material in the engineering plastics industry. However, achieving high-quality results requires a precise approach to processing.
Standard ABS often lacks the thermal performance required for demanding applications. To bridge this gap, manufacturers have developed heat-resistant ABS resins by copolymerizing with $alpha$-methylstyrene 그리고 N-phenylmaleimide. These modifications raise the Heat Deflection Temperature (HDT)[^2] to between 90°C and 120°C.
⚠️ The Core Challenge: Internal Stress
While these additives improve heat resistance, the molecular structure—containing rigid benzene rings and N-phenyl groups—increases steric hindrance. This slows down the relaxation speed of the molecular chains, making the material prone to high internal stress.
If not managed correctly, this leads to common defects such as:
- Stress cracking
- Stress whitening
- Brittleness
Therefore, the golden rule of processing heat-resistant ABS is: Minimize internal stress[^3].
Here are the 5 critical factors you must control to ensure successful injection molding.
Product and Mold Design
Design is the foundation. Poor design creates stress traps that no amount of process tuning can fix.
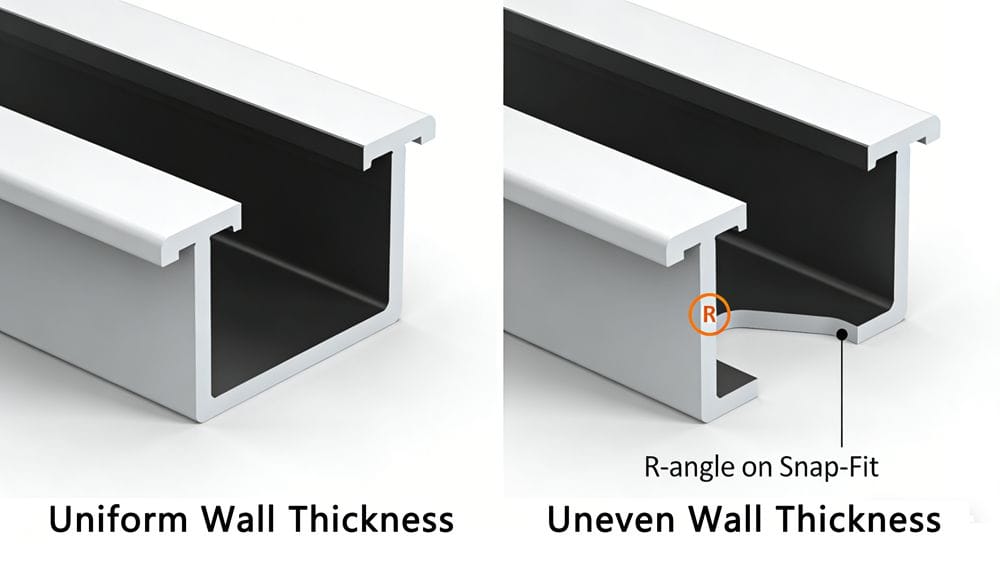
- 균일한 벽 두께: Wall thickness variations should be controlled within 25%. Drastic changes cause uneven cooling and stress concentration.
- Bosses and Ribs: For columns (bosses) with weak strength, add fillets (R-angles) at the roots or reinforce with ribs to prevent fracture.
- Snap-Fit Design: The root of a snap-fit must have a fillet. The ratio of the R-angle to wall thickness should be > 0.3. While a larger ratio reduces stress, balance it against the risk of surface sink marks.
- 냉각 채널: Design cooling water channels to ensure uniform cooling. Uneven cooling leads to uneven shrinkage, which generates internal stress.
> ? Pro Tip: Avoid sharp corners at all costs. Sharp corners are the number one initiator of stress cracks in heat-resistant materials.
Material Drying
Heat-resistant ABS is hygroscopic. During storage and transport, it absorbs moisture from the air (typically 0.2% ~ 0.4%).
If this moisture is not removed, you will face surface defects like silver streaks 그리고 water splashes. Because heat-resistant ABS requires higher drying temperatures than standard ABS, strict adherence to drying protocols is essential.
Recommended Drying Parameters:
- Target Moisture Content: < 0.05% (Ideally 0.3 ratio. | | 건조 | Dry at 80-95°C for 3-4 hours. Target <0.05% moisture. | | Temp | Use mid-to-high melt temps to lower viscosity. | | Pressure | Use lower holding pressure to minimize stress. | | Mold Temp | Keep mold at 60-80°C to prevent brittleness. |
[^1]: Explore the advantages of heat-resistant ABS, a crucial material for high-performance engineering applications. [^2]: Understand the significance of HDT in evaluating the thermal performance of materials. [^3]: Find out how to effectively manage internal stress in heat-resistant ABS to ensure quality.
자주 묻는 질문
⚠️ The Core Challenge: Internal Stress
While these additives improve heat resistance, the molecular structure—containing rigid benzene rings and N-phenyl groups—increases steric hindrance. This slows down the relaxation speed of the molecular chains, making the material prone to high internal stress.
If not managed correctly, this leads to common defects such as: Stress cracking Stress whitening Brittleness
Therefore, the golden rule of processing heat-resistant ABS is: Minimize [internal stress](https://kingstarmold.com/causes-of-internal-stress-in-plastic-parts-and-cracking-in-pc-and-abs/)[^3].
Product and Mold Design
Design is the foundation. Poor design creates stress traps that no amount of process tuning can fix.
균일한 벽 두께: Wall thickness variations should be controlled within 25%. Drastic changes cause uneven cooling and stress concentration. Bosses and Ribs: For columns (bosses) with weak strength, add fillets (R-angles) at the roots or reinforce with ribs to prevent fracture. Snap-Fit Design: The root of a snap-fit must have a fillet. The ratio of the R-angle to wall thickness should be > 0.3. While a larger ratio reduces stress, balance it against the risk of surface sink marks. 냉각 채널: Design cooling water channels to ensure uniform cooling. Uneven cooling leads to uneven shrinkage, which generates internal stress.
> ? Pro Tip: Avoid sharp corners at all costs. Sharp corners are the number one initiator of stress cracks in heat-resistant materials.
Material Drying
Heat-resistant ABS is hygroscopic. During storage and transport, it absorbs moisture from the air (typically 0.2% ~ 0.4%).
If this moisture is not removed, you will face surface defects like silver streaks 그리고 water splashes. Because heat-resistant ABS requires higher drying temperatures than standard ABS, strict adherence to drying protocols is essential.
Recommended Drying Parameters: Target Moisture Content: < 0.05% (Ideally < 0.02%) Drying Temperature: 80°C – 95°C Drying Time: 3 – 4 hours
Melt Temperature Settings
Temperature control is about balancing flow with material stability.
You should set the temperature to ensure full plasticization of the resin. Generally, aim for the middle-to-upper range of the supplier's recommended temperature window.
Why higher temperatures help: Increasing the melt temperature significantly reduces the viscosity of the heat-resistant ABS. This improves flow length and ensures the cavity is filled completely without excessive injection pressure, which can also induce stress.
Holding Pressure and Time
For heat-resistant ABS, the holding phase is a balancing act between preventing sink marks and creating stress.
Holding Pressure: Increasing pressure packs the molecules tighter, increasing density and reducing shrinkage. However, excessive pressure drastically increases internal stress. Use the lowest pressure possible that still maintains part quality. Holding Time: This should be set based on the time it takes for the gate to freeze. - Too Long: Over-packing occurs, molecular gaps shrink too much, and stress rises. - Too Short: Sink marks appear, and dimensions become unstable.
Optimization Strategy: The ideal holding time is the shortest duration where the part weight no longer increases.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean