 日本語




Polybutylene Terephthalate (PBT) is a widely used engineering thermoplastic known for its excellent mechanical properties, chemical resistance, and electrical insulation. However, to achieve high-quality parts consistently, understanding its unique processing behavior is essential. Below, we detail PBT’s processing characteristics and recommended 射出成形[^1] conditions.
Processing Characteristics of PBT
Low Hygroscopicity—but Moisture-Sensitive at High Temperatures
PBT absorbs relatively little moisture, yet residual water can cause hydrolysis during high-temperature processing, leading to molecular degradation, discoloration (darkening), and surface blemishes. Pre-drying is strongly recommended: typically 2–4 hours at 120°C (with desiccant dryer, dew point ≤ −40°C).Excellent Melt Flowability
PBT exhibits very low melt viscosity, enabling easy molding of thin-walled and complex geometries. However, this also increases the risk of flash (mold) そして drooling from the nozzle—requiring tight mold fit and proper nozzle shut-off design.Sharp Melting Transition
PBT has a distinct melting point (~223–225°C). Once above this threshold, melt flow increases abruptly—so precise temperature control is critical to avoid uncontrolled flow or jetting.Narrow Processing Window, Fast Crystallization
PBT crystallizes rapidly upon cooling—even at ambient temperatures. Combined with its high flowability, this makes it ideal for high-speed injection molding, but demands precise control over cycle time and cooling.High & Anisotropic Shrinkage
PBT exhibits relatively large shrinkage (typically 1.5–2.5% for unfilled grades), and shrinkage differs significantly between flow and transverse directions. This anisotropy must be accounted for in mold design to prevent warpage or dimensional inaccuracy.High Notch Sensitivity
PBT is extremely sensitive to sharp corners, edges, or notches, where stress concentration can drastically reduce load-bearing capacity and lead to brittle fracture under impact or static load.
✅ Design tip: Always use generous fillets (R ≥ 0.5 mm) at internal corners—especially in load-bearing areas.Elongation & Demolding Behavior
- Unfilled PBT has high elongation (~200%), allowing forced ejection of parts with minor undercuts or shallow recesses.
- Glass-fiber or mineral-filled grades show much lower elongation ( ? 注記: Always optimize parameters based on part geometry, wall thickness, and machine capability. Use DOE (Design of Experiments) for critical applications.
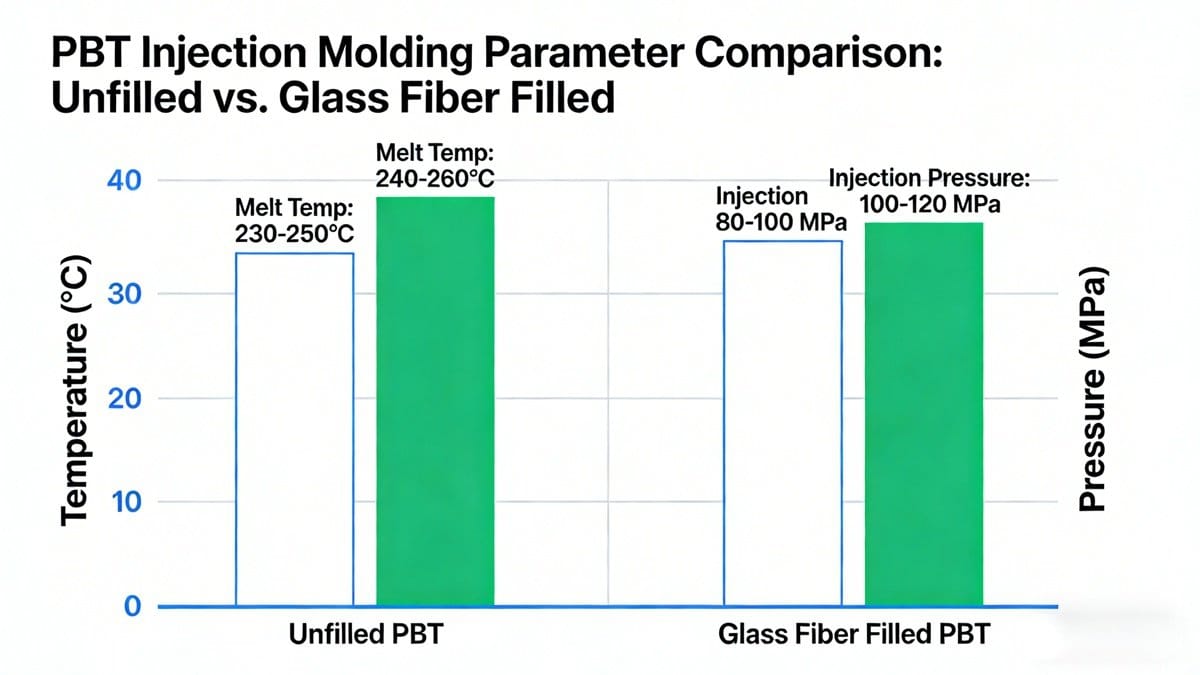
Final Takeaway
PBT is a high-performance polymer—but its narrow processing window, sensitivity to moisture, and anisotropic shrinkage demand careful attention to drying, temperature control, mold design, and gate strategy. When handled correctly, PBT delivers outstanding dimensional stability, strength, and surface quality.
[^1]: Explore this resource to gain insights into optimal injection molding techniques for PBT, ensuring high-quality production.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean