 日本語




射出成形金型
- Poor machining of the mold cavity—such as scratches, micro-pores, wear, and rough surfaces—will directly result in inferior gloss on the plastic parts. To solve this, carefully machine the mold to achieve a low surface roughness, and polish or chrome-plate the cavity if necessary.
- Oil, water stains, or excessive release agent on the cavity surface can make the plastic surface dull and non-glossy. Clean away oil and water stains promptly, and use release agent in moderation.
- An insufficient draft angle causes difficult demolding or excessive stress during ejection, impairing surface gloss. Increase the draft angle accordingly.
- Poor mold venting traps excess gas inside the cavity, leading to poor gloss. Inspect and improve the mold venting system.
- An excessively small or abruptly changing cross-section of the gate or runner creates high shear force and turbulent flow, reducing surface gloss. Properly enlarge the cross-sectional area of the gate and runner.
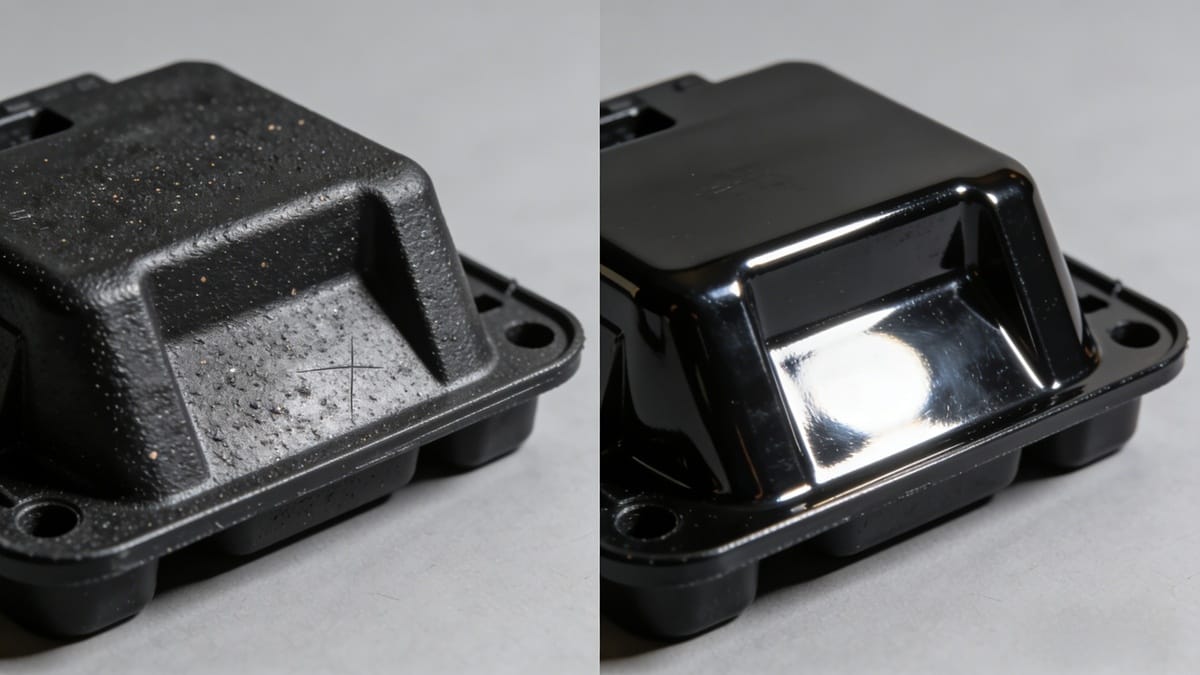
射出成形[^1] Process
- Low injection speed results in a non-dense surface and poor gloss. Appropriately increase the injection speed[^2].
- Insufficient cooling for thick-walled parts causes a fuzzy, dull surface. Optimize the 冷却システム[^3].
- Insufficient holding pressure and short holding time lead to low density and poor gloss. Raise the holding pressure and extend the holding time.
- Low melt temperature reduces fluidity and causes poor gloss. Increase the melt temperature properly.
- For parts made of crystalline resins such as PE, PP, POM, uneven cooling causes poor gloss. Improve the cooling system for uniform cooling.
- Excessively high injection speed combined with an undersized gate creates a dull area near the gate. Reduce the injection speed and enlarge the gate cross-section.
結論
In summary, achieving superior gloss for injection molded products[^4] requires a balance between precise mold surface finishing and optimized injection molding parameters. By addressing issues like poor venting, insufficient cooling, and incorrect injection speed, manufacturers can significantly enhance product aesthetics and quality. This guide serves as a practical reference for solving common gloss problems in production.
[^1]: Explore this resource to discover essential techniques and insights that can enhance your injection molding process and product quality. [^2]: Learning about injection speed's effects can help optimize your processes for better product aesthetics. [^3]: Optimizing your cooling system is crucial for achieving uniform quality and gloss in injection molded products. [^4]: Explore this resource to discover expert techniques that enhance the quality and aesthetics of injection molded products.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean