 English



Resin grade guide · 34 profiles
Injection Molding Plastic Materials
Every resin recommendation below is developed under our ISO 9001 quality management system and tied to official supplier TDS data. Selecting the right plastic — shrinkage, melt temperature, chemical resistance or heat deflection — is the foundation for a successful tool design and production campaign.
Plastic Materials Guide: Browse Commodity, Engineering and High-Temperature Resin Families
Semi-crystalline and amorphous resins have different shrinkage behaviour, hold different temperature limits and ask for different mould steels. Filter by family, then open the grade guide for the process window and steel recommendation.
Commodity resins
8 grades COMMODITY RESINSABS Injection Molding GuideCommodity thermoplasticABS is the default choice for rigid, impact-resistant housings that need a clean moulded finish and a forgiving process window. It is replaced when the part lives outdoors, meets solvents, or has to hold a dimension above roughly 80 °C.Read guide
 COMMODITY RESINSPP Injection Molding GuidePolypropylene - commodityPolypropylene is the highest-volume commodity resin — low cost, low density, good chemical resistance and a forgiving process window make it the default choice for packaging, caps, containers and automotive interior trim.Read guide
 COMMODITY RESINSPS Injection Molding GuidePolystyrene - commodityPolystyrene is a rigid, clear commodity resin used for packaging, disposable cutlery and toy components. It is brittle, limited by poor impact resistance, and has been displaced in many applications by ABS and PP.Read guide
 COMMODITY RESINSPE Injection Molding GuidePolyethylene - commodityPolyethylene is a semi-crystalline commodity resin used for flexible packaging, caps, bottles and small containers. Low cost, good chemical resistance and very low density -but it shrinks more and holds less precision than its styrenic cousins.Read guide
 COMMODITY RESINSPVC Injection Molding GuidePolyvinyl chloride - corrosive commodityPVC is a corrosive commodity resin that releases hydrogen chloride when moulded, requiring a stainless steel tool. Used for pipes, window profiles and a range of consumer products -but the corrosion risk is the first thing to settle before cutting the block.Read guide
 COMMODITY RESINSPMMA Injection Molding GuideAcrylic - clear commodityPMMA (acrylic) is a clear, glossy commodity resin used for optical components, displays and automotive trim. Excellent clarity and polishability, but prone to stress cracking and limited impact resistance.Read guide
 COMMODITY RESINSPET Injection Molding GuidePolyethylene terephthalate - commodityPET is a semi-crystalline commodity resin best known for bottles and food packaging. High clarity when properly dried, recyclable and moderate temperature resistance -but it demands careful drying and a warmer mould than ABS or PP.Read guide
 COMMODITY RESINSSAN Injection Molding GuideStyrene-acrylonitrile - commoditySAN is a clear styrene-acrylonitrile copolymer used for rigid transparent containers, cookware and consumer electronics housings. Better chemical resistance than PS, comparable clarity and a similar process window.Read guide
Engineering resins
10 grades ENGINEERING RESIPC Injection Molding GuideAmorphous engineering resinPolycarbonate is chosen when a part has to stay stiff and clear at temperatures that would soften ABS, or take an impact that would crack it. It is replaced when the part needs chemical resistance, a low-cost housing, or a mould that can run cold.Read guide
 ENGINEERING RESIPA+GF Injection Molding GuideGlass-fibre reinforced engineering resinA 30 % glass-filled polyamide is chosen when a part has to be stiff, strong and heat-resistant at a metal-adjacent cost. It is replaced when the part needs a cosmetic surface, tight isotropic tolerance, or a tool that will not wear.Read guide
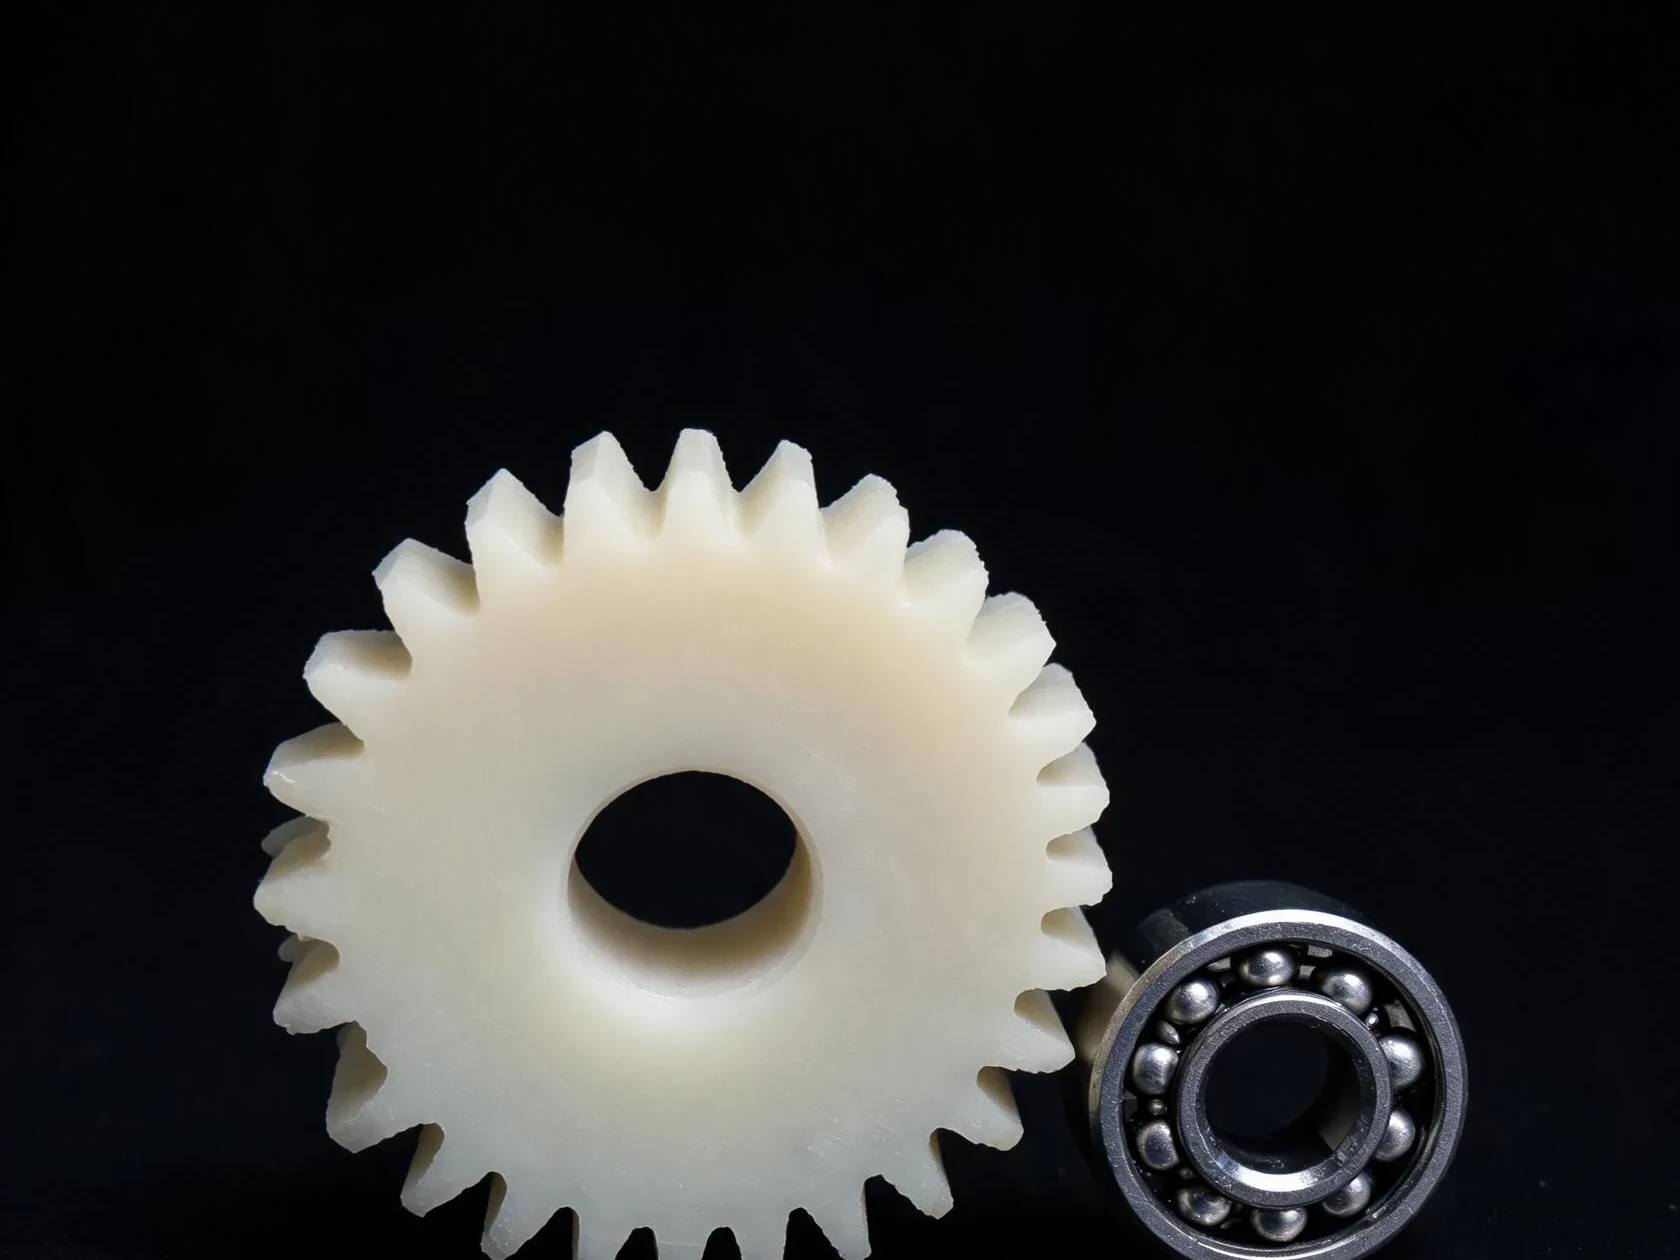 ENGINEERING RESIPA / Nylon Injection Molding GuidePolyamide / Nylon - engineeringPA (nylon) is a semi-crystalline engineering resin chosen for load-bearing parts that also need temperature and chemical resistance. Available unfilled, glass-filled and mineral-filled -the filler changes the properties more than the grade letter does.Read guide
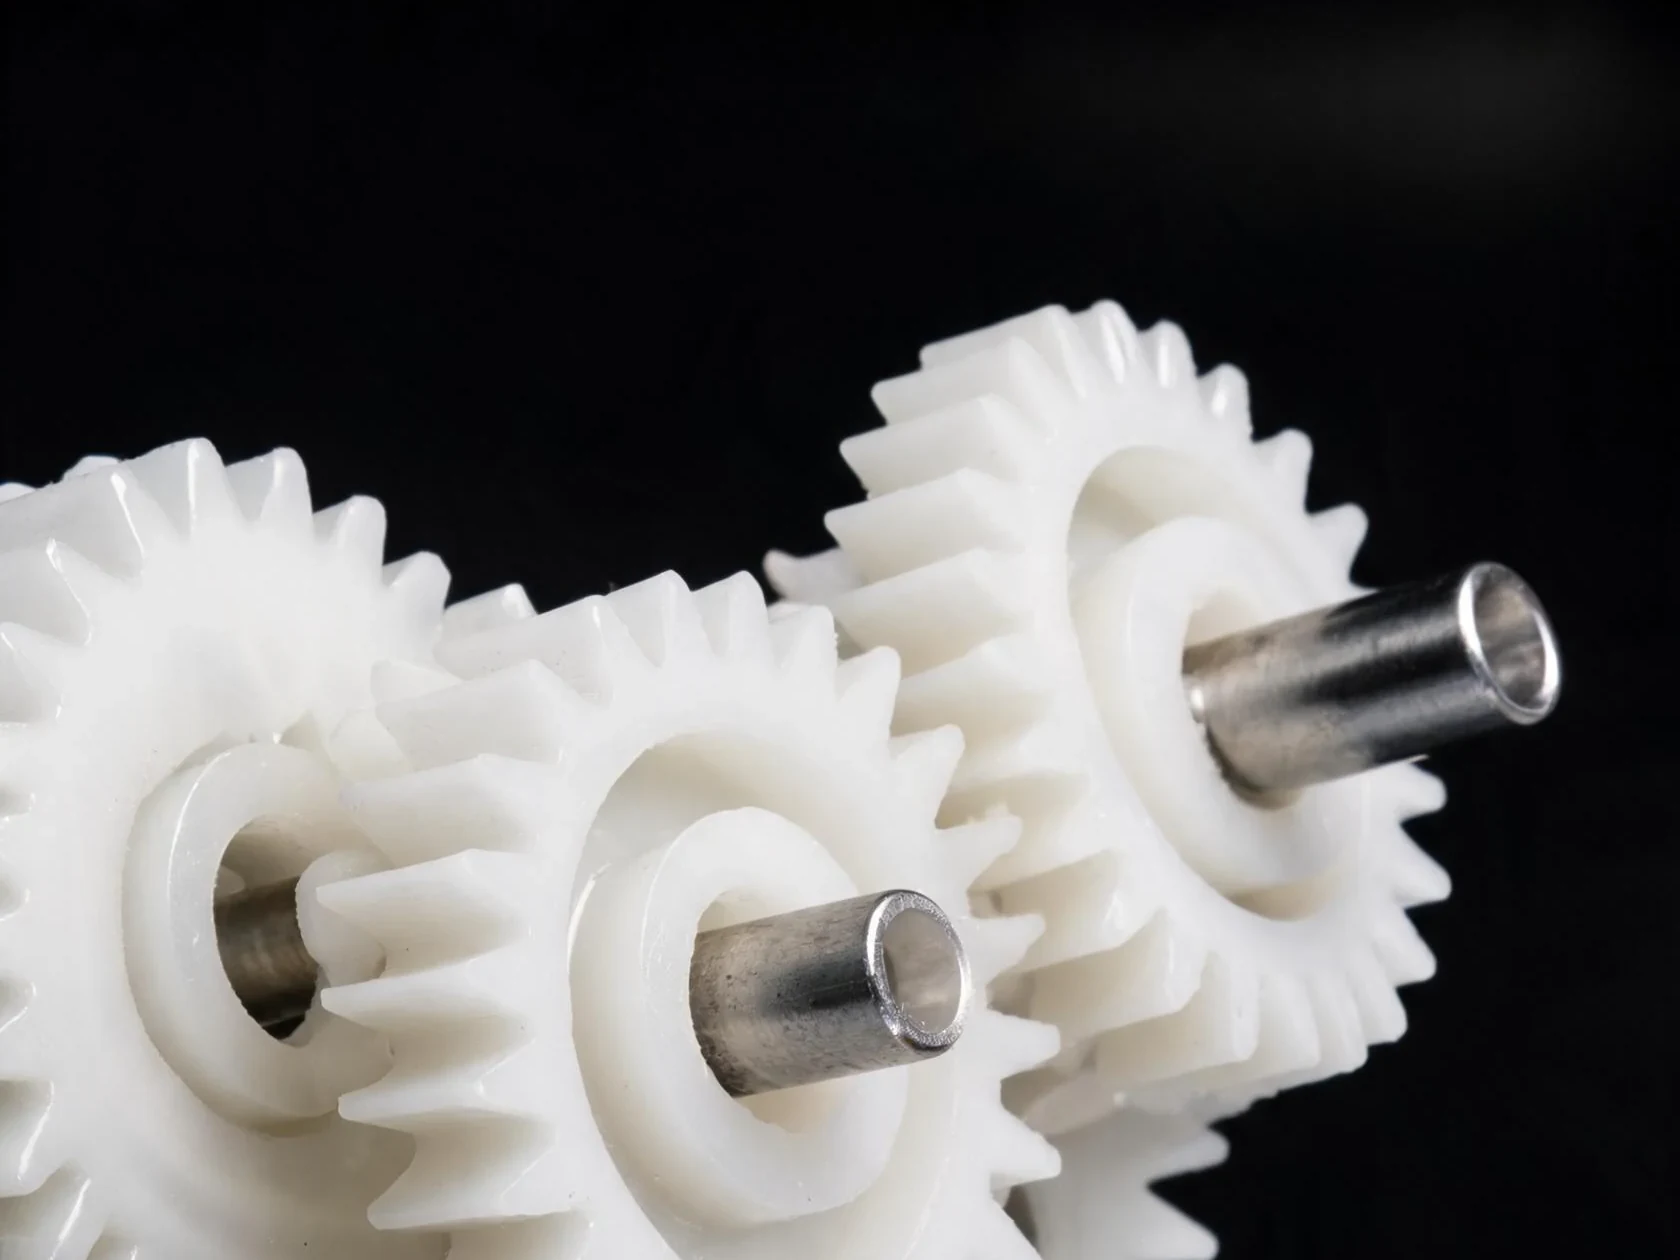 ENGINEERING RESIPOM Injection Molding GuidePolyacetal - engineeringPOM (acetal) is a hard, low-friction engineering resin used for gears, bearings and wear-sensitive components that must run dry or with minimal lubrication. Stiffer than PA, lower shrinkage than PEEK, and far more forgiving than PA with fillers.Read guide
 ENGINEERING RESIPBT Injection Molding GuidePolybutylene terephthalate - engineeringPBT is a semi-crystalline engineering resin that resembles PET but moulds faster and crystallises more reliably. Common in electrical connectors, automotive components and cosmetic housings where a good balance of heat resistance and processability matters.Read guide
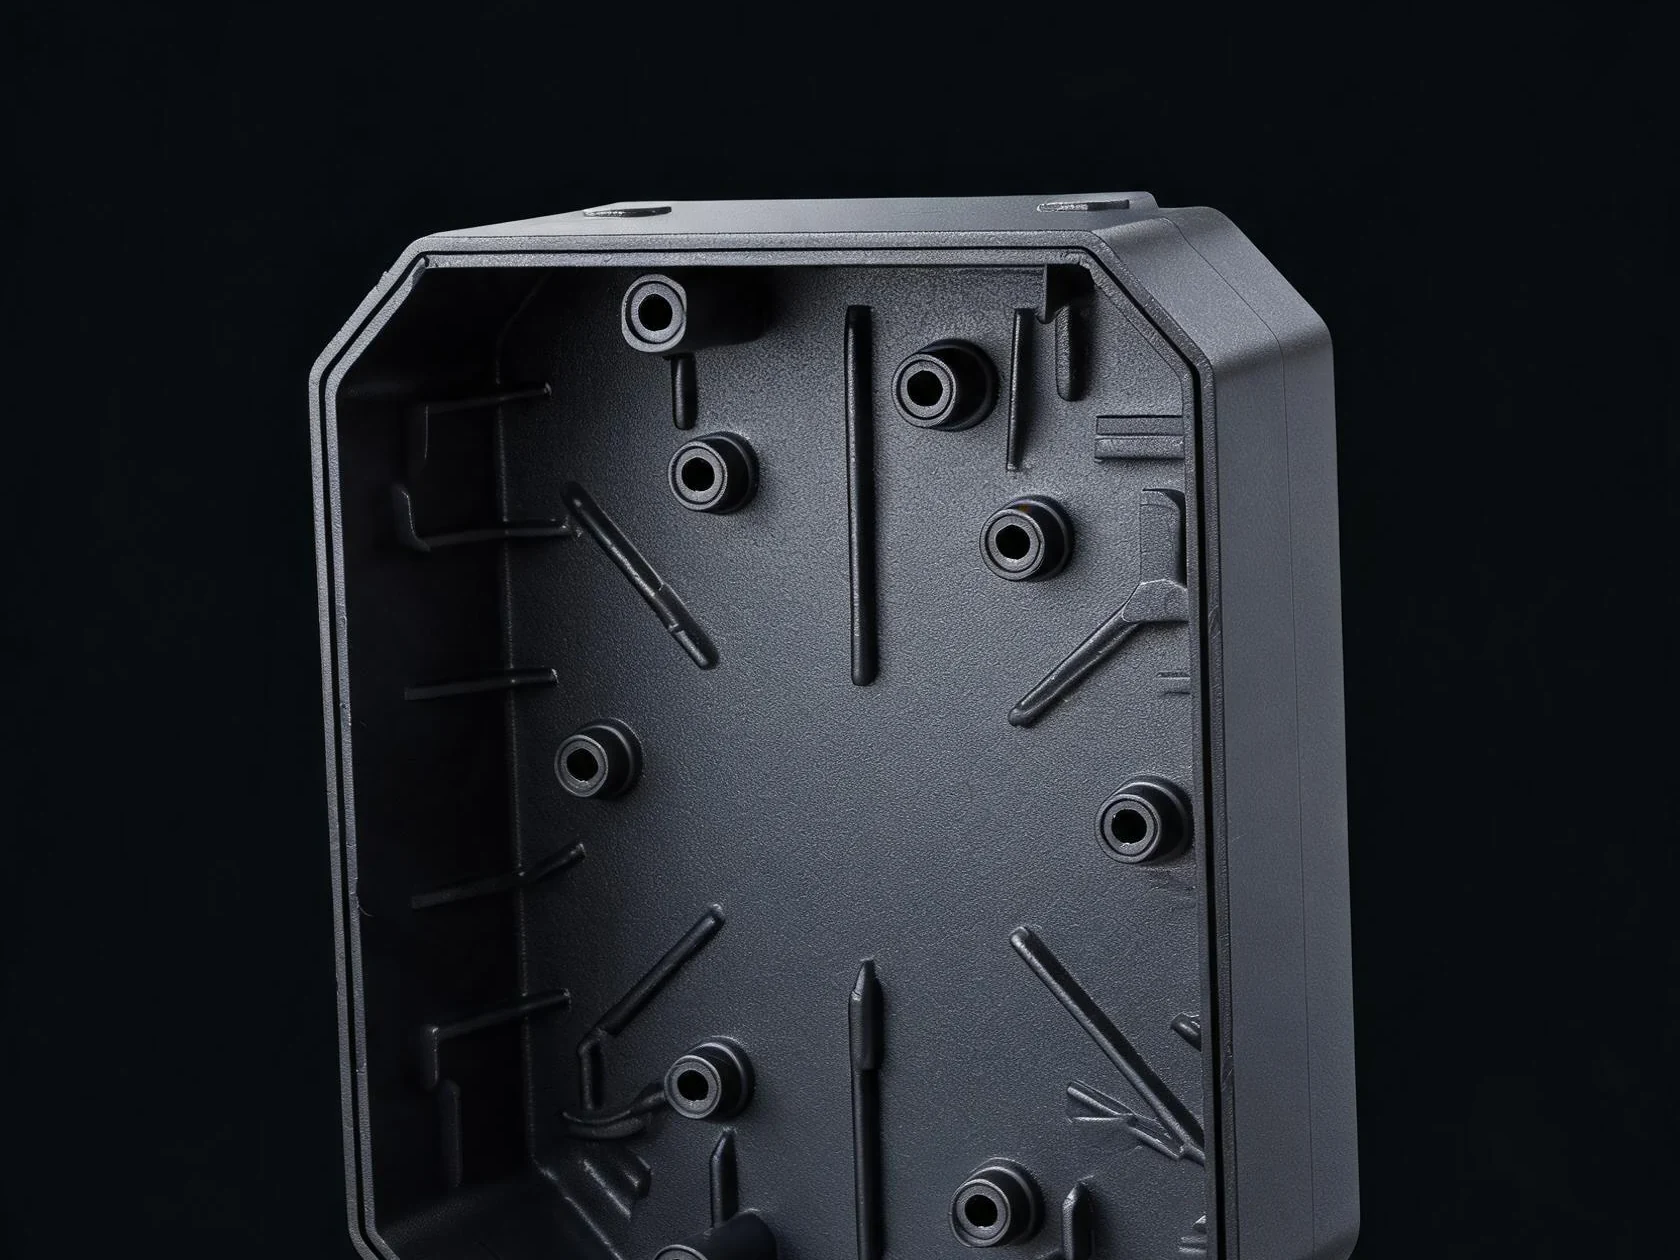 ENGINEERING RESIPC/ABS Injection Molding GuidePolycarbonate-ABS blend - engineeringPC/ABS is an amorphous copolymer blend that sits between ABS and PC in cost and performance -better heat and impact resistance than ABS, easier to process and less notch-sensitive than PC. The default blend for consumer electronics housings.Read guide
 ENGINEERING RESIPPO / PPE Injection Molding GuidePolyphenylene oxide - engineeringPPO (often blended with PS for processability) is a high-heat amorphous engineering resin used for automotive electrical, appliance and aerospace components. The glass transition is above 200 °C, so heat resistance is excellent -but the material is hygroscopic and expensive.Read guide
 ENGINEERING RESITPU Injection Molding GuideThermoplastic polyurethane - engineeringTPU is a flexible engineering elastomer used for gaskets, soft-touch overmoulds and wear-resistant components. Can be either ester-based (better oil resistance) or ether-based (better hydrolysis resistance). The tool runs cooler than hard engineering plastics.Read guide
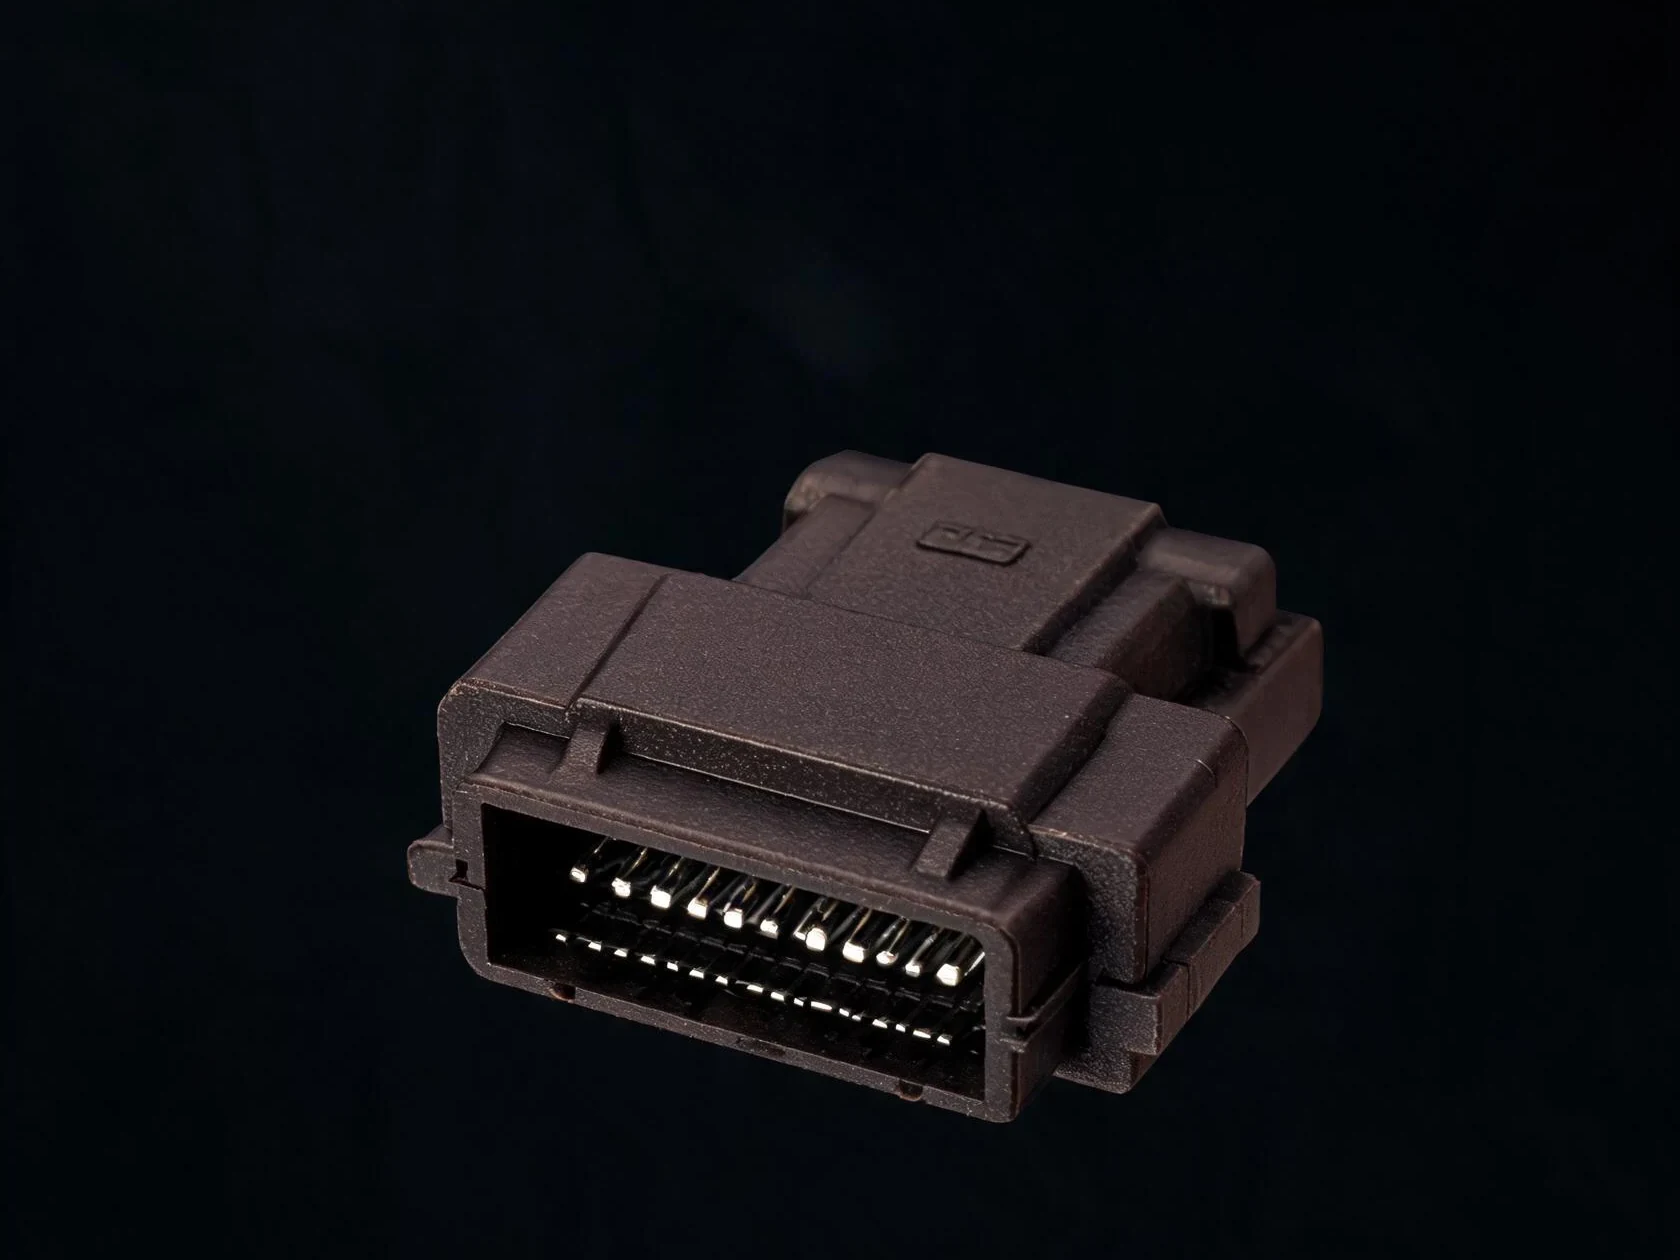 ENGINEERING RESIPPS Injection Molding GuidePolyphenylene sulfide - engineeringPPS is a high-temperature semi-crystalline engineering resin used for electrical components, under-hood automotive parts and applications that demand excellent chemical resistance and dimensional stability at sustained temperature.Read guide
 ENGINEERING RESIUHMWPE Injection Molding GuideUltra-high-molecular-weight PE - engineeringUHMWPE is an engineering thermoplastic with extraordinarily high wear resistance and low coefficient of friction, used for liners, chute plates and gears that slide against steel. It is difficult to mould due to melt viscosity, and typically runs on a specialised press.Read guide
High-temperature resins
7 grades HIGH-TEMPERATUREPEEK Injection Molding GuidePolyether ether ketone - high-tempPEEK is a premium high-temperature semi-crystalline thermoplastic used for aerospace, medical and oil-field components that must survive 200 °C+ service temperature, aggressive chemicals and high mechanical load. The tool needs a hot mould (170-90 °C) and the block is usually H13 or Invar to match the heat.Read guide
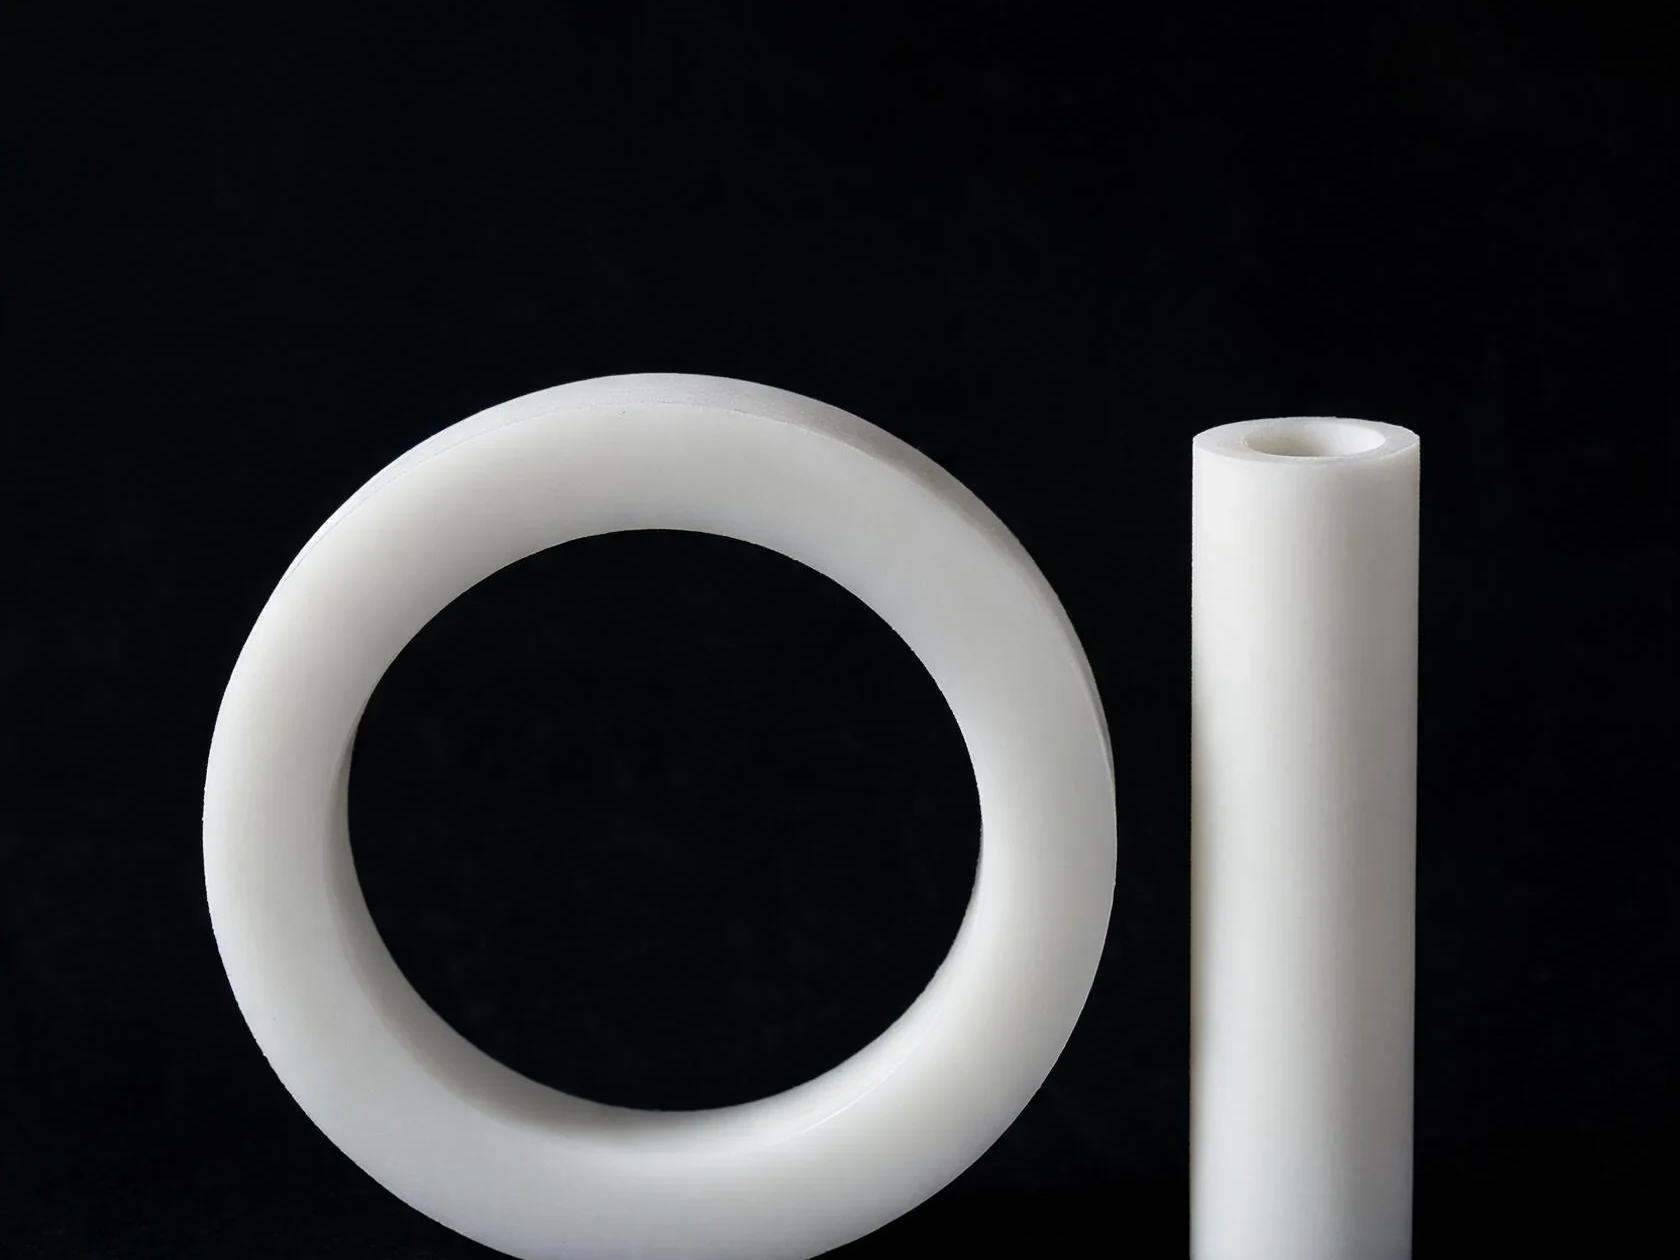 HIGH-TEMPERATUREPTFE Injection Molding GuidePolytetrafluoroethylene - high-tempPTFE (Teflon) is a high-temperature fluoropolymer with extraordinary chemical resistance and the lowest coefficient of friction of any solid. It is not injection mouldable -components are sintered from powder -so this guide exists for reference when PTFE components must be considered against mouldable alternatives.Read guide
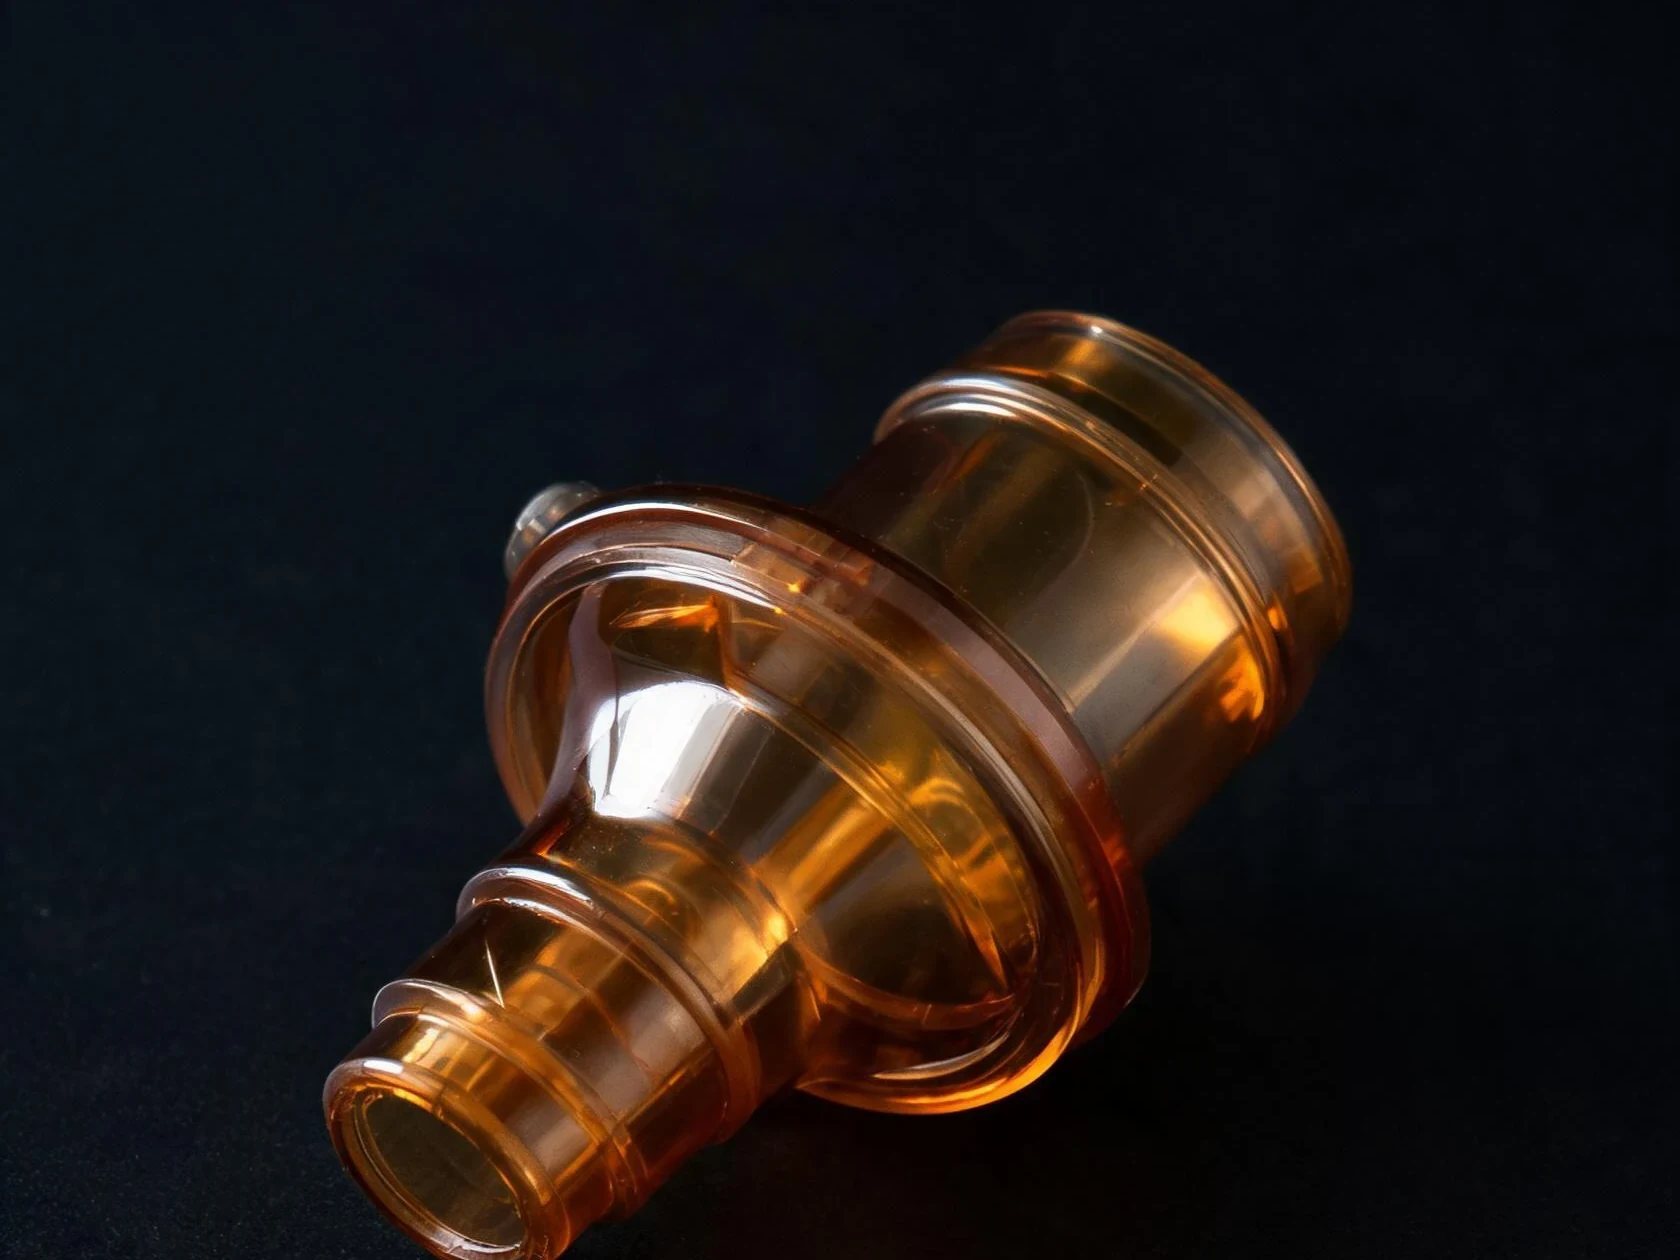 HIGH-TEMPERATUREPPSU Injection Molding GuidePolyphenylsulfone - high-tempPPSU is a clear, tough high-temperature amorphous engineering resin used for medical devices, baby bottles and food-service components that must survive repeated autoclaving or dishwasher cycles with no creep, discoloration or flavour change.Read guide
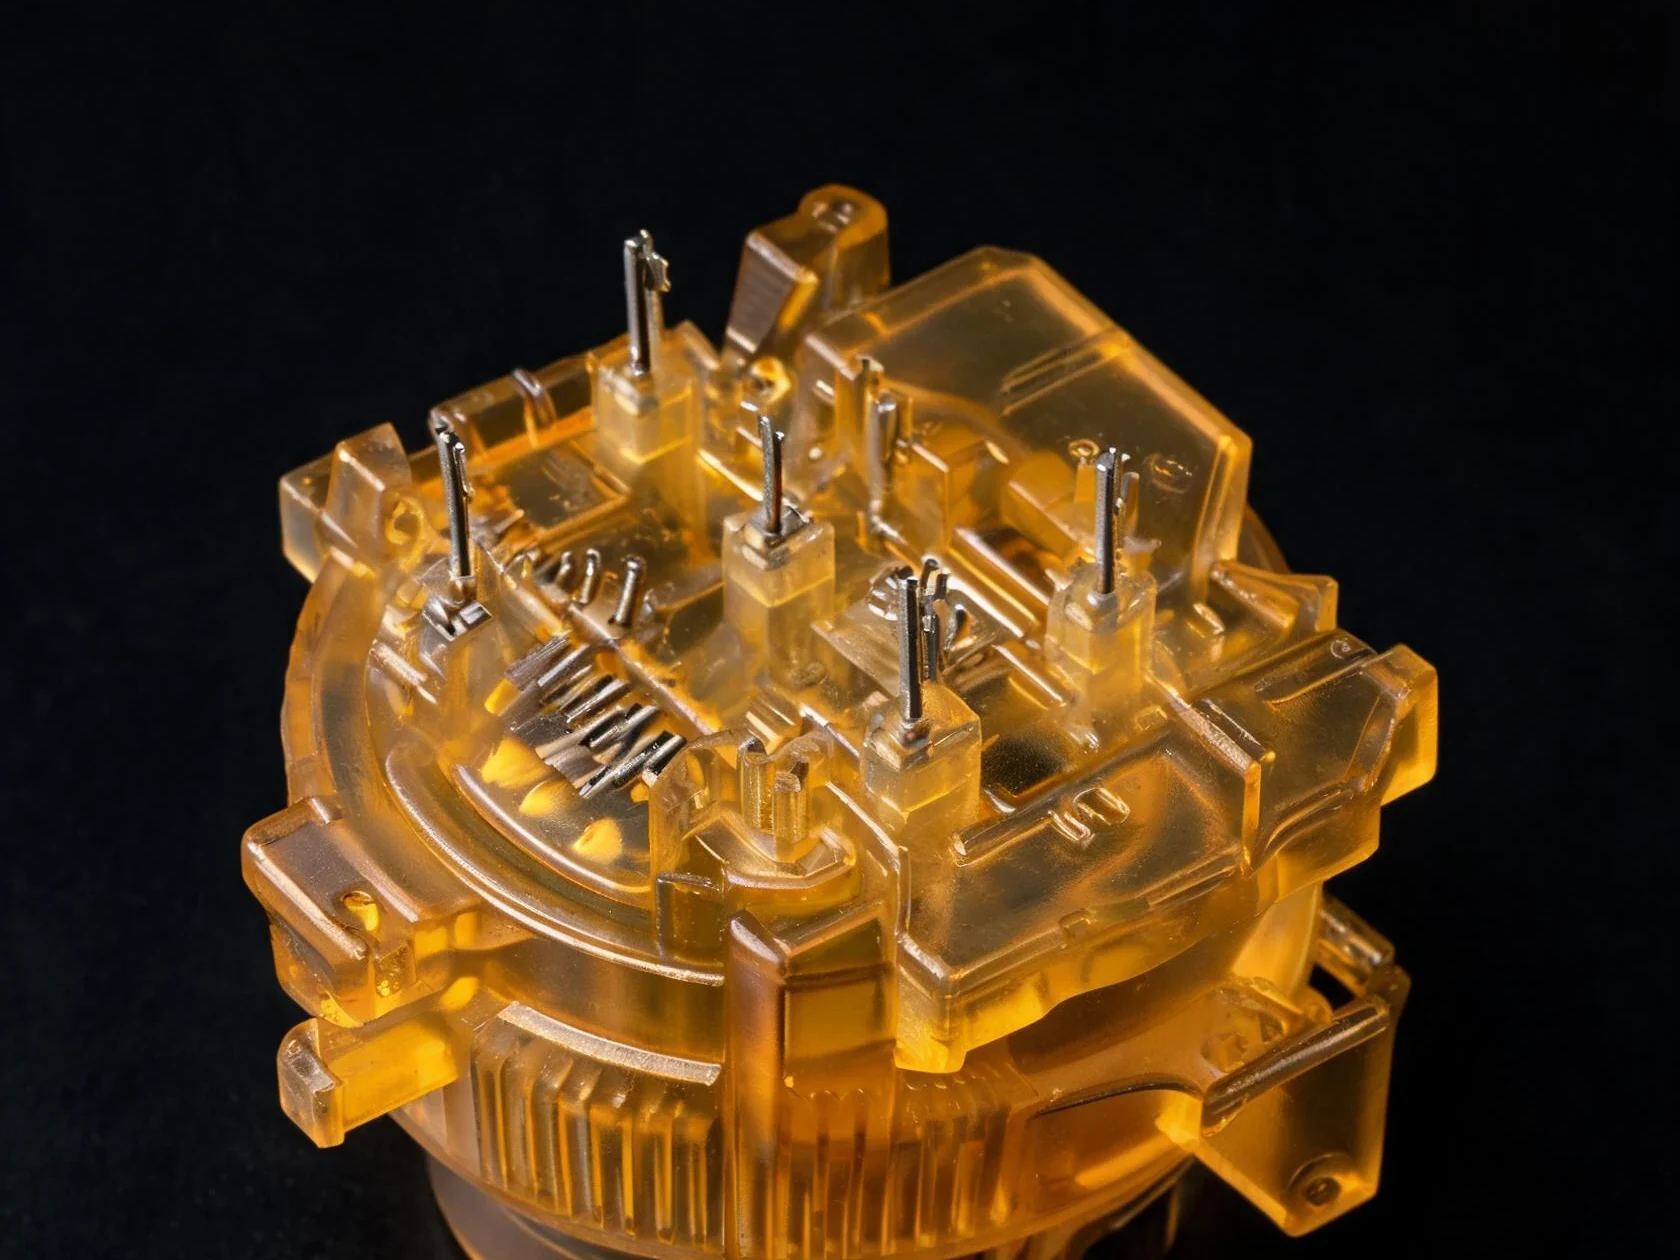 HIGH-TEMPERATUREPEI Injection Molding GuidePolyetherimide - high-tempPEI (Ultem) is a high-temperature amorphous engineering resin used for aerospace interior components, electrical connectors and high-performance automotive parts. Continuous service up to 170 °C, excellent flame resistance and good mechanical properties.Read guide
 HIGH-TEMPERATURELCP Injection Molding GuideLiquid crystal polymer - high-tempLCP is a high-temperature semi-crystalline polymer with self-reinforcing fibres that align under shear during injection moulding. Extremely low shrinkage (one of the lowest of any engineering plastic), excellent dimensional accuracy and electrical insulation.Read guide
 HIGH-TEMPERATUREPPA Injection Molding GuidePolyphthalamide - high-tempPPA is a high-temperature semi-crystalline polyamide family (often marketed as Amodel or Zytel HTN) used for automotive under-hood components, electrical connectors and components that must hold stiffness above 150 °C.Read guide
 HIGH-TEMPERATUREPA46 Injection Molding GuidePolyamide 46 - high-tempPA46 is a high-temperature polyamide (Stanyl) with faster crystallisation, higher HDT and better creep resistance than PA66, used for automotive timing gears, electrical connectors and thin-walled parts that need stiffness at sustained temperature.Read guide
Elastomers: TPE, TPU, LSR
4 grades ELASTOMERS: TPE,LSR Injection Molding GuideLiquid silicone rubber - elastomerLSR is a two-part liquid silicone rubber used for medical device seals, soft-touch grippers and food-contact components. It is moulded differently than thermoplastics -typically with a 2K injection system -and cures in the mould.Read guide
 ELASTOMERS: TPE,TPE Injection Molding GuideThermoplastic elastomer - elastomerTPE is a family of thermoplastic elastomers that behave like rubber but mould like thermoplastics. Common in soft-touch grips, seals and gaskets where the part can be recycled and has to run on standard equipment.Read guide
 ELASTOMERS: TPE,TPV Injection Molding GuideThermoplastic vulcanizate - elastomerTPV is a family of crosslinked thermoplastic elastomers (EPDM/polypropylene blends) used for automotive weather-stripping, seals and flexible components that need better heat and oil resistance than TPU.Read guide
 ELASTOMERS: TPE,TPS / SEBS Injection Molding GuideStyrenic thermoplastic elastomer - elastomerTPS (commonly SEBS, SBS) is a styrenic thermoplastic elastomer family used in consumer products, medical devices and automotive soft-touch components. Lower melt temperature than TPE, excellent clarity and good UV stability.Read guide
Bio-based & specialty
5 grades BIO-BASED & SPECPLA Injection Molding GuidePolylactic acid - bio-specialtyPLA is a bio-based, biodegradable thermoplastic made from corn starch or sugar cane. Low carbon footprint but lower heat resistance and mechanical performance than commodity or engineering plastics. Common in disposable packaging and consumer products with sustainability claims.Read guide
 BIO-BASED & SPECPBAT Injection Molding GuidePolybutylene adipate terephthalate - bio-specialtyPBAT is a biodegradable copolymer with good flexibility and film-forming properties, used in compostable bags, food packaging and soft disposable components. Blended with PLA to improve the mechanical properties of PLA in packaging applications.Read guide
 BIO-BASED & SPECPA11 Injection Molding GuidePolyamide 11 - bio-specialtyPA11 (Rilsan) is a bio-based polyamide made from castor oil. Excellent flexibility, good chemical resistance, lower density than PA6 or PA66, and used in automotive fuel lines, pneumatic tubing and industrial hoses.Read guide
 BIO-BASED & SPECPA12 Injection Molding GuidePolyamide 12 - bio-specialtyPA12 is a polyamide with very low moisture absorption compared with PA6 or PA66, good dimensional stability and excellent impact resistance at low temperature. Common in fuel lines, gear wheels and components where moisture-induced dimensional change is a problem.Read guide
 BIO-BASED & SPECGlass-Filled Composites Injection Molding GuideGlass-fibre and mineral filled composites - bio-specialtyGlass-fibre and mineral filled composites are thermoplastics (PA, PP, PBT, PPS) reinforced with glass fibre, mineral flakes or a mixture. The filler changes the shrinkage, the heat resistance and the wear behaviour -the steel moves up a family because glass is abrasive.Read guide
Compare Plastic Grades at a Glance: Shrinkage, Process Window and Mold Steel
Shrinkage, melt and mould temperature, abrasiveness and the steel each grade normally runs in — values for grade selection, not a replacement for the resin supplier's TDS.
| Material | Shrinkage % | Melt °C | Mould °C | Abrasiveness | Usual steel |
|---|---|---|---|---|---|
| ABS | 0.4–0.7 | 220–260 | 40–80 | Low | P20 / 718H |
| PP | 1.5-2.0 | 200-240 | 40-60 | Low | P20 / 718H |
| PS | 0.4-.7 | 180-220 | 40-60 | Low | P20 |
| PE | 1.5-2.0 | 180-220 | 40-60 | Low | P20 |
| PVC | 0.5-.8 | 160-20 | 40-60 | Low | S136 / 2316 |
| PMMA | 0.4-.6 | 210-40 | 60-0 | Low | 718H / NAK80 |
| PET | 0.7-1.0 | 250-270 | 70-0 | Medium | H13 / 718H |
| SAN | 0.4-.7 | 200-30 | 50-0 | Low | P20 / 718H |
| PC | 0.5–0.7 | 280–320 | 80–110 | Low | H13 / S136 |
| PA+GF | 0.2–0.5 / 0.6–1.0 | 260–290 | 80–100 | High (glass) | H13 / 2316 |
| PA | 1.5-.5 | 250-90 | 60-00 | Medium | 718H / H13 |
| POM | 1.8-.1 | 190-10 | 80-00 | Medium | H13 / NAK80 |
| PBT | 1.7-.3 | 230-60 | 70-0 | Medium | H13 |
| PC/ABS | 0.5-.8 | 230-60 | 50-0 | Low | 718H |
| PPO | 0.5-.7 | 260-90 | 80-00 | Low-Med | H13 |
| TPU | 0.8-1.2 | 180-10 | 30-0 | Low | P20 / 718H |
| PPS | 0.3-0.7 | 280-20 | 130-50 | High | H13 / S136 |
| UHMWPE | 2.5-.5 | 180-220 | 70-00 | High | H13 |
| PEEK | 0.8-1.2 | 340-80 | 170-90 | High | H13 / Invar |
| PTFE | N/A | N/A | N/A | N/A | N/A (sintered) |
| PPSU | 0.7-1.0 | 320-60 | 120-40 | Low | 718H / NAK80 |
| PEI | 0.5-.8 | 340-80 | 130-50 | Low | H13 / 718H |
| LCP | 0.05-0.2 | 280-30 | 80-20 | Medium | H13 |
| PPA | 1.0-.8 | 290-30 | 80-00 | Medium | H13 / 718H |
| PA46 | 1.5-2.0 | 280-10 | 80-00 | Medium | 718H / H13 |
| LSR | 0.5-.0 | N/A (curing) | 160-00 | Low | S136 / 2316 / H13 |
| TPE | 0.8-.5 | 160-20 | 25-0 | Low | P20 / 718H |
| TPV | 1.0-2.5 | 190-30 | 30-0 | Low | P20 |
| TPS | 1.5-2.0 | 150-00 | 25-0 | Low | P20 |
| PLA | 0.2-.5 | 180-10 | 30-0 | Low | P20 |
| PBAT | 1.0-2.5 | 180-00 | 25-0 | Low | P20 |
| PA11 | 1.0-2.5 | 220-40 | 40-60 | Medium | 718H |
| PA12 | 1.5-2.0 | 210-30 | 40-60 | Medium | 718H |
| GF-Composite | 0.2-.0 | 200-20 | 60-40 | High | H13 / S136 |
Typical values for grade selection. Confirm the exact grade against the resin supplier TDS before releasing a tool or a tolerance.
Frequently asked resin questions
Which resin should I avoid for a first tool?
A glass-filled engineering resin is a difficult first tool because it couples two costs at once: high melt temperature and abrasive wear. If the part only needs to prove the geometry, cut the first tool in an unfilled grade that behaves similarly and move to the filled grade once the design is settled. Starting in PA6-GF30 means the gate, the vents and the screw all wear while the design is still changing.
Does a glass-filled grade really shorten mould life?
Yes, and the wear is concentrated rather than spread. Glass fibre erodes the gate, the sprue bush, the vent lands and any narrow flow path first, because velocity and impingement are highest there. The cavity walls see much less. That is why a glass-filled tool is often specified with a hardened gate insert in an otherwise pre-hardened block.
Can you match a colour without me sending a part?
A physical target is still the reliable route, because a colour read off a screen or a photograph depends on the display, the light source and the camera. If you cannot send a part, send a Pantone reference plus the resin grade, and accept that the first shot is a trial: we will mould coupons and compare them against the reference before the tool is finished.
What do I have to send you to get a material recommendation?
The 3D part or a drawing, the annual volume, the service environment (indoor, outdoor, chemical contact, temperature), the appearance requirement and any regulatory constraint. With those we reply with a resin shortlist, the shrinkage allowance we would cut the tool to, and the steel grade the resin implies.
Why do two suppliers quote different shrinkage for the same resin?
Because shrinkage is a range produced by a specific test plaque, not a constant. Wall thickness, gate location, melt temperature, mould temperature, packing pressure and hold time all move the number, and a supplier may quote flow direction, cross-flow, or an average. The value to design to is the one measured on a part with your geometry, which is why we cut a sample cavity before committing a production tool.
Next step
Tell us the service temperature and the load.
We reply with a shortlist of candidate grades, the shrinkage allowance we would cut the tool to, and the mould steel each grade implies.
 English
 French
 Dutch
 German
 Japanese
 Korean