 한국어



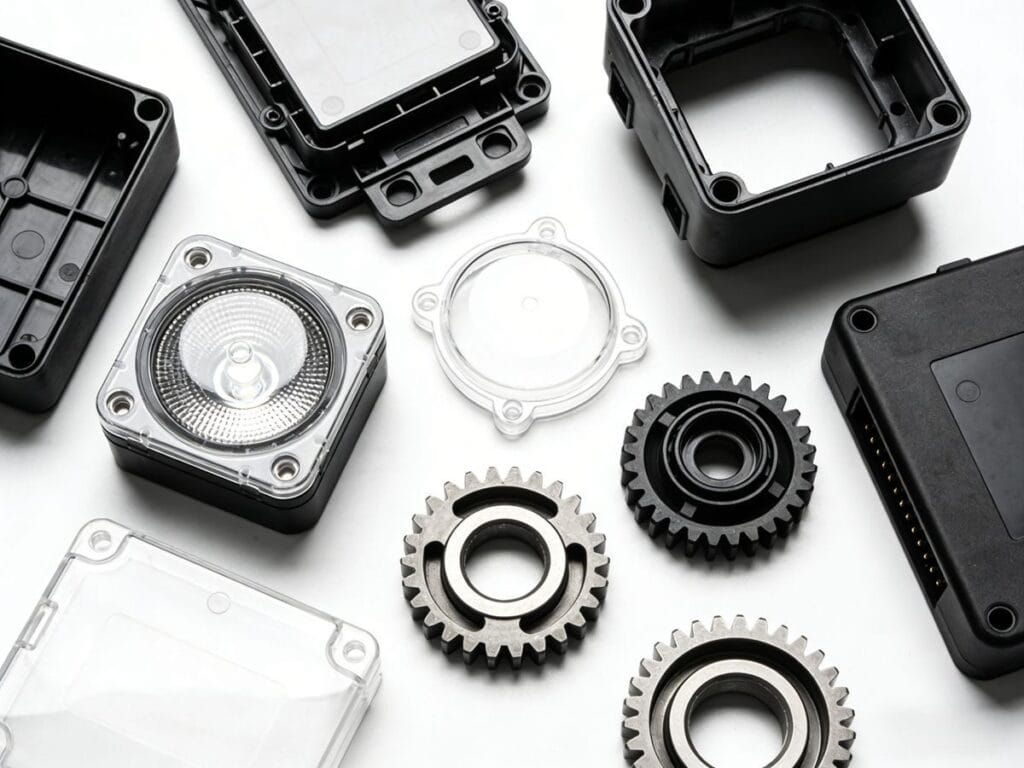
Transfer position is often misunderstood. What does it really mean for injection molding processes?
The transfer position in injection molding is crucial for achieving optimal part quality. It defines when the transition occurs from filling the cavity to maintaining pressure. Misunderstanding or miscalculating this can lead to defects.
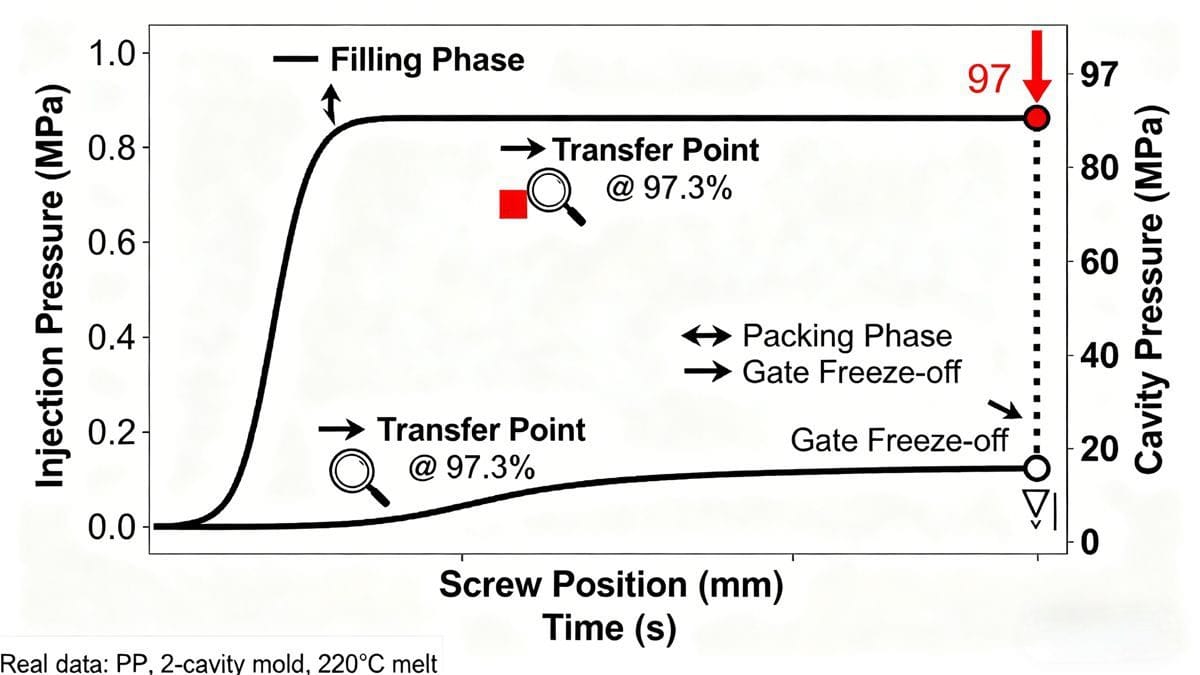
Too often, injection molders take transfer position for granted. It’s not just a number. It's a complex interplay of multiple factors. Failing to grasp this can seriously impact your production and quality.
The Physics of Transition: How Molecular Orientation and Thermal Gradients Dictate Optimal Transfer Timing?
The mechanics of injection molding can be puzzling. How do factors like molecular orientation and thermal gradients affect transfer timing?
Transfer timing relies heavily on how materials behave under heat and pressure. The orientation of molecules can dictate how well the material fills the cavity. Moreover, thermal gradients can lead to inconsistencies in the fill, affecting the final product.
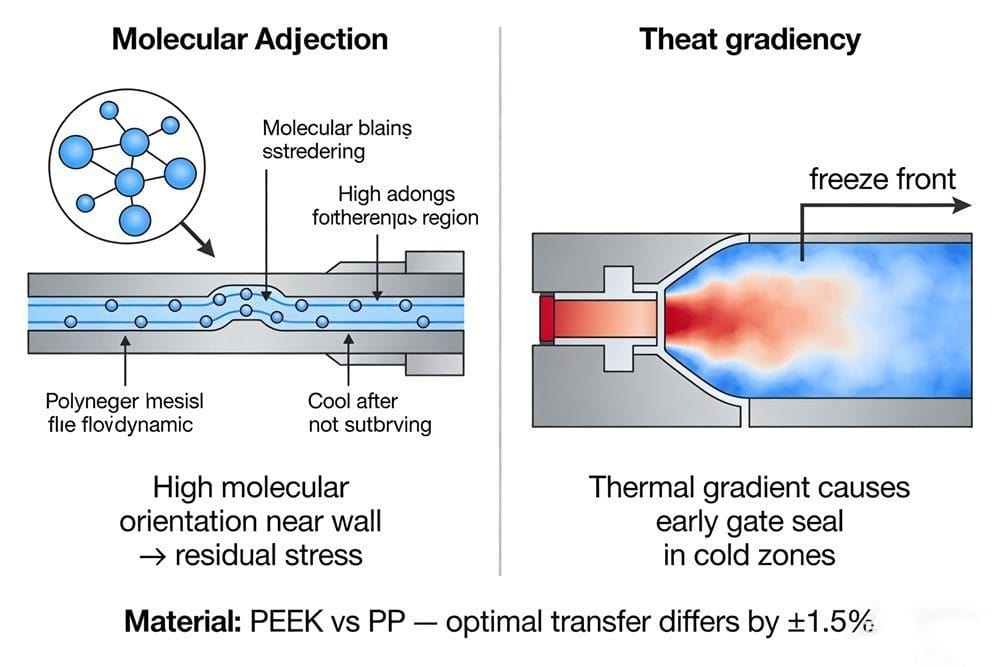
Understanding these elements can help you optimize the transfer position. It’s about aligning the material's behavior with the mold's characteristics. This careful balancing act is what makes quality parts.
When we consider molecular orientation, it becomes clear that temperature plays a role. Different materials have different thermal characteristics. For instance, high-temperature materials, like PEEK, may require different transfer positions than standard polypropylene. This is not just academic; it affects the reality of production.
Take time to analyze both thermal gradient and molecular orientation for your specific materials. A small adjustment in temperature can lead to better outcomes. This is an area where many molders overlook critical insights.
Beyond Screw Position: Cavity Pressure Sensing, Real-Time Feedback Loops, and Closed-Loop Transfer Control Architectures?
Is there more to transfer position than just screw position? Absolutely! Let's delve deeper into the technology that enhances this aspect.
Gone are the days when screw position was the sole indicator of when to transfer. Modern injection molding utilizes cavity pressure sensing and real-time feedback loops to provide a more precise control mechanism. This real-time data allows for adjustments that were not possible before.

Cavity pressure sensors provide feedback on the fill stage. They can indicate when the material has reached a point where it begins to freeze off at the gate. This is your signal for an optimal transfer point. The use of dual-sensor ΔP rate methods, which measure pressure differences across cavities, has become increasingly popular.
This technology offers a level of detail that allows for better decision-making. It’s not just about being close to the target. It’s about hitting it precisely.
In the ever-evolving world of molding, integrating sensor data with automated systems enhances efficiency. The beauty of closed-loop systems is their ability to tune in real time, making adjustments as necessary. This dramatically reduces the scrap rate and ensures higher quality parts.
Defining the “Transfer Window”: A Process Window Analysis (PWA) Framework for Robust Mold Filling?
What is a transfer window, and why is it important? Let’s explore how to define and utilize this concept for better manufacturing.
The "transfer window" refers to a specific range where the transfer position must be set for optimal outcomes. This is not a narrow line but a comprehensive zone of acceptable parameters.
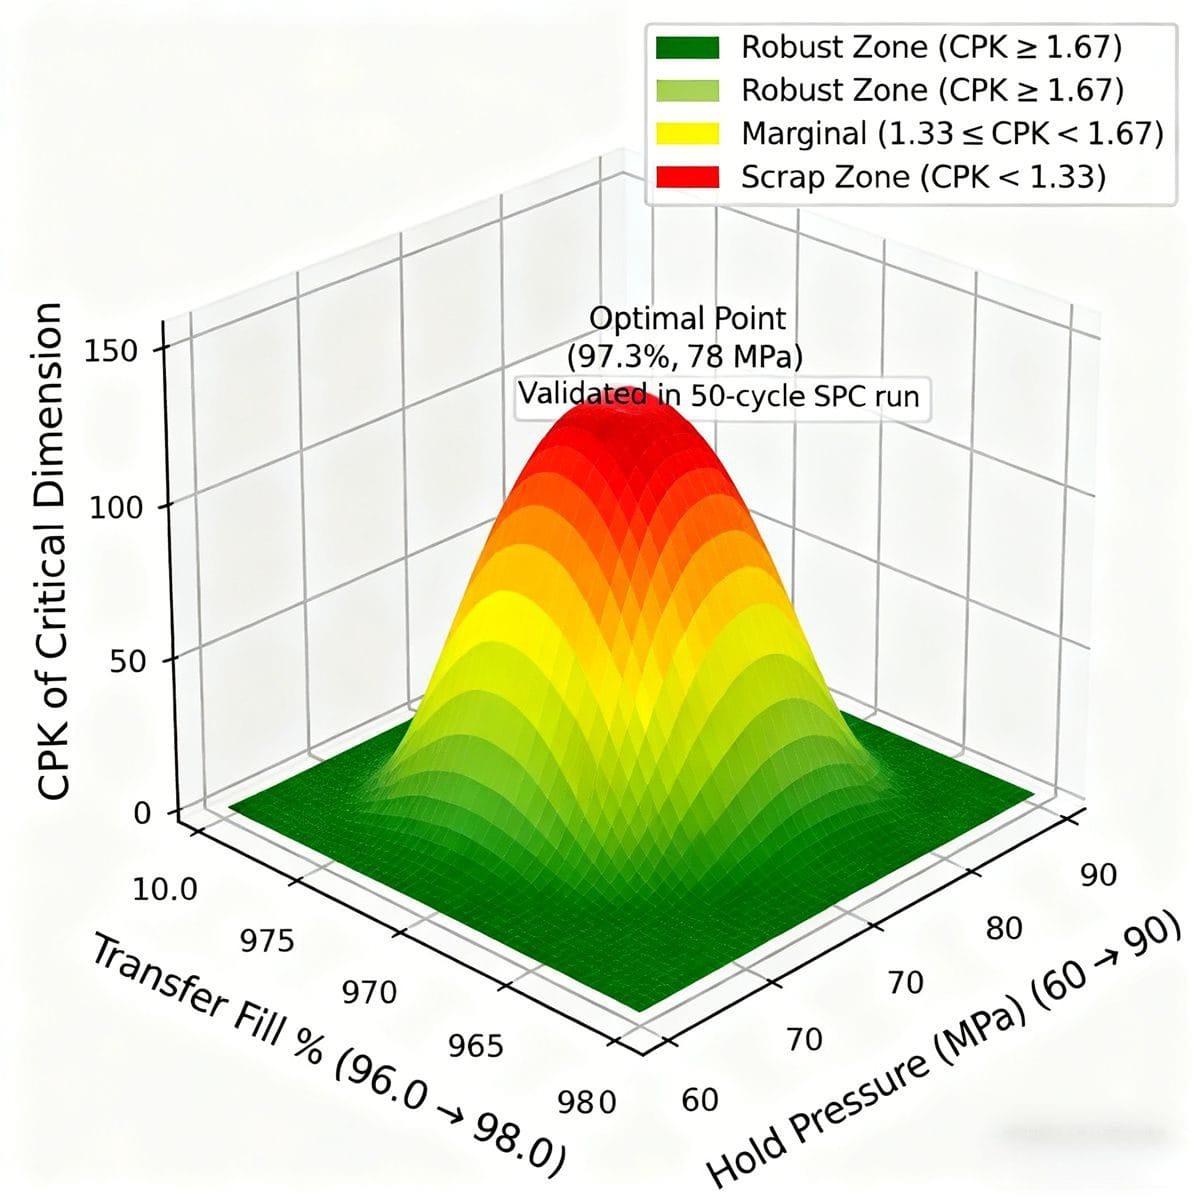
To effectively utilize this window, a Process Window Analysis (PWA) framework can help. By examining various factors like hold pressure and time, you can create a robust mold filling strategy.
Modeling experiments can give you a clear view of where your mold functions best. After running tests, you’ll see that certain combinations yield quality results. For example, a specific hold pressure in tandem with a transfer percentage can lead to fewer defects.
Utilizing the transfer window effectively helps identify the sweet spot where the process operates optimally. This means you’re not just shooting in the dark; you're using data to inform decisions.
Multi-Cavity Imbalance and Transfer Synchronization: When One Cavity Leads, the Rest Follow — or Fail?
How does multi-cavity molding complicate the transfer position? The answer lies in synchronization and balance.
In a multi-cavity mold, if one cavity fills faster than the others, it can create significant issues. Transfer positions must be synchronized to avoid defects such as sink marks and voids.

Each cavity may have unique conditions based on its position in the mold. Factors like runner geometry and cooling can create imbalances. If you set a global transfer position, you risk underpacking some cavities while overpacking others.
To combat this, per-cavity transfer offsets can be established. This means adjusting the settings for each cavity based on its specific needs. By monitoring cavity pressure and timing, you can make informed adjustments.
In short, understanding your multi-cavity setup is essential for success. Synchronization of transfer positions contributes directly to quality and consistency.
From Trial-and-Error to Model-Based Optimization: Integrating Moldflow Simulation with In-Mold Sensor Data for Predictive Transfer Tuning?
Is trial and error the best way to find the transfer position? Not anymore! Let's discuss how modern techniques can lead to better outcomes.
By integrating Moldflow simulations with in-mold sensor data, injection molders can shift from a trial-and-error approach to a more predictive method. This means understanding how each variable affects the final product before even setting up the mold.

Using simulations allows you to visualize the filling process under various conditions. By running these simulations alongside real data from sensors, you can identify the true transfer point more accurately.
This predictive tuning not only improves efficiency but also reduces costs. It minimizes the number of trial runs needed and quickly leads to optimal settings.
The combination of simulation and real-time data is a game-changer. It's about making informed decisions based on real-world variables rather than guesswork.
The Cost of Mis-Transfer: Quantifying Defect Formation, Scrap Rate, and Long-Term Part Performance Degradation?
What happens when the transfer position is not set correctly? The consequences can be severe.
Mis-transfers can lead to defects, which in turn increase scrap rates. The cost of these miscalculations goes beyond immediate waste. They can affect long-term part performance, leading to customer dissatisfaction.
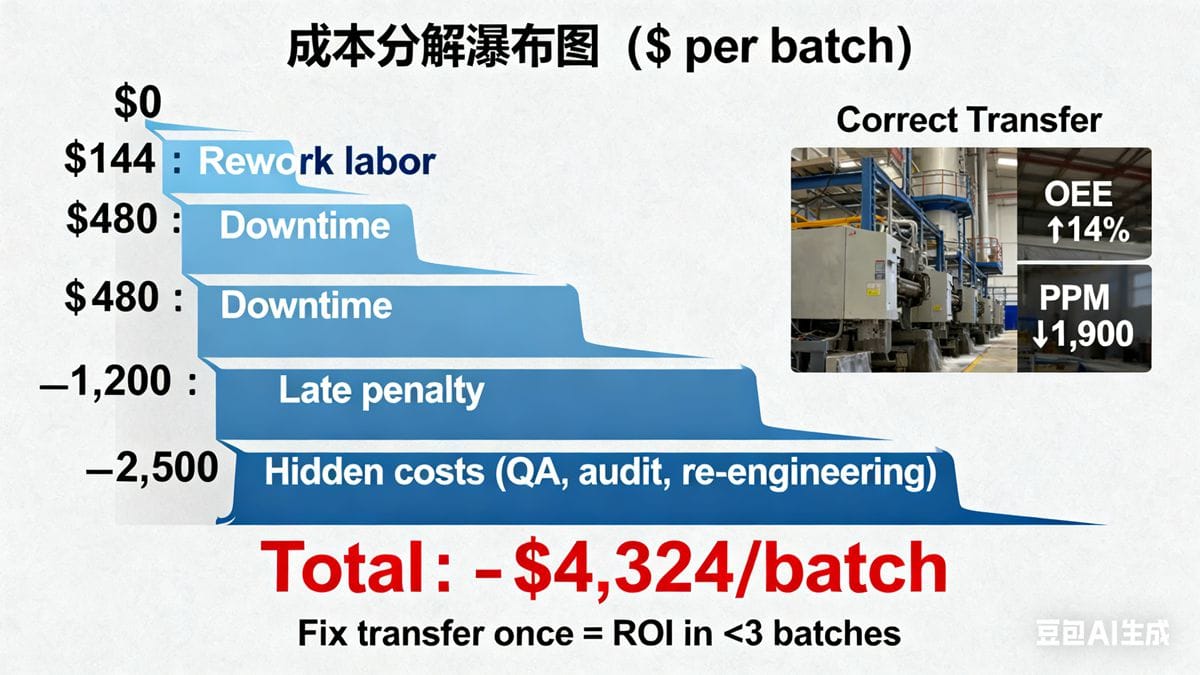
Understanding the financial implications of a poor transfer position is crucial. It’s not just about the immediate losses; it affects your reputation and future work.
Taking the time to analyze your transfer settings can save money in the long run. Identify defects early and address the transfer position accordingly.
결론
In summary, understanding and optimizing transfer position is key to high-quality injection molding. Don’t let outdated practices dictate your process.
저자 소개

Alex Yu
아이디얼 프로 매뉴팩처링
알렉스는 Ideal Pro의 공동 창립자이지만, 주요 프로젝트를 총괄하거나 기술 팀을 이끌지 않을 때는 장거리 자전거 타기를 즐기거나, 동네에서 가장 맛있는 커피를 찾아다니거나, 다음 여행 계획을 세우는 모습을 볼 수 있습니다. 국제 무역 영업과 프로젝트 관리 분야에서 20년 이상의 경력을 쌓아온 그는 촉박한 마감 기한부터 까다로운 엔지니어링 문제까지, 그 사이의 모든 상황을 다 겪어보았습니다. 그는 훌륭한 성과는 충분한 휴식을 취한 마음과 맛있는 커피에서 나온다고 믿으며, 맡은 모든 프로젝트에 그와 같은 호기심과 세심한 주의를 기울입니다. 사무실에 있지 않을 때는 대개 야외 어딘가에서 새로운 장소를 탐험하며, 나중에 나눌 이야기를 수집하곤 합니다.




 English
 French
 Dutch
 German
 Japanese
 Korean