 日本語



Mastering PSU Injection Molding: A Comprehensive Processing Guide
Polysulfone (PSU, also known as PSF) is a high-temperature, high-strength thermoplastic engineering plastic. It is renowned for its high mechanical strength, excellent electrical insulation, high heat deflection temperature, and good chemical resistance. Notably, it exhibits superior thermal aging resistance, creep resistance, and dimensional stability.
Typical Applications
PSU is widely used across various sectors including electronics, food & daily commodities, automotive, aerospace, medical, and general industry.
- Electronics: Contactors, connectors, transformer insulation parts, SCR caps, insulating bushings, coil bobbins, terminals, PCBs, bushings, covers, TV system parts, capacitor films, brush holders, and alkaline battery boxes.
- Aerospace & Automotive: Protective cover assemblies, electric gears, battery covers, aircraft interior/exterior parts, and spacecraft protective shields.
- Consumer Goods: Camera baffles, lighting components, and sensors.
- Food & Medical: Replacing glass and stainless steel for steam trays, coffee servers, microwave cookers, milk containers, milking machine parts, and beverage dispensers. In the medical field, it is used for surgical trays, atomizers, humidifiers, dental instruments, flow controllers, and laboratory equipment.
- Chemical Industry: Pump covers, tower protective layers, acid-resistant nozzles, pipes, and valve containers.
Injection Molding Process Characteristics
Understanding the rheological properties of PSU[^1] is crucial for successful molding.
- Amorphous Polymer: PSU has no distinct melting point. The Glass Transition Temperature ($T_g$) is approximately 190°C. Molding temperatures generally exceed 280°C. The finished products are transparent.
- Viscosity Sensitivity: Similar to Polycarbonate (PC), PSU melt behaves like a Newtonian fluid. The viscosity is highly sensitive to temperature. When the melt temperature exceeds 330°C, viscosity drops by 50% for every 30°C increase.
- Flow & Stress: Despite temperature sensitivity, the viscosity remains high, resulting in poor flow. The melt cools rapidly, and due to the rigid molecular chains, internal stress is difficult to eliminate.
- Moisture Sensitivity: Although PSU has no hydrophilic groups and low equilibrium moisture absorption (0.6%), trace moisture during molding can cause melt degradation due to high heat and shear. Drying is mandatory.
- Shear Sensitivity: Excessive injection rates can cause melt fracture, limiting the filling rate and making mold filling difficult.
Machine & Equipment Requirements
To process PSU effectively, specific machine configurations are recommended to handle its high viscosity and temperature requirements.
Screw and Barrel Specifications:
| Component | Requirement | 詳細 |
|---|---|---|
| Screw Type | Single flight, Full thread | Constant pitch, Low compression ratio. |
| L/D比 | 14:1 to 20:1 | Ensures proper melting and homogeneity. |
| Speed Control | Variable Speed Drive | Required to reduce screw load. Speed: 15–45 rpm (stepless speed regulation). |
| 温度管理 | High Precision | Must be stable up to 400°C. |
| ノズル | Extension Type | Must have independent heating control. Aperture > 5mm (no drooling due to high viscosity). |
Product & Mold Design
Designing for PSU requires accounting for its flow limitations and thermal properties.
Wall Thickness & Geometry
- Minimum Thickness: Due to poor flow (Flow Length/Thickness ratio $approx$ 80), wall thickness should not be less than 1.5mm (ideally > 2mm).
- Corners: PSU is sensitive to notches. Use fillets (arc transitions) for all right or sharp angles to prevent stress concentration.
- Shrinkage: Stable at 0.4% – 0.8%. Shrinkage is consistent in both flow and transverse directions.
- Draft Angle: Recommended at 1:50.
Mold Layout
- 表面仕上げ: Cavity surface roughness should be Ra 0.4 or better for a glossy finish.
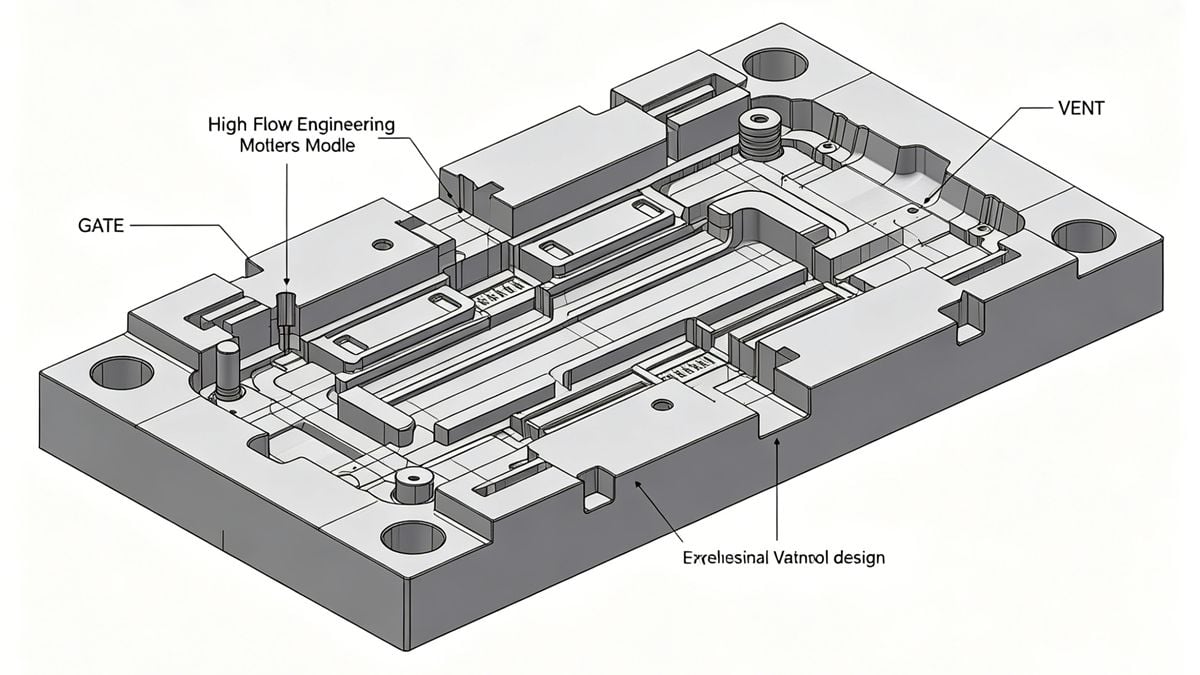
- Runners: Main sprue should be short and thick (diameter $ge$ 1/2 of part thickness) with a 3°–5° taper. Sub-runners should be circular or trapezoidal; avoid bends.
- Gates: Size should be as large as possible. The land length (straight part) should be short (0.5–1.0mm). Locate gates at thick wall sections.
- Cold Slug Well: Essential at the end of the sprue.
- Venting: Critical for thin-walled parts requiring high injection speed. Vent depth should be controlled below 0.08mm.
- 金型温度[^2]: High mold temperature is necessary to improve flow. Ideally > 140°C (minimum 120°C).
Processing Parameters
Optimizing these parameters is key to preventing defects like degradation or melt fracture.
Drying Process
- Hot Air Circulation: 120–140°C for 4–6 hours. Bed thickness: 20mm.
- Vacuum/Desiccant Drying: 130°C for 0.5–1.0 hours.
Temperature Settings
- Barrel Temperature:
- **Thin Wall ( 300°C (up to 320°C or 350°C for specific grades).
- Thick Wall (> 5mm): 280–300°C.
- ️ Warning: Decomposition begins visibly above 360°C. Do not exceed 400°C.
Pressure & Speed
- 射出圧力[^3]: High pressure is required due to poor flow. Generally > 100 MPa, sometimes up to 140 MPa. This increases density and reduces shrinkage.
- Injection Speed: Generally Low to Medium. High speeds cause melt fracture. Exception: Thin walls (~2mm) may require higher speeds to fill before freezing.
- Screw Speed: Low speed recommended (15–45 rpm) due to high melt viscosity.
Cycle & Post-Processing
- Mold Temp:
- Wall 2–5mm: 100–120°C.
- Wall > 5mm or 320°C should be avoided to prevent degradation.
[^1]: Understanding rheological properties is crucial for optimizing PSU processing and product quality. [^2]: Explore the significance of mold temperature in achieving optimal flow and product quality. [^3]: Discover how injection pressure influences the quality and characteristics of molded thermoplastic products.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean