 日本語



Injection speed (screw forward speed) is arguably the most critical parameter in the 射出成形[^1] process. It has a direct and relationship with the quality of the finished part.
By properly determining the start, middle, and end points of filling speed segments—and achieving a smooth transition between set points—you can maintain a constant melt surface speed. This ensures optimal molecular orientation and minimizes internal stress.
> 主なポイント: The goal of velocity profiling is to keep the melt front velocity (MFV) constant throughout the filling phase.
1. Core Principles of Speed Segmentation
To achieve high-quality molding, we recommend adhering to the following fundamental principles:
- 一定表面速度: The velocity of the fluid front should remain constant.
- 凍結防止: Use rapid injection to prevent the melt from freezing prematurely during the process.
- Critical Area Management: Balance high speed in runners with reduced speed at the gate (entry point).
- Precision Stopping: The speed must ensure the cavity stops filling immediately after being full to prevent over-packing, flash, and residual stress.
- Geometry Awareness: 設定では、金型の形状、流れの制限、および不安定要因を考慮に入れる必要があります。.
2. The Relationship Between Material and Speed
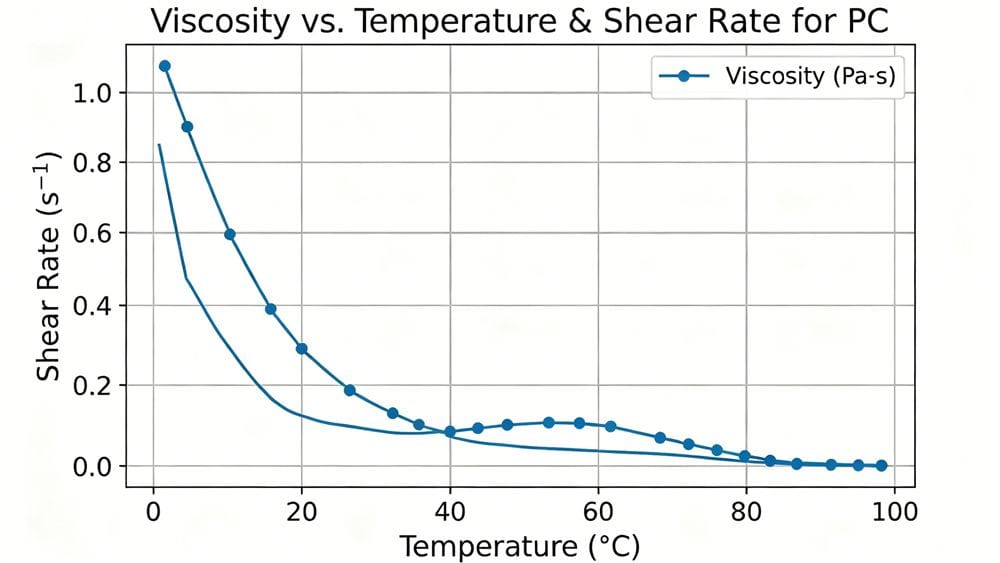
Material characteristics are paramount. Polymers can degrade due to excessive stress. While increasing melt temperature can lead to oxidation, shear-induced degradation is often the bigger risk.
However, higher temperatures reduce viscosity, which lowers shear stress. Multi-stage injection speeds[^2] are particularly helpful for heat-sensitive materials like PC(ポリカーボネート), POM(アセタール), そして UPVC.
Shear Sensitivity vs. Viscosity
| 材料の種類 | Viscosity Characteristic | Speed Strategy | Risk Factor |
|---|---|---|---|
| PC, POM, UPVC | Heat Sensitive | Multi-stage / Controlled | Thermal degradation & Shear stress |
| Glass-Filled Nylon | High Sensitivity | Smooth Transitions | Fiber breakage & Surface finish |
| High Viscosity (e.g., PC) | High Resistance | Slower at Gate | Cold slugs entering cavity |
3. Mold Geometry: The Deciding Factor
The physical shape of your mold dictates your speed profile:
- Thin Walls: Require maximum injection speed to fill before freezing.
- Thick Walls: Require a Slow-Fast-Slow velocity curve to avoid defects.
- Cross-Sections: Decelerate when the melt front reaches cross-sectional changes.
- Radial Diffusion: Ensure the melt volume increases evenly for complex molds.
- Long Runners: Must be filled rapidly to reduce melt front cooling. Exception: High viscosity materials (like PC) where too much speed drags cold slugs into the cavity.
4. Troubleshooting Defects via Speed Control
Most injection molding defects can be solved by adjusting the injection speed. Here is how to tackle specific issues:
A. Gate Defects (Burn Marks & Flow Lines) When melt passes through the gate, the surface may cool or stagnate due to sudden narrowing. This creates a pressure peak. High pressure damages the material, causing flow marks or gate burn marks.
- Solution: Decelerate just before the gate to prevent excessive shear, then accelerate back to the original speed. Since precise control at the gate is difficult, decelerating in the final section of the runner is often a better approach.
B. Flash and Air Traps
- Flash: Caused by over-packing.
- Air Traps: Caused by poor venting or turbulent flow at the end of the fill.
- Solution: Reduce the speed in the final segment of injection. This prevents over-filling and allows air to escape through vents.
C. Short Shots These occur when speed is too slow at the gate or flow is obstructed.
- Solution: ゲートや局所的な流れの妨げを通過した直後に、射出速度を上げてください。.
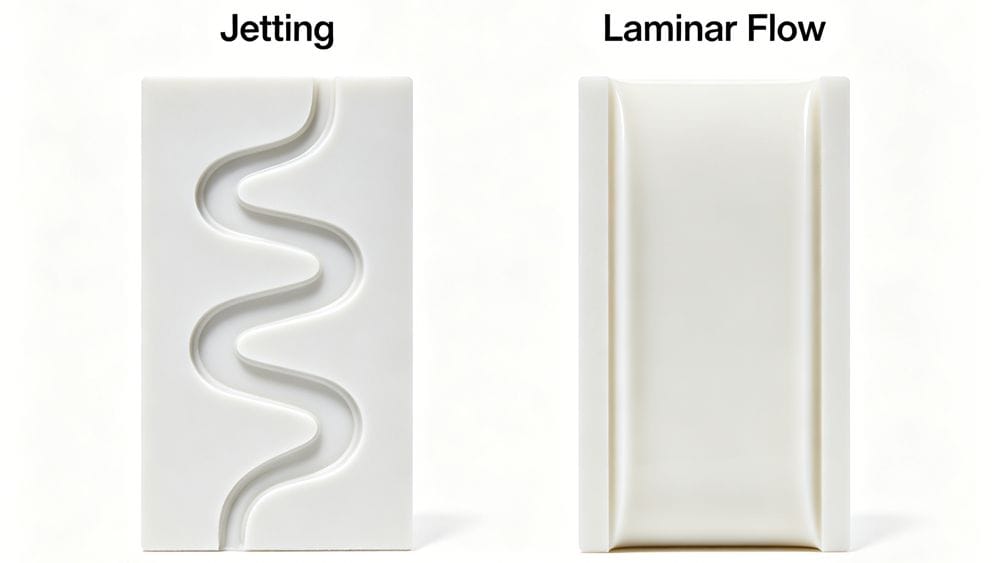
D. Jetting (Snake-like flow) To prevent jetting, the speed setting must ensure rapid filling of the runner area, followed by a slow speed through the gate.
- The Challenge: Finding the conversion point. Too early increases cycle time; too late causes jetting due to inertia. Low viscosity and high barrel temperature exacerbate this trend.
5. Summary: Defects and Speed Adjustments
For quick reference, use the table below to adjust your parameters:
| 欠陥の種類 | 主な原因 | 速度調整戦略 |
|---|---|---|
| ショートショット | Flow obstruction / Slow gate speed | 速度を上げる at gate/obstruction |
| Flash | Over-packing / Excessive pressure | 速度を下げる in final segment |
| 焼け跡 | Excessive shear at gate | 速度を下げる before gate |
| シンクのへこみ | Low pressure transfer / Slow speed | 速度を上げる (High speed reduces heat loss) |
| ジェッティング | High inertia at gate | Slow Down at gate entry |
| Wavy Surface | Viscosity changes / Unstable flow | Optimize for Constant MFV |
結論
Ultimately, the smoothness of the part depends on injection speed. Glass-fiber-filled materials are especially sensitive; for instance, dark spots (waviness) are caused by flow instability due to viscosity changes.
Since melt flow rate is difficult to measure directly, operators often rely on screw forward speed or cavity pressure (assuming no check valve leakage) to (calculate) the settings. Mastering the art of velocity segmentation is the key to controlling part quality.
[^1]: Explore this resource to discover essential techniques and insights for optimizing injection molding processes and improving part quality. [^2]: Explore this resource to discover expert insights and techniques for optimizing injection speeds, ensuring high-quality molded parts.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean