 English



Injection molding[^1] is a complex process where precision is paramount. Among the various parameters that dictate the quality of the final product, pressure plays the most critical role. But are you familiar with the different types of pressures involved?
In this guide, we break down the four essential pressures in injection molding: Injection Pressure, Clamping Pressure, Back Pressure, and Nozzle Pressure. Understanding these concepts is key to optimizing your production line and minimizing defects.
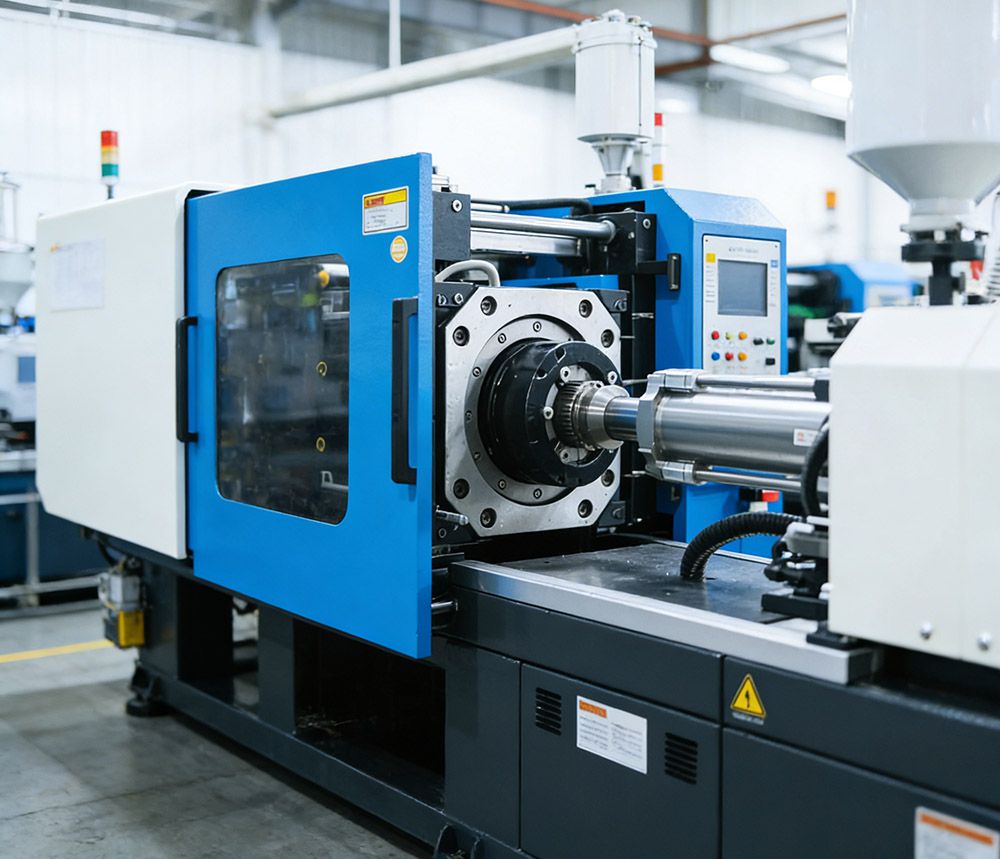
1. Injection Pressure: The Driving Force
Injection pressure is the force responsible for causing the plastic to flow. It is typically measured using sensors located at the nozzle or along the hydraulic line.
Unlike fixed values, injection pressure is dynamic. The more difficult it is to fill the mold, the higher the injection pressure required. There is a direct correlation between line pressure and injection pressure.
Phase 1 vs. Phase 2 Pressure
During the filling stage of the injection cycle, high injection pressure is often necessary to maintain the required injection speed. However, once the mold is filled, this high pressure is no longer needed.
> Pro Tip: When processing semi-crystalline thermoplastics[^2] like PA (Nylon) or POM (Acetal), sudden pressure changes can deteriorate the material structure. In such cases, it is sometimes advisable to skip the second-stage holding pressure to prevent structural damage.
2. Clamping Pressure: Holding the Mold Shut
To counteract the immense force of the injection pressure, clamping pressure is essential. A common mistake is automatically selecting the maximum available clamping force. Instead, you should calculate a suitable value based on the projected area of the part.
The projected area is defined as the maximum area seen from the direction of the clamping force application.
Calculating Clamping Force
For most injection molding scenarios, a rough rule of thumb is:
- 2 tons per square inch
- 31 Mega-Newtons per square meter
Warning: This is a conservative baseline. If your part has significant depth, the side wall area[^3] must also be taken into account, requiring higher clamping forces to prevent flash (material leaking out of the mold).
3. Back Pressure: Balancing Quality and Efficiency
Back pressure is the resistance the screw must overcome while retreating during the plasticizing phase. It is a double-edged sword:
- Pros: High back pressure improves color dispersion and ensures thorough melting of the plastic.
- Cons: It extends the screw recovery time, reduces the length of fibers in reinforced plastics (damaging mechanical properties), and increases stress on the injection molding machine.
Best Practice
"The lower, the better." Under no circumstances should the back pressure exceed 20% of the machine's maximum rated injection pressure. Finding the sweet spot ensures material homogeneity without compromising cycle time or material integrity.
4. Nozzle Pressure: The Final Frontier
Nozzle pressure refers specifically to the pressure inside the nozzle. It is essentially the pressure that directly initiates the flow of plastic into the runner system. Like injection pressure, it has no fixed value and increases with the difficulty of mold filling.
There is a direct relationship between Nozzle Pressure, Line Pressure, and Injection Pressure. However, energy loss occurs between the hydraulic system and the nozzle, varying by machine type:
- Screw-type Machines: Nozzle pressure is typically about 10% lower than the injection pressure.
- Plunger-type Machines: Pressure losses can be significant, reaching up to 50% between the injection pressure and the nozzle pressure.
Understanding these losses is vital for setting accurate process parameters, especially when switching between different types of machinery.
Conclusion
Mastering the nuances of Injection, Clamping, Back, and Nozzle pressures is fundamental to successful injection molding. By moving away from "maximum settings" and adopting a calculated approach based on material properties and mold geometry, manufacturers can achieve higher quality parts, longer tool life, and greater efficiency.
Are you monitoring these pressures in your daily operations? Share your experiences in the comments below!
[^1]: Explore this link to gain in-depth knowledge about injection molding techniques and best practices for optimal production. [^2]: Explore the characteristics of semi-crystalline thermoplastics to better understand their behavior during injection molding. [^3]: Learn about the significance of side wall area in clamping force calculations to prevent material leakage.
About the Author

Alex Yu
Ideal Pro Manufacturing
Alex is the co-founder of Ideal Pro, but when he's not overseeing key projects or steering the technical team, you'll likely find him on a long bike ride, hunting for the best coffee in town, or planning his next travel adventure. With over 20 years of experience spanning international trade sales and project management, he's seen it all — tight deadlines, tricky engineering problems, and everything in between. He believes great work comes from a well-rested mind and a good cup of coffee, and he brings that same curiosity and attention to detail to every project he takes on. When he's not in the office, he's usually somewhere outdoors, exploring new places and collecting stories to share.




 English
 French
 Dutch
 German
 Japanese
 Korean