 日本語



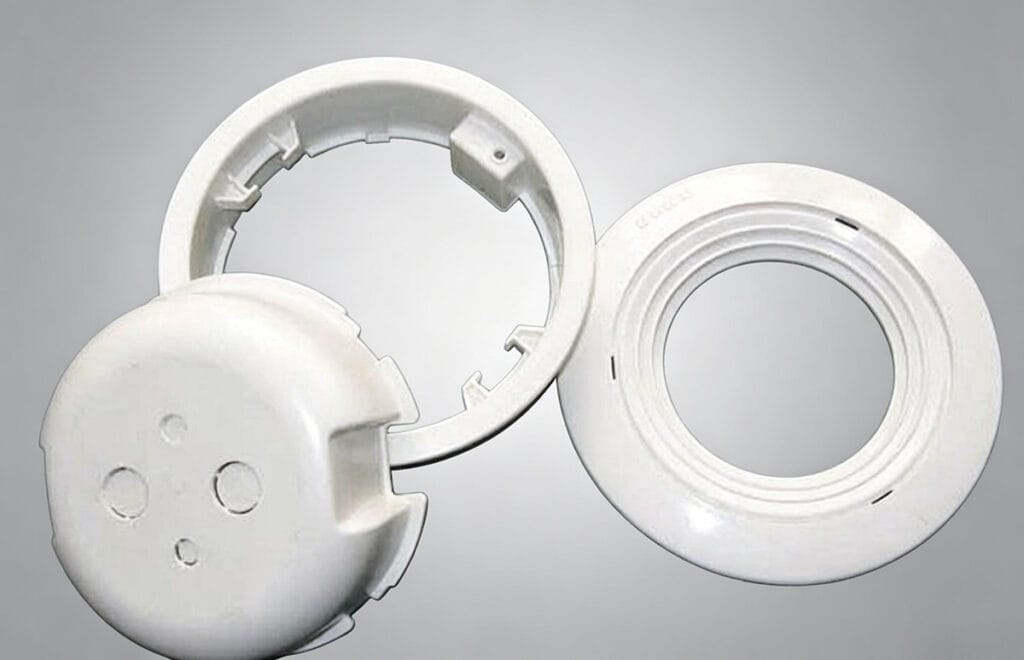
Plastic degradation is a common headache in the 射出成形 industry. Whether it appears as burn marks, discoloration, or brittleness, degraded plastic compromises the quality and strength of your final product.
But what exactly causes this issue? Usually, the culprits fall into three categories: マシン, The Mold, あるいは The Material.
In this guide, we break down the root causes of plastic degradation and provide actionable solutions to help you optimize your production process.
Issues Related to the Injection Molding Machine
Often, degradation happens because the plastic is subjected to excessive heat or stays in the barrel for too long. Here is how to troubleshoot machine-related problems:
A. Excessive Heating in the Barrel
- The Problem: The plastic melt temperature is set too high, causing the polymer chains to break down.
- The Solution: Lower the melt temperature settings. Ensure the temperature profile matches the specific requirements of the resin you are using.
B. Malfunctioning Temperature Controllers
- The Problem: The temperature controller may be reading incorrectly or failing to regulate the heat properly.
- The Solution: Verify that the controller is monitoring the correct zone of the barrel. Recalibrate the temperature controller and inspect the heating bands for stuck relays or loose connections.
C. Incorrect Thermocouple Type
- The Problem: Using a thermocouple type (e.g., J-type vs. K-type) that does not match the controller's configuration leads to false temperature readings.
- The Solution: Check that the installed thermocouples match the type specified by the controller manufacturer (e.g., FECON). Test all thermocouples to ensure they are functioning accurately.
D. Excessive Residence Time
- The Problem: If the shot weight is too small for the machine size, plastic sits in the barrel too long and degrades.
- The Solution: Check your shot weight. If it is less than 25% of the machine's maximum injection capacity, move the mold to a smaller machine.
- 注: If a smaller machine is unavailable, reduce the barrel temperatures to the minimum viable limit to produce acceptable parts.
E. Material Stagnation During Stops
- The Problem: Leaving plastic inside the barrel during production pauses or shutdowns allows it to bake and degrade.
- The Solution: Always purge and clean the barrel before stopping production. Leave the screw in the forward position to prevent material from sitting in the heating zones.
F. Material "Hang-ups" in the Barrel
- The Problem: Plastic can get trapped in scratches or damaged areas inside the barrel (often near the non-return valve), eventually degrading and breaking off into the shot.
- The Solution: Inspect the barrel interior thoroughly. Remove any residue or buildup on the mating surfaces and check for mechanical damage.
Issues Related to the Mold
While less common, mold specifications can indirectly contribute to degradation issues.
A. Mold Capacity Mismatch
- The Problem: Similar to the machine issue, if the mold requires a shot size that is too small for the available machine, it leads to long residence times.
- The Solution: Relocate the mold to an injection molding machine with a smaller shot capacity that better matches the part weight.
Issues Related to the Plastic Material
Sometimes the defect starts before the plastic even enters the machine.
A. Excessive Moisture Content
- The Problem: Many engineering plastics (like Nylon, PET, PC) are hygroscopic. High moisture content causes hydrolysis, leading to degradation and splay marks.
- The Solution: Implement a strict drying regimen. Use the correct hopper dryer settings (temperature and time) recommended by the material supplier.
B. Poor Quality or Contaminated Regrind
- The Problem: Using regrind (recycled scrap) that contains dust, metal contaminants, or has been heat-damaged previously will ruin the new batch.
- The Solution: Strictly separate and inspect regrind materials. Filter out impurities and limit the percentage of regrind mixed with virgin material.
Summary Checklist
To prevent plastic degradation, remember these key takeaways:
- Monitor Temperatures: Ensure controllers and thermocouples are accurate.
- Match Machine to Part: Avoid running small parts on massive machines.
- Cleanliness is Key: Purge the barrel when stopping and keep regrind clean.
- Dry Your Material: Never skip the drying process for hygroscopic resins.
By systematically checking these areas, you can eliminate degradation defects and improve your overall yield.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean