 日本語




Large flat injection molded parts are notoriously prone to warpage and distortion. Because of their expansive surface area, these parts experience significant shrinkage. When combined with severe molecular orientation and uneven mold cooling, the shrinkage rates vary across different directions, causing thin, large-area parts to warp.
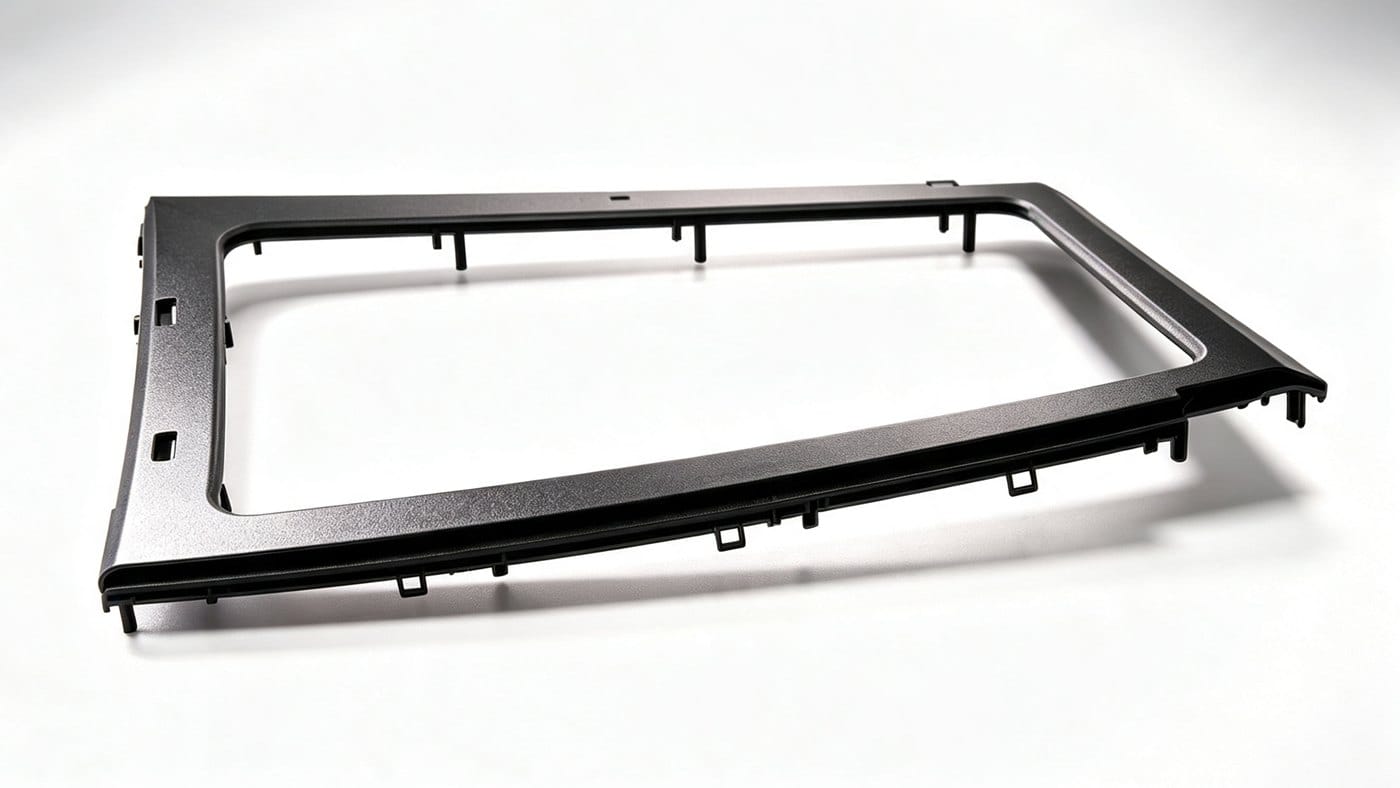
The problem often gets worse if one side of the part features supporting ribs. In such cases, the part will almost inevitably bend toward the ribbed side due to uneven wall thickness and localized shrinkage.
Completely eliminating warpage in large flat parts is a well-known challenge in manufacturing. However, through years of production experience, we have identified four highly effective strategies to resolve this issue. For deeper root cause analysis of warpage defects across all molded components, you can read our full guide: 射出成形における反り:原因、予防策、および是正方法.
Optimize Gate Design with Multi-Point Injection
For large flat parts, a single gate is rarely sufficient. Upgrading to a multi-point gating system (typically using a 3-plate mold) is highly recommended. For parts requiring machines of 240 tons or above, use at least 4 gates.
- Why it works: Multiple gates reduce the severity of molecular orientation and minimize the gap between shrinkage rates in different directions, resulting in a more dimensionally stable part. Unbalanced gate layout is one top trigger of unstable part sizes; check our article about dimensional inconsistency for more background: Why Are My Injection Molded Parts Coming Out with Unstable Dimensions?
Increase Mold Temperature
Raising the mold temperature slows down the cooling rate of the plastic. For ABS materials, maintain the mold temperature at 60°C (140°F) or higher.
- Why it works: A slower cooling process reduces thermal shock and temperature gradients that cause warpage. It also helps relax the polymer chains, decreasing molecular stress and orientation. Proper mold cooling balance is critical for flat part quality.
Boost Injection/ Holding Pressure and Time (Most Critical)
This is arguably the most important step. Significantly increase your injection or holding pressure and drastically extend the holding time.
- Why it works: Extended holding time forces more material into the cavity to compensate for volumetric shrinkage, effectively increasing the final part size and reducing warpage.
- プロのアドバイス Extending the holding time by 10 to 15 seconds has become our go-to troubleshooting method for fixing deformation.
Quick Reference: Troubleshooting Warpage at a Glance
| ソリューション | Key Parameter / Action | Primary Benefit |
|---|---|---|
| Multi-Point Gating | 4+ gates for 240T+ machines | Reduces molecular orientation & uneven shrinkage |
| Higher Mold Temp | ≥ 60°C for ABS | Slows cooling, reduces thermal stress |
| Extended Hold Time | +10 to 15 seconds holding time | Compensates for volumetric shrinkage |
| Out-of-Mold Fixing | Hot jigging (Hot夹具定型) | Corrects residual warpage post-ejection |
Out-of-Mold Fixing (Hot Jigging)
If the first three methods don't yield perfect results, you must resort to out-of-mold fixing. This technique requires precision and a bit of trial-and-error.
- Eject Early: Remove the part from the mold while it is still hot (it should be too hot to touch comfortably).
- Clamp Immediately: Place the hot part into a custom-designed fixing jig on a workbench. Jig design is critical here.
- Account for Springback: Plastic parts will experience "springback" (elastic recovery) as they cool. This recovery typically stabilizes after 12 hours.
- Over-Correct: Because lower ejection temperatures increase springback, you must intentionally over-bend the part in the jig to compensate. You must test and calculate the exact over-correction amount for your specific material and geometry.
まとめ
Fixing warpage in large flat injection molded parts requires a holistic approach. Always start with mold design (gating) and process optimization (temperature and holding time) before relying on post-mold fixing. By systematically applying these four techniques, you can dramatically improve part flatness and reduce scrap rates.
著者について

アレックス・ユー
アイデアル・プロ・マニュファクチャリング
アレックスはIdeal Proの共同創業者ですが、重要なプロジェクトの監督や技術チームの指揮をとっていないときは、長距離サイクリングを楽しんだり、街で一番おいしいコーヒーを探し回ったり、次の旅の計画を立てたりしている姿を見かけるでしょう。 国際貿易の営業やプロジェクト管理に20年以上の経験を持つ彼は、厳しい納期や厄介な技術的課題など、ありとあらゆる状況を経験してきました。彼は、素晴らしい仕事は十分な休息と一杯の美味しいコーヒーから生まれると信じており、その好奇心と細部へのこだわりを、手掛けるすべてのプロジェクトに注ぎ込んでいます。 オフィスにいないときは、たいてい屋外で、新しい場所を探索したり、皆と共有できるエピソードを集めたりしています。.




 English
 French
 Dutch
 German
 Japanese
 Korean